
Sprue
Entry from the machine nozzle.
SprueGlossary
A runner is the channel that carries molten plastic from the sprue to each gate. Runner balance and cross section drive multi cavity fill, scrap, and gate location on the same tool.
Definition
A runner is the channel in an injection mold that carries molten plastic from the sprue to the gate.
It is the main feed path in multi cavity and family molds. Runner layout sets how evenly each impression fills.
Runners can be cold (solidify with the part) or hot (heated, kept molten). This page covers runner geometry and balance. See cold runner and hot runner for system trade offs and tooling scope.
Runner volume still counts in resin planning even when buyers only weigh the molded part.
Tooling
Feed path geometry, balance, and cold versus hot scrap belong on the runner page.
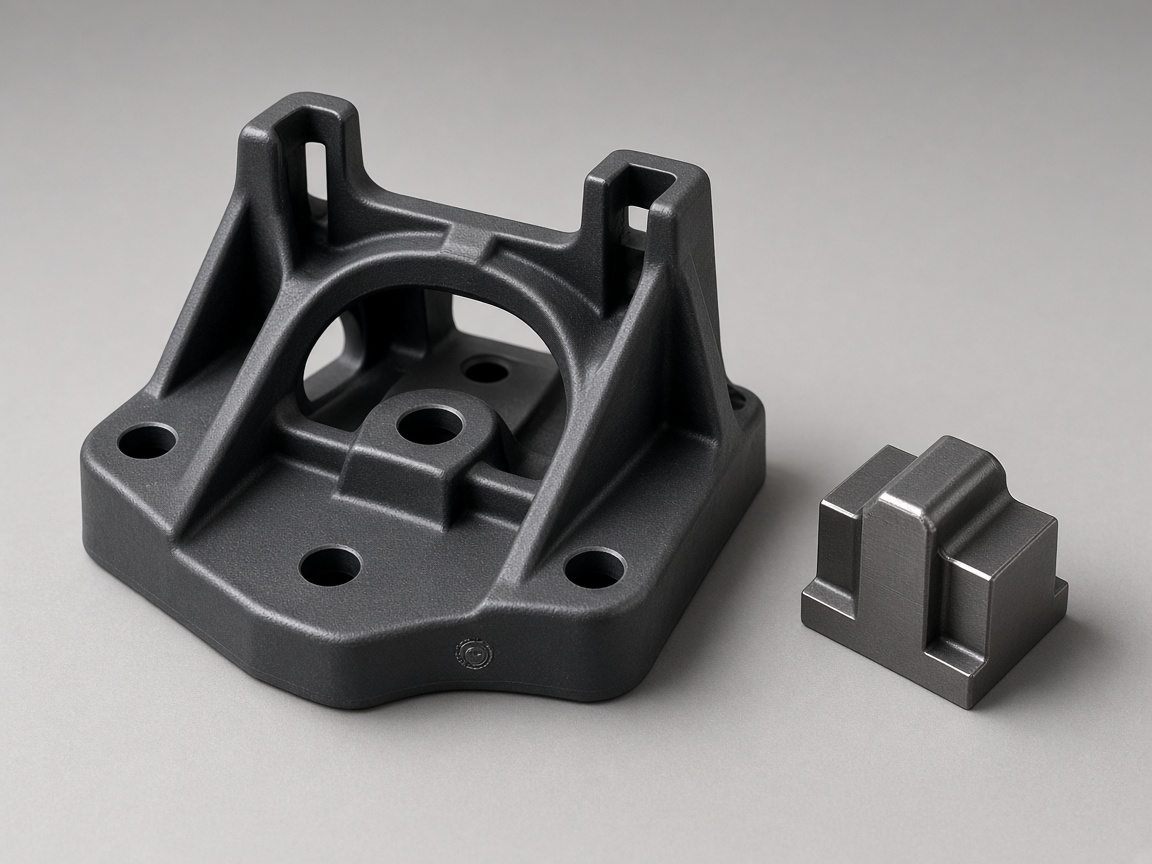
Geometry
Overview for DFM threads. Steel detail and simulation belong on the tooling print.
Common cross sections include round, trapezoidal, and rectangular
Round flow is efficient but needs matching halves; trapezoidal channels are common for machining and ejection
Typical industry diameters are often a few millimeters on commodity layouts; high viscosity or glass filled resins often need larger sections
Balance
Imbalance drives overpack or flash in first fill cavities and short fill or sink in last fill cavities.
Naturally balanced: equal path length, equal cross section, equal bends (H pattern, star, radial)
Artificially balanced: unequal paths tuned by diameter changes to equalize pressure drop
High cavitation tools benefit from mold flow validation before steel is cut
Systems
Hot runner is not always cheaper. Low volume or frequent color changes often favor cold runner.
| Factor | Cold runner | Hot runner |
|---|---|---|
| Scrap | Runner solidifies, adds trim waste | No cold runner slug each cycle |
| Tooling cost | Lower on many programs | Higher (manifold and heaters) |
| Cycle | Longer while runner cools | Often shorter |
| Color change | Easier purge through frozen slug | Harder purge and residence |
| Best use | Low volume, proto, heat sensitive resins | High volume, multi cavity, cosmetic gate needs |
Design
Fix layout in DFM before T1 when possible. Large imbalance after samples often needs steel change.
Shortest practical path from sprue to each gate
Equal branch lengths or validated diameter tuning for balance
Smooth radii, avoid sharp ninety degree turns
Cold slug well at sprue base and direction changes on cold runner tools
Draft for runner ejection on cold runner layouts
Gate seals before the runner freezes on cold runner cycles
Simulate fill balance before cutting steel on multi cavity programs
Go deeper
Each entry covers a different lever on the same tool, not a duplicate definition.
Entry from the machine nozzle.
SprueWhere the runner meets the cavity.
Gate location DFMFrozen slug trim and regrind policy.
Cold runner scrapHeated feed path scope.
Hot runner manifoldHow cold runner scrap returns to material cost.
RegrindBalance shows up in cavity traces.
Cavity pressureLast fill and vent paths follow gate plan.
VentProjected area includes cold runner on many tools.
Clamping forceLayout rules on the DFM hub.
Runner design guideVisual reference
Images are selected from the NetProto Forge media library for this topic.
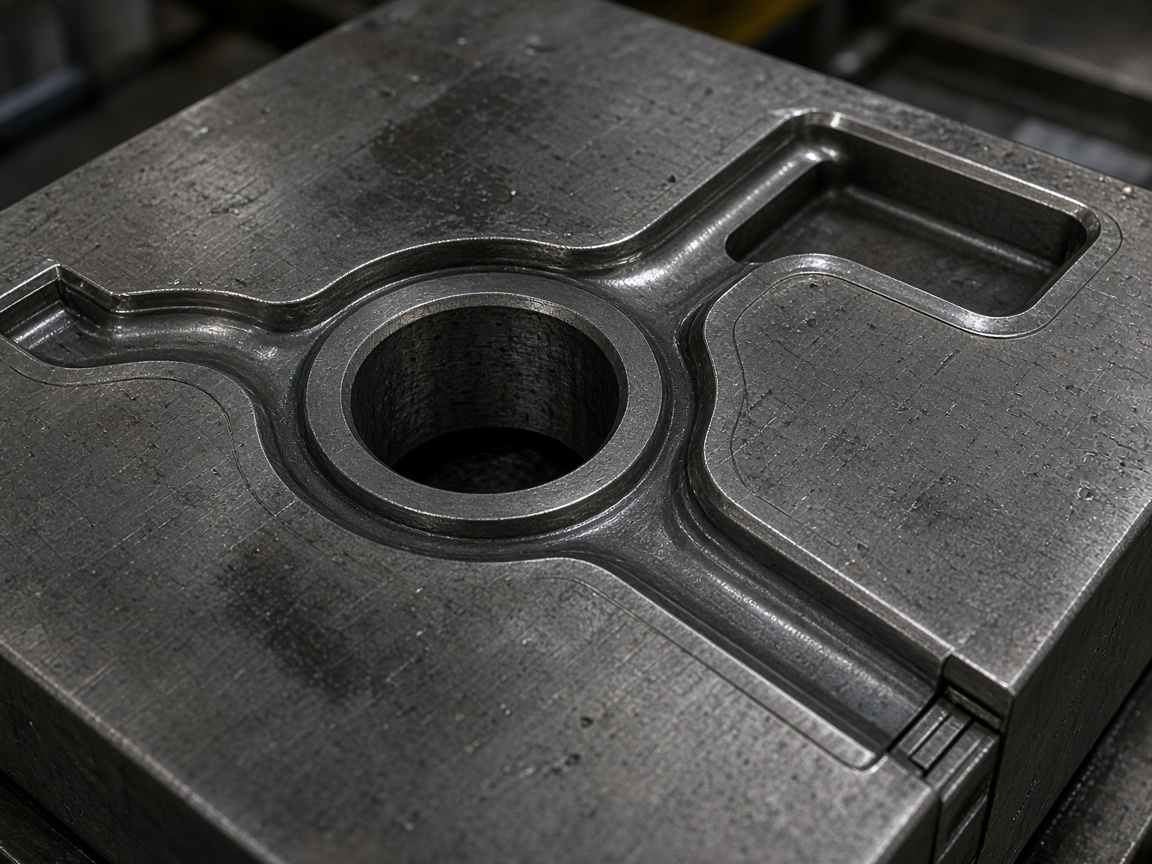
Sprue bushing and machined runner channels on injection mold
Sprue bushing and machined runner channels on injection mold steel
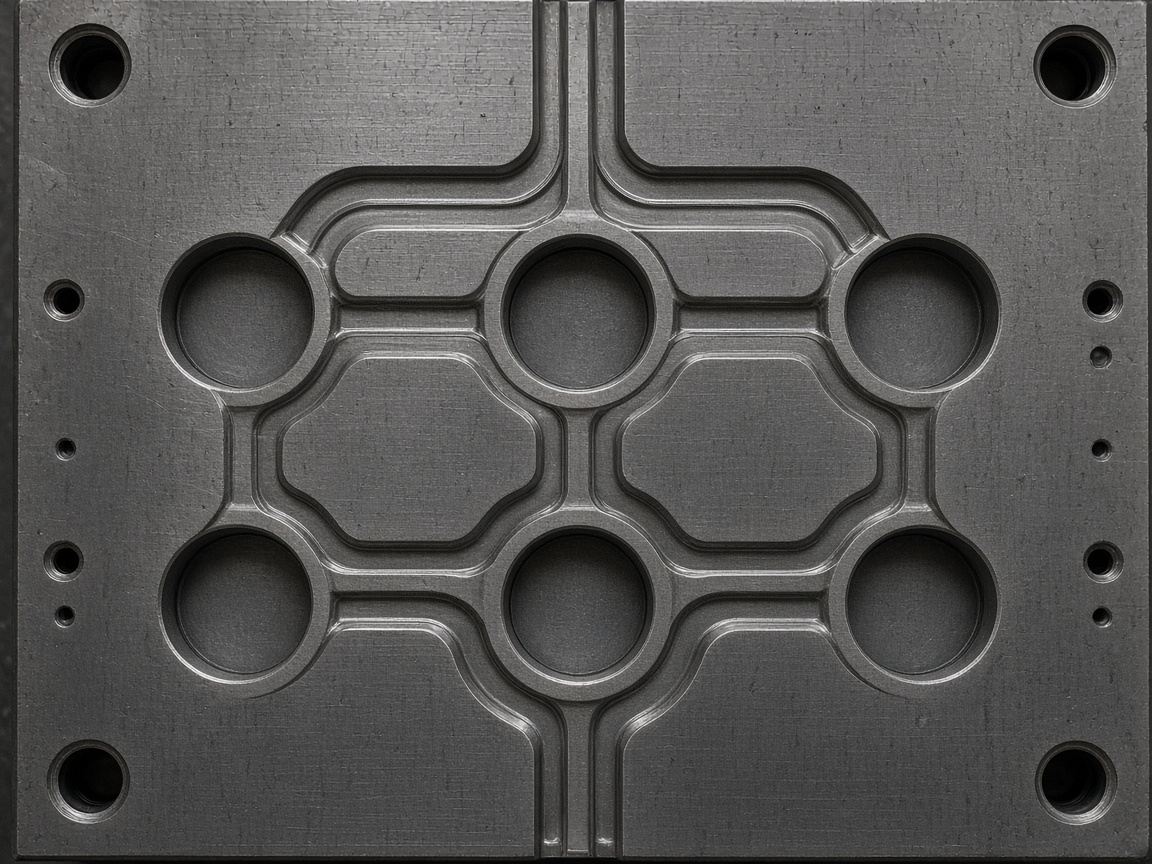
Top view of multi cavity runner layout on mold plate
Top view of multi cavity runner layout on mold plate
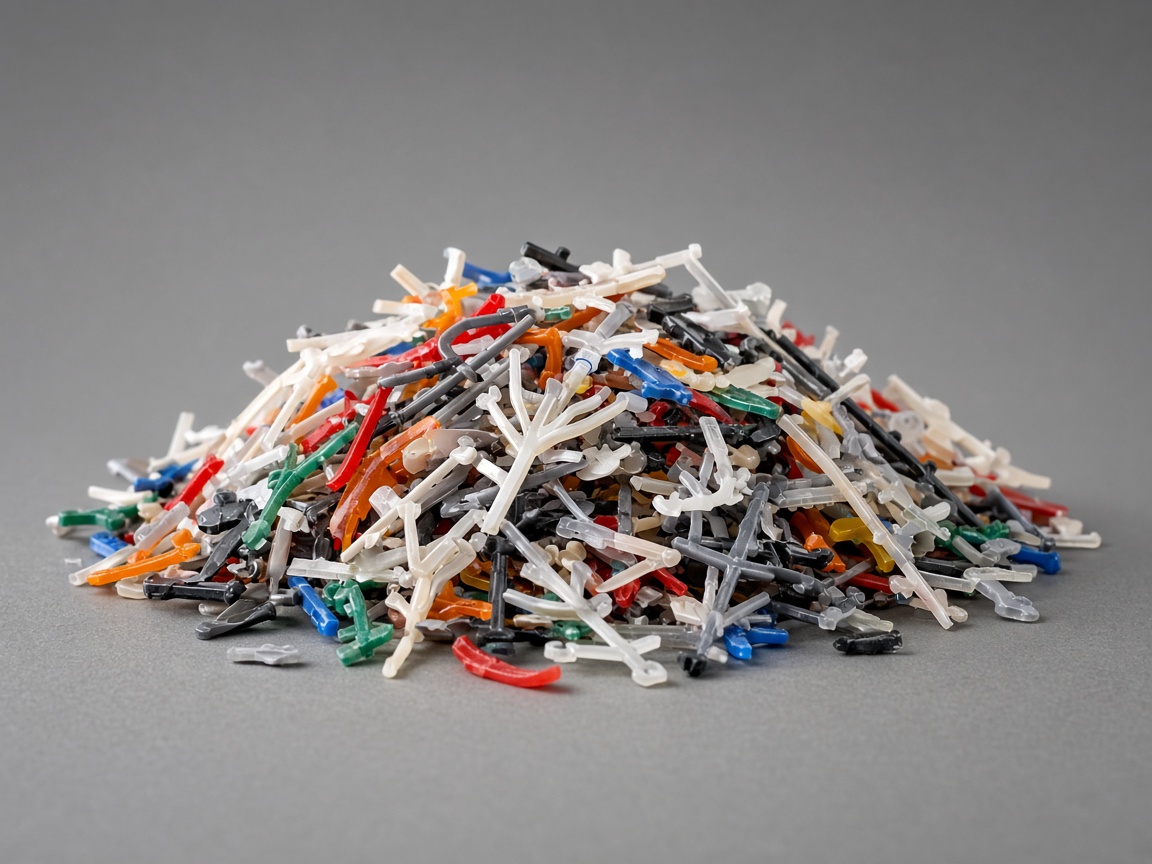
Cold runner trim slug or regrind pile from molding scrap
Cold runner trim slug or regrind pile from molding scrap
FAQ
The sprue connects the machine nozzle to the mold. The runner branches to each cavity. The gate is the restricted entry into the part.
A layout where each cavity sees similar fill time and pack pressure. Natural balance uses equal paths; artificial balance tunes diameters on unequal paths.
Round is efficient for flow. Trapezoidal is easier to cut and eject on many cold runner tools. The mold designer picks based on steel access and balance goals.
Cold runner slug weight adds to each shot. The share depends on part size, cavity count, and runner volume. Regrind policy changes net material cost.
Yes. Fast filling cavities can flash while slow ones short. Weld line position shifts when fill fronts arrive at different times.
Hot runner removes the cold slug trim path. Melt still flows through heated channels and gates. See the hot runner glossary for system scope.
Balance and gate location should be set in DFM before steel is cut. Minor gate tweaks are possible at T1; large imbalance often needs runner steel change.
Next step
If fill imbalance, weld lines, or gate vestige trace to feed path, send CAD with cavity count and annual volume.