
Press picked from memory
- Flash on thin walled lids or large flat covers
- Parting line witness that grows as pack pressure rises
- Tool damage when operators compensate with higher pack
Glossary
During fill and pack, molten plastic exerts pressure on every surface inside the mold. Clamping force is the closing force the press applies so the two halves stay sealed. It is not injection pressure. It is the counterforce that resists separation from cavity pressure on projected area.
Definition
Clamping force is the closing force the press applies so mold halves stay sealed during fill and pack.
During fill and pack, molten plastic pushes on every cavity surface. The press must resist that separation force at the parting line and shutoffs.
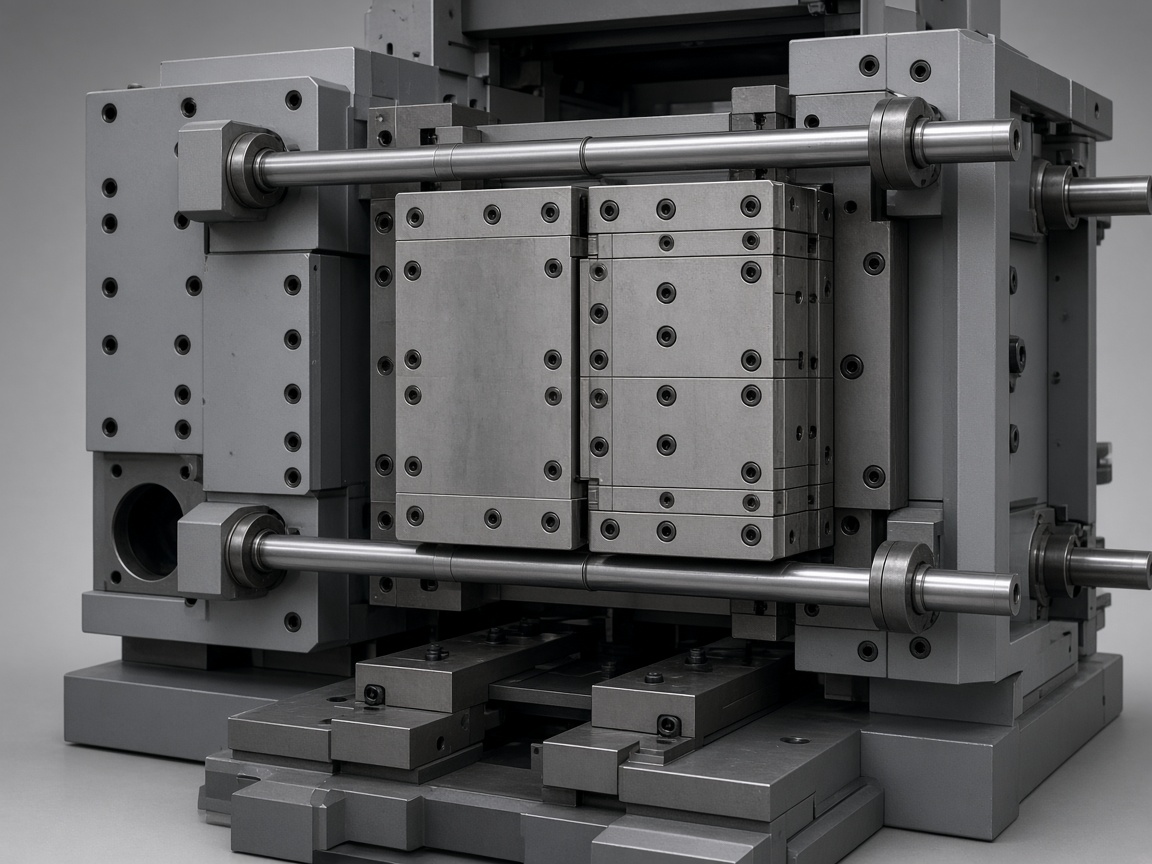
When available clamp is too low for projected area and resin pressure, the parting line opens slightly. Flash, dimension drift, or oil on the seam follow. Raising clamp is not always the first fix. See does higher clamp pressure stop flash .
Clamping force is not injection pressure. It is the counterforce that resists cavity separation from injection pressure acting on projected area.
NetProto sizes production on hardened steel tools for real fill conditions. Upload CAD so projected area and material family enter the conversation before someone picks a press from habit.
Production
Tonnage nameplates, flash at shutoff, and platen context explain sizing better than generic floor shots.
Sizing
Tonnage is a capacity ceiling, not a quality badge. Match projected area, runner style, and resin to the machine window.
Over clamp
More tonnage does not fix poor gate or vent design. It can create new problems.
Crushed vent lands leading to air trap or burn marks
Overload on fine cores and shutoffs leading to tool damage
Higher tie bar preload and mold deflection on some layouts
Small part on a large machine raising hourly cost and setup difficulty
Estimate
Typical industry first pass sizing. Required tonnage is approximately projected area in square inches times clamp factor in tons per square inch, times a safety margin. Confirm on the tooling print and molder study.
| Material class | Typical clamp factor (tons per in squared) |
|---|---|
| PP, PE, soft TPE | About 2 to 3 |
| ABS, PS, HIPS | About 3 to 4 |
| PC, PA, POM | About 4 to 5 |
| Thin wall or glass filled | About 5 to 8 |
Runners and units
These details change clamp math more than most buyers expect.
Cold runner projected area adds to total separation force. Hot runner systems remove runner area from the calculation, which can lower required tonnage on multi cavity tools.
Multi cavity tools multiply cavity projected area. Include runner area unless the tool is hot runner fed.
Add a typical industry safety margin on top of the estimate before you pick a press.
Tonnage units vary by region. One US ton is 2,000 lb. One metric ton is 2,204 lb. About 1,000 kN is roughly 102 metric tons or 112 US tons. Confirm which unit your molder uses.
RFQ notes
Strong RFQ notes reduce press mismatch at T1.
Largest projected area view with parting direction marked
Resin family or known fill pressure class, even if grade is TBD
Cold runner versus hot runner intent and cavity count
Cosmetic class on the parting line versus hidden faces
Go deeper
Each link is a different angle on the same program.
How shops name clamp capacity on the nameplate.
TonnagePack pressure and last fill regions.
GateIn mold data when clamp margin is tight.
Cavity pressureOver clamp can crush vent lands.
VentWhen the parting line opens during pack.
Flash defectClamp rating pairs with shot capacity.
Shot sizeRunner area and tonnage math.
Hot runnerWall, draft, and gate rules that change fill pressure.
Design guide hubRFQ notes for projected area and pack, not a tonnage stamp on the drawing.
How to calculate clamping forceWorn shutoffs and pack changes still leak after you raise the setting.
Does higher clamp pressure stop flash?Visual reference
Images are selected from the NetProto Forge media library for this topic.
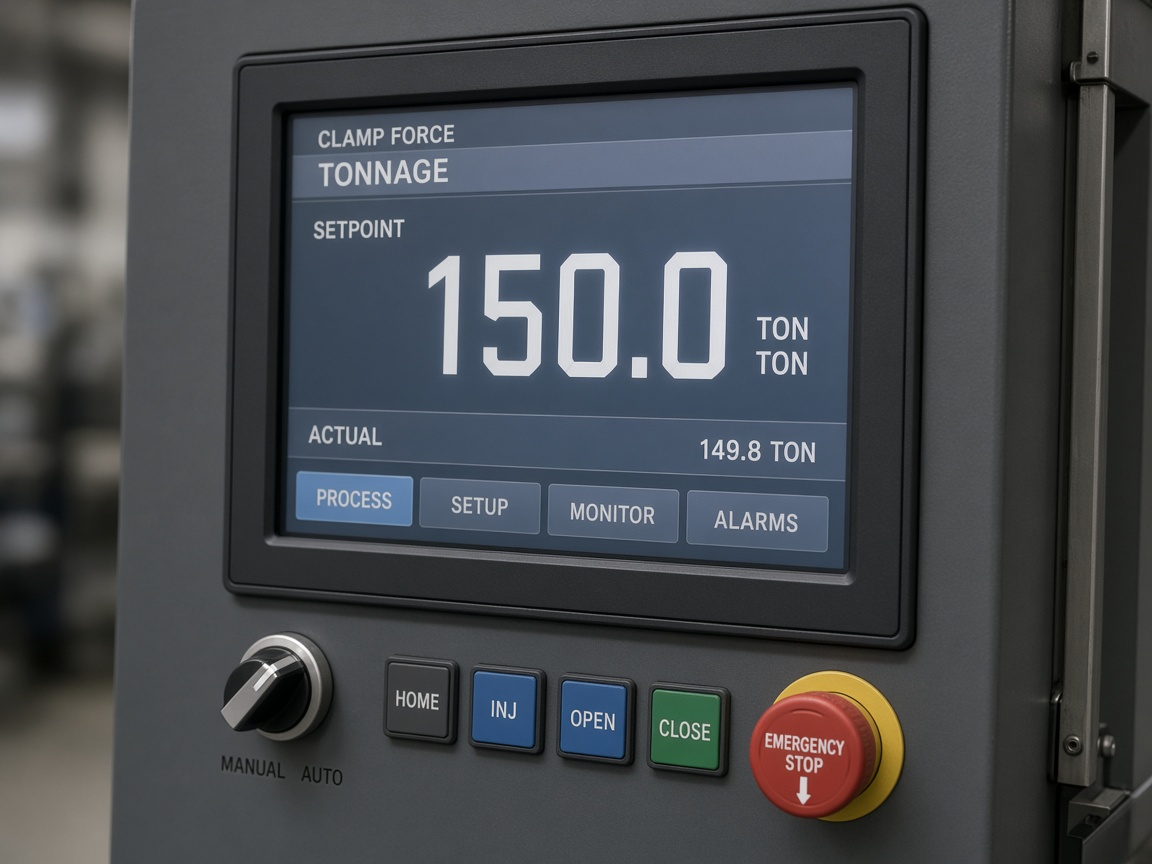
Injection molding press tonnage nameplate or HMI clamp setti
Injection molding press tonnage nameplate or HMI clamp setting
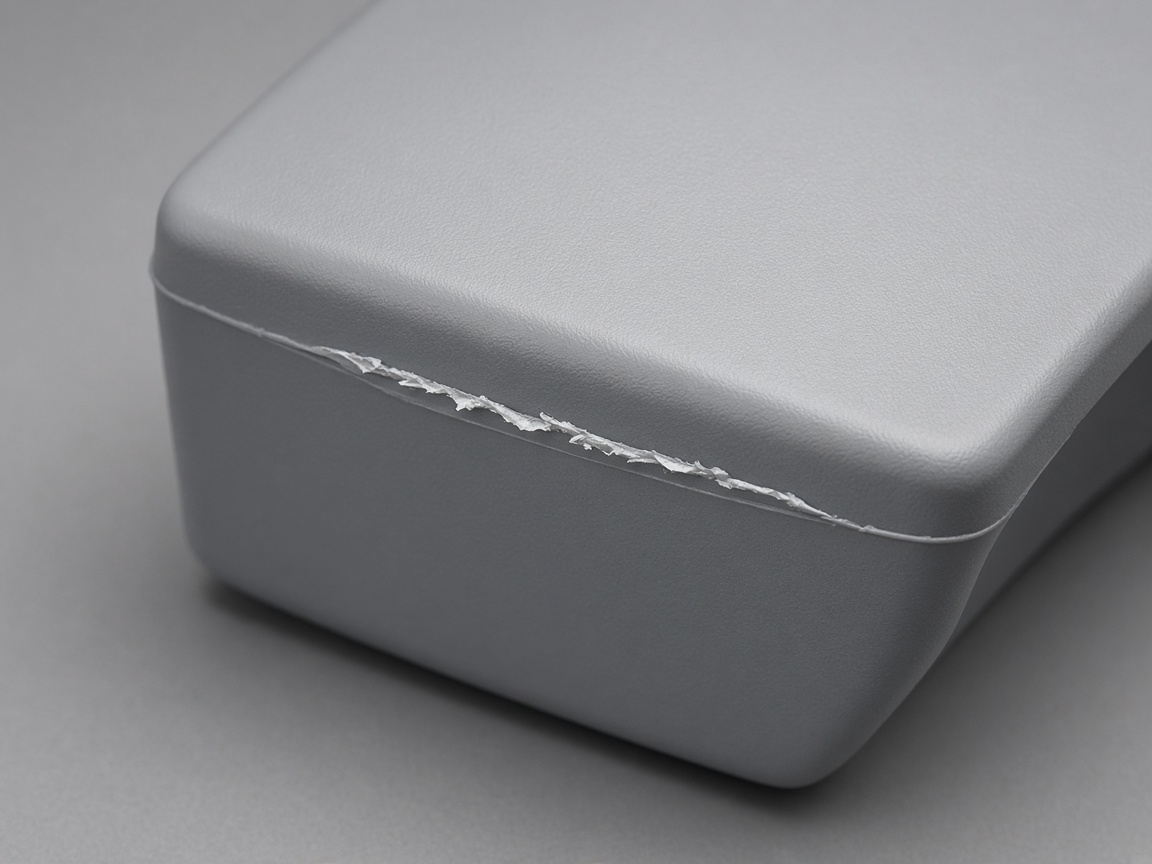
Flash excess plastic at molded part parting line close up
Flash excess plastic at molded part parting line close up
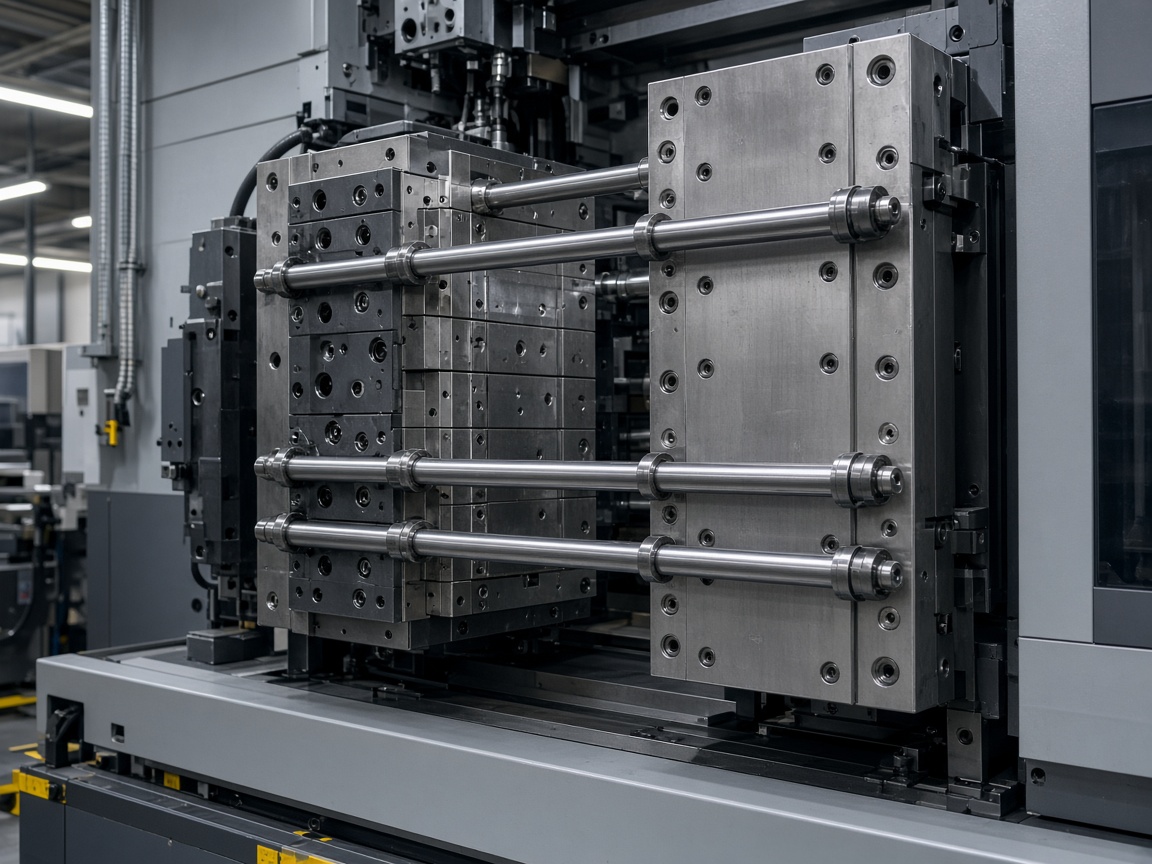
Injection molding machine platen and tie bar shut height con
Injection molding machine platen and tie bar shut height context
FAQ
Multiply projected area in square inches by a material clamp factor in tons per square inch, then add a safety margin. Use the largest projected view normal to the parting direction. Your molder validates the number against steel and process.
Tonnage is how North American catalogs express available clamp on a press. The idea is the same: how hard the machine can hold the mold closed.
Excess clamp can crush vents, overload fine steel, increase mold deflection, and put a small tool on an expensive large press without improving quality.
About 1,000 kN is roughly 102 metric tons or 112 US tons. Always confirm US ton versus metric ton on quotes because the labels differ by about ten percent.
Thin walls often need higher fill rates and resins with higher cavity pressure, which raises clamp factor in the estimate. Geometry and gate plan still drive the final press choice.
Hot runner tools usually exclude cold runner projected area from the separation force calculation, which can reduce required tonnage versus an equivalent cold runner layout.
Injection pressure is melt pressure inside the cavity. Clamping force is the press closing force that keeps the mold shut against separation load from that pressure on projected area.
Sum projected area for all cavities on the shot plus cold runner area if applicable, then apply clamp factor and safety margin. Hot runner fed impressions skip runner area in most shop calculations.
You can state constraints, but the molder still must validate projected area, flow length, and pack strategy against the tool they build.
Not by itself. Excess tonnage does not fix poor gate location, inadequate venting, or a parting line that telegraphs on a cosmetic face.
Toggle clamps are energy efficient and repeatable. Hydraulic clamps offer adjustable stroke and direct force control. Electric and hybrid presses target precision and lower energy use on sensitive production lines.
Next step
Upload CAD for a hardened steel tool quote with production piece price on the same program.