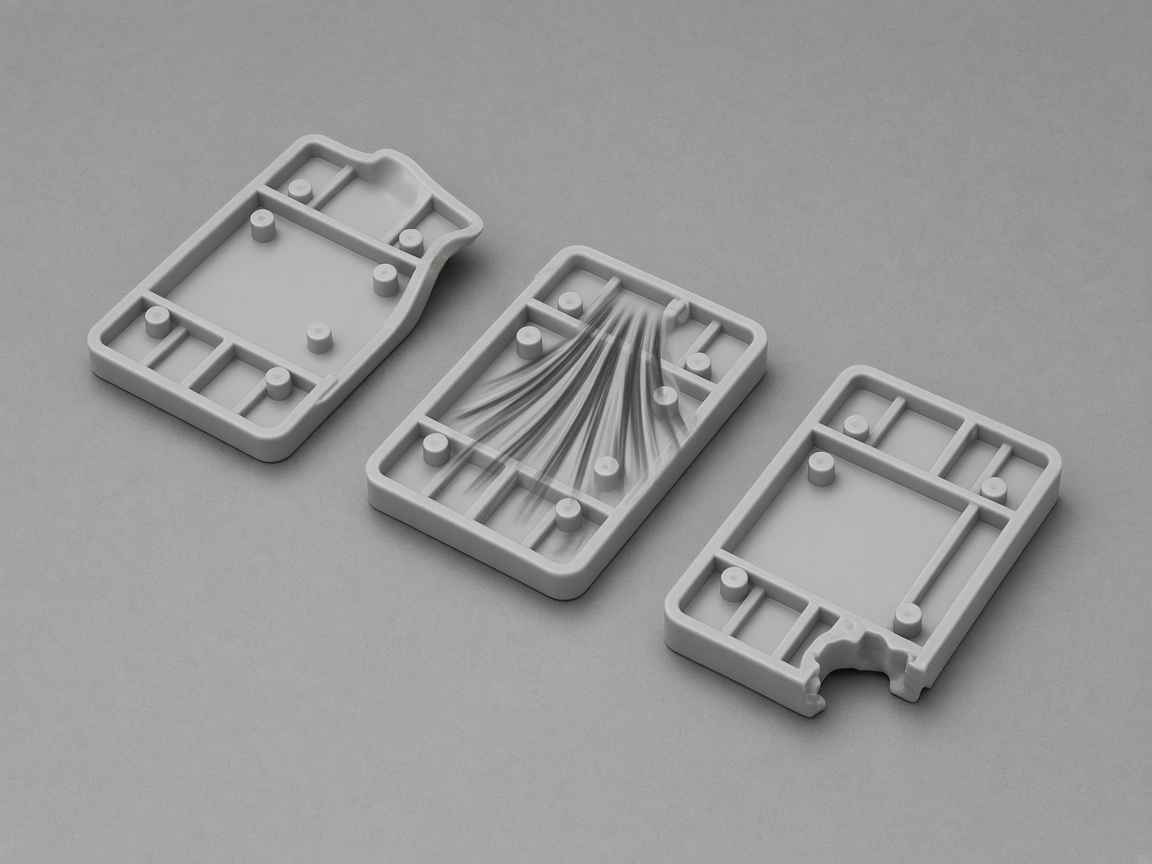
| Insufficient clamp force for projected area and peak cavity pressure | Flash only after pack and hold; parting line opens mid-cycle on thin areas | Verify clamp tonnage against projected area; reduce hold pressure in steps; confirm mold footprint on platen |
| Overfill during first-stage injection or late transfer | Flash on fill-only parts; flash at end-of-fill regions | Move transfer earlier; reduce peak fill rate near end of fill; confirm short-fill baseline before adding pack |
| Low-viscosity melt from overheating or degraded material | Flash worsens on fast cycles; discoloration or odor on same lot | Lower melt temperature within supplier band; reduce residence time; dry hygroscopic resin and verify lot identity |
| Blocked or inadequate venting at parting line | Flash with burns or short fill at last-fill points on the same cavity | Clean and restore vents; confirm air path to atmosphere; inspect for plastic trapped behind slides |
| Worn, damaged, or misaligned shutoffs and parting surfaces | Flash in the same steel location every shot; flash returns after process tweaks | Hand-clean parting line; check for nicks and galling; schedule shutoff rework or spotting when wear is confirmed |
| Contamination or debris preventing full mold close | Intermittent flash; flash after manual mold wipe fixes it briefly | Remove plastic behind leader pins and slides; verify mold open and close stops; use parting-line inspection each startup |