
Cold runner often wins
- Lower annual volume programs
- Frequent material or color changes
- Heat sensitive resins where short residence time helps
- Prototype or bridge tooling
- Simple single cavity layouts
Glossary
A cold runner is an unheated mold channel from sprue to gate that solidifies each shot. Trimmed runner slug becomes scrap or regrind. Cold runner suits many lower volume and color change programs.
Definition
A cold runner is the unheated channel in an injection mold that carries molten plastic from the sprue to the gate and solidifies with each shot.
The solidified runner ejects with the part and is trimmed as scrap or regrind feedstock.
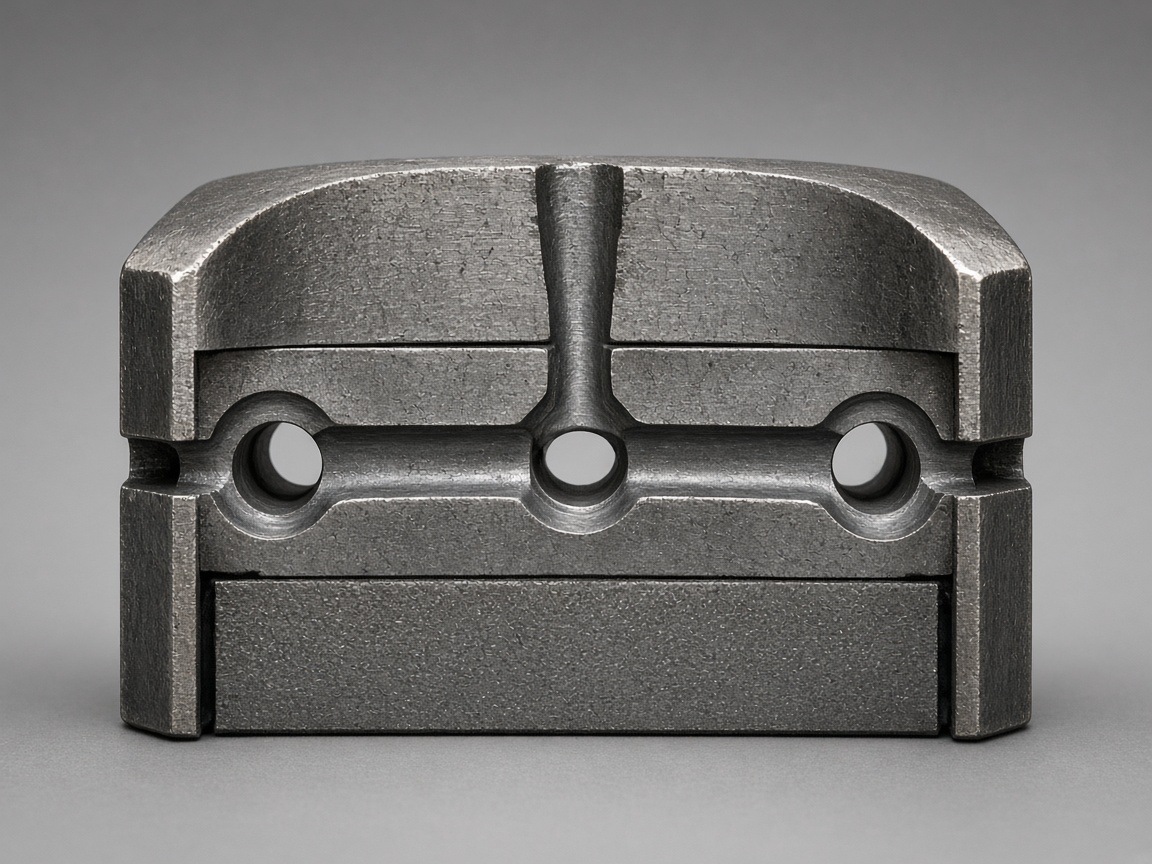
Cold runner systems are mechanically simpler than heated alternatives. They suit lower volumes, frequent material or color changes, and heat sensitive resins.
For the heated alternative, see the hot runner page. For feed path balance and a full cold versus hot comparison, see the runner glossary entry.
Tooling
Subtype, degating, and regrind limits define whether cold runner fits the program.
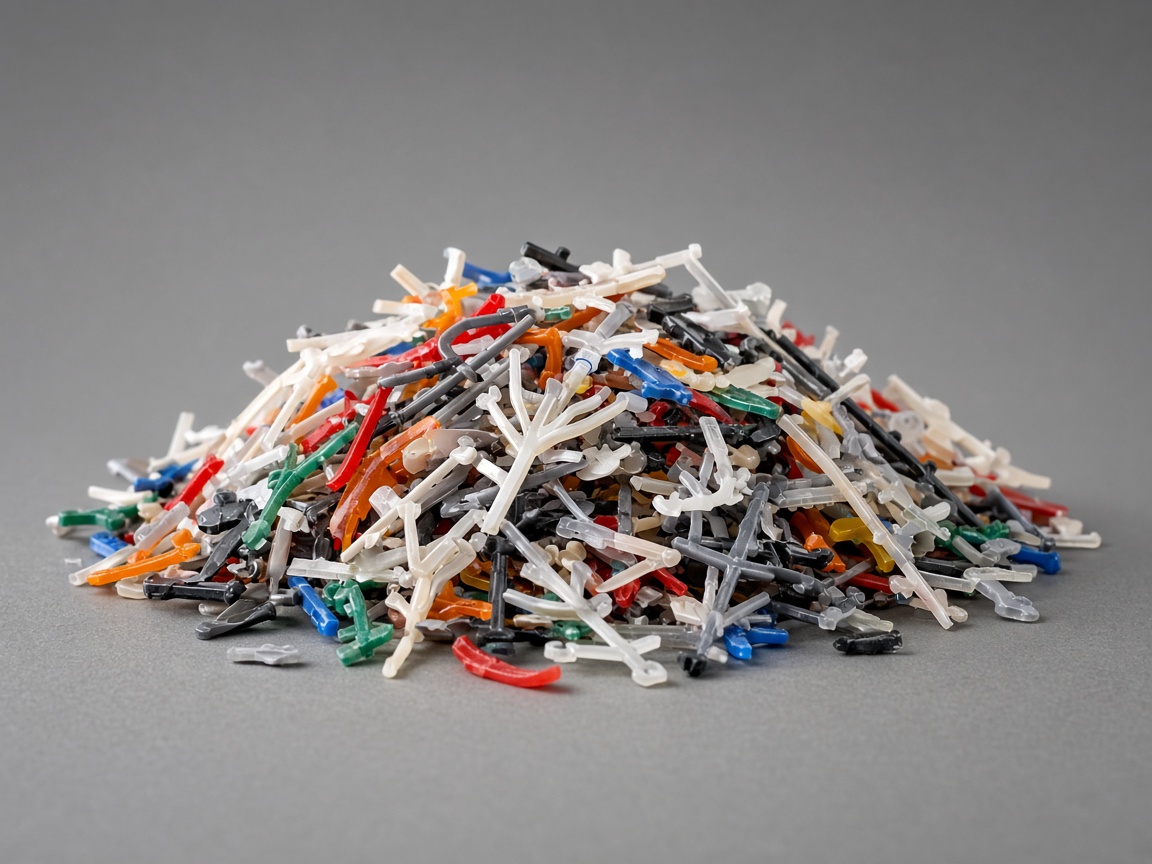
Tradeoff
Volume, scrap, and color change behavior decide runner type on your program.
Cold runner trades higher scrap and longer cycle for lower tool cost and faster color change on many layouts. Use the runner glossary entry for the full cold versus hot comparison table.
Types
Gate style links to steel detail on the tooling print.
Two plate cold runner: runner and part eject together; simplest and most common
Three plate cold runner: runner and part eject on separate plates; supports automatic degating and center gate on the top face
Submarine (tunnel) gate: gate opens into a side wall or core; degates automatically on ejection
Pin point gate: small gate mark; common on three plate layouts
Degating
Labor versus tooling cost trades off by volume and automation level.
Manual trim: operator cuts runner from the part; lowest tool cost, highest labor
Automatic degating: gate breaks during ejection on submarine, pin point, or three plate tools
Robotic degating: robot removes runner after ejection; flexible but capital intensive
Regrind
Resin spec on the RFQ sets whether regrind is allowed.
Glass filled, flame retardant, food contact, and regulated medical resin specs often restrict or prohibit regrind
Typical industry blends use limited regrind with virgin resin; high regrind ratios can degrade mechanical properties
On small parts in multi cavity tools, runner weight can exceed part weight, so scrap economics matter
Selection
These are program patterns, not universal rules. Validate on CAD, volume, and resin spec.
Tooling
Runner steel detail belongs on the mold design, not only on the part CAD.
Cold slug well: pocket at the sprue base and at runner direction changes to trap the first cool shot before it enters the cavity
Runner ejection: runner needs draft and enough ejector pins to push out without sticking; undercuts in runner layout complicate ejection
Go deeper
Each entry covers a different lever on the same tool.
Balance, cross section, and comparison table.
Runner feed pathEntry after the runner.
Gate location DFMScrap feedstock policy.
RegrindHeated feed path scope.
Hot runner alternativeUpstream of the runner.
SprueTraps at sprue and runner turns.
Cold slug wellsLayout rules on the DFM hub.
Runner design guideVisual reference
Images are selected from the NetProto Forge media library for this topic.
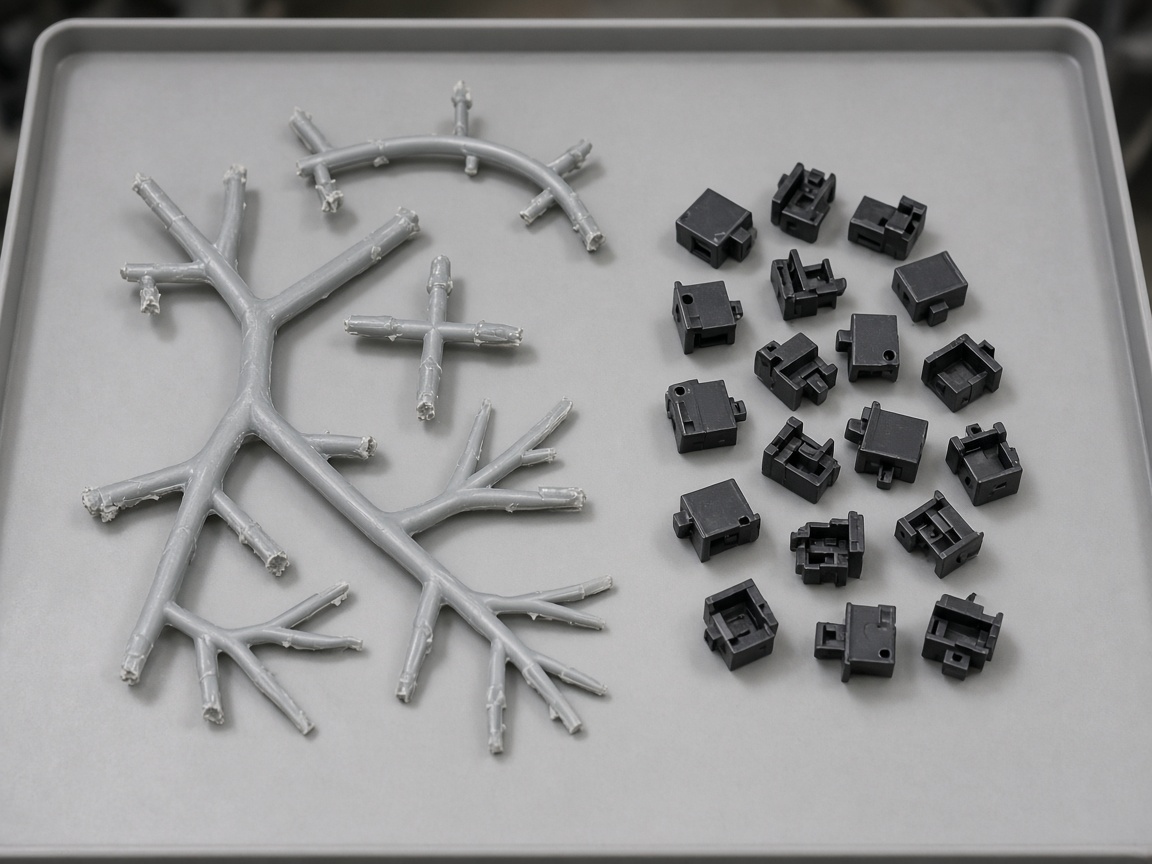
Cold runner sprue and runner slug scrap on molding tray
Cold runner sprue and runner slug scrap on molding tray
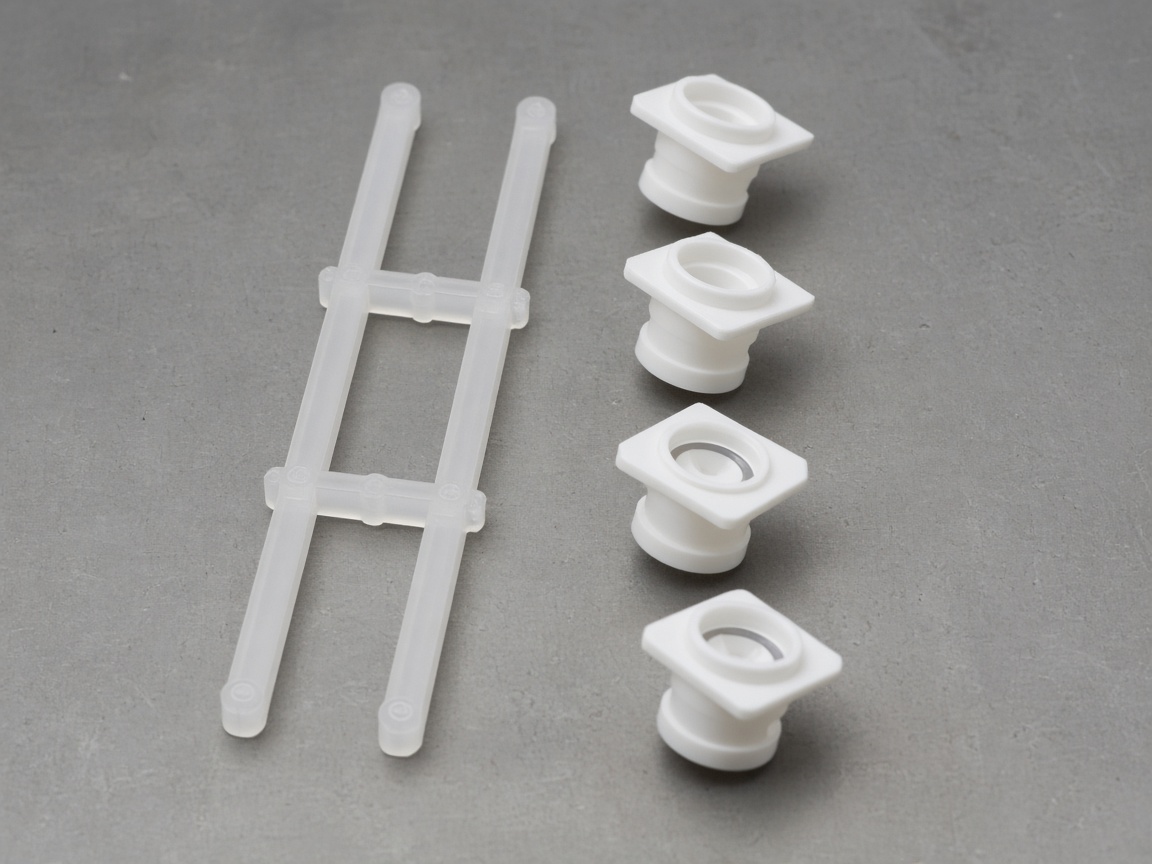
Three plate mold runner strip separated from molded parts
Three plate mold runner strip separated from molded parts
Submarine tunnel gate region on injection molded part wall
Submarine tunnel gate region on injection molded part wall
FAQ
Neither is universal. Cold runner fits many low volume and color change programs. Hot runner fits many high volume and low scrap programs. Start with annual volume, cavity count, and resin cost, then see the runner page comparison.
It depends on part size, wall thickness, cavity count, and runner volume. Small parts in multi cavity tools can see runner weight dominate the shot.
Often yes on commodity resins with an approved regrind ratio. Regulated or filled grades may prohibit regrind. See the regrind glossary and your material spec.
A mold with an extra plate so the runner strip ejects separately from the part, enabling automatic degating and some center gate layouts.
A gate that tunnels into the part wall or core and shears off on ejection. It is a degating method used on many cold runner production tools.
Tooling is often lower on cold runner layouts. Total cost depends on scrap, labor, cycle time, and volume. Low volume often favors cold runner capital.
Yes with three plate, submarine, or robotic degating. Manual trim remains common on low volume programs.
Many regulated medical, food contact, flame retardant, and glass filled specs restrict regrind. Confirm on the resin data sheet and customer quality plan.
Next step
Upload CAD with annual volume and material spec to confirm whether cold runner suits your program.