
Averaged across the shot
- Quick, and fine for general dimensions
- One worn seat is diluted by all the good ones
- Volume complaints cannot be traced to a source
Molded part guide: pipette tips
A pipette tip is a thin cone molded over a slender core, with a small hole at the end where the liquid leaves. The volume it delivers depends on that hole, the wall around it, and how the tip seals on the pipette. Every tip from every cavity has to behave the same, because the user never knows which cavity made the one in their hand.
The tip
Standard, filter, low-retention, and extended-length tips for single and multichannel pipettes.
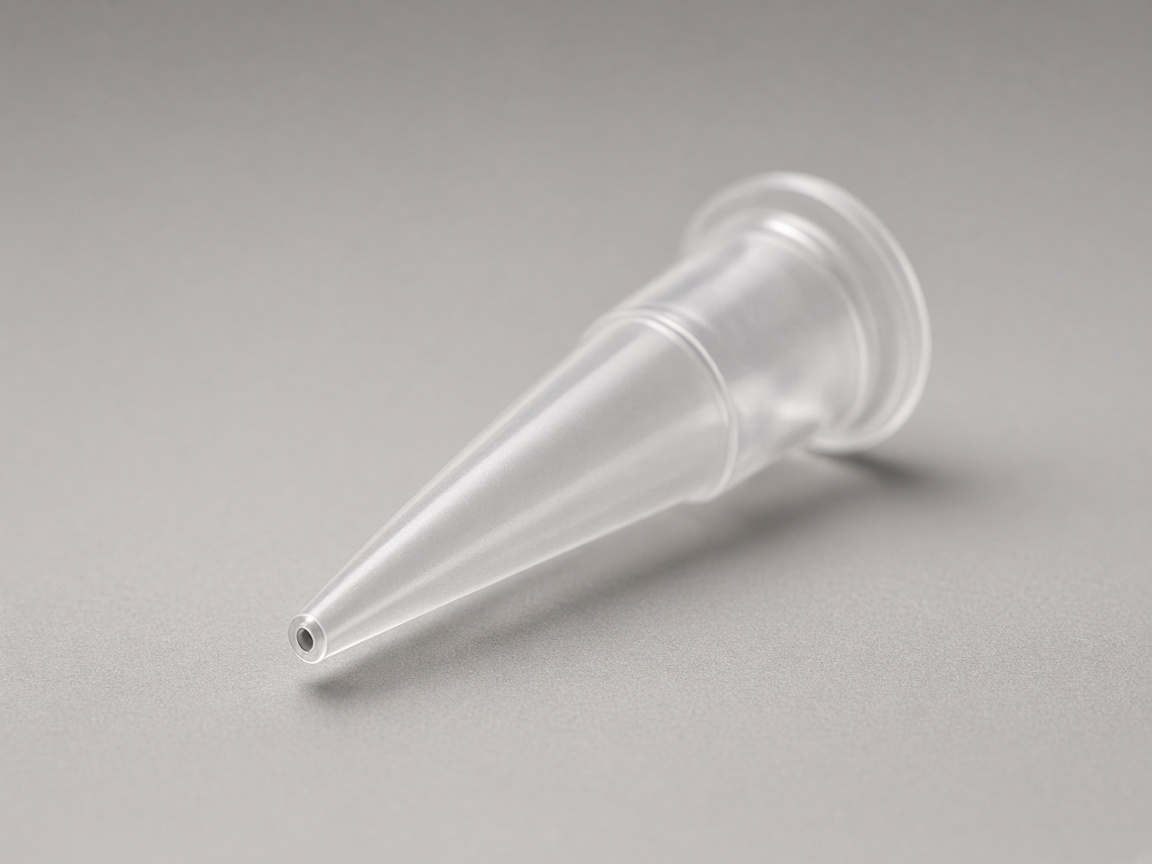
The tip is molded over a long, tapered core. Melt usually enters near the wide collar and flows down toward the narrow end, where the wall is thinnest and the plastic freezes fastest. The narrow end therefore fills last. If air is trapped there, or the melt slows too much, the end comes out short, rough, or burned, and the orifice shape suffers.
The core has to stay centered. It is slender and supported mainly at its base, so uneven filling can push it sideways and leave one side of the cone thinner. A tip with an off-center bore bends slightly as it cools, and a curved tip can touch the side of a well. In many designs the end of the core seats against the cavity steel at the orifice, which supports the core and forms the hole at the same time.
That seat is the most sensitive spot in the tool. A clean seat forms a crisp, round orifice. A worn or dirty one leaves a thin film of flash or a ragged edge, and droplets cling to it. Orifice size and edge are measured on tips from every cavity, and the seat is inspected on a schedule.
The inside surface matters too. Liquid that clings to the bore is not dispensed. A highly polished core and a polypropylene grade with few additives reduce retention, because some slip and antistatic additives can migrate to the surface and change how liquid wets it.
Features
Most accuracy problems trace back to one of these.
| Feature | Affects | How it is controlled |
|---|---|---|
| Orifice at the end | Droplet release and delivered volume | Clean core seat, measured on every cavity |
| Thin wall near the end | Complete fill and straightness | Venting at the end, balanced fill, and core support |
| Upper bore | Seal on the pipette nose cone | Consistent bore with a smooth sealing band |
| Inside surface | Liquid clinging to the wall | Polished core and a resin with few additives |
| Cavity identification | Tracing a problem to its source | A small cavity mark molded into each tip |
Service tiers
Tiers describe molded lab and device parts only. NetProto does not claim biocompatibility or certifications in marketing copy. Confirm regulated requirements with your compliance team. Part focus: Thin end fill, orifice seat, per-cavity marking.
| Tier | Environment | What matters most | Typical molded route | Quote path |
|---|---|---|---|---|
| 1 Thin end | The narrow end fills last | A short, rough, or burned orifice | PP, vented at the end | Upload CAD; expect thin-end DFM |
| 2 Orifice seat | The core seats in the steel | Flash or a ragged edge | A clean seat, measured by cavity | Instant quote; note the orifice |
| 3 Nose seal | Upper bore and sealing band | Fit on the named pipette models | Bore sized to those models | Upload CAD; name the pipette models |
| 4 Low retention | The inside surface | Liquid clinging to the bore | Polished core, PP with few additives | Instant quote; note additive limits |
| 5 Many cavities | Annual volume sets the tool size | One worn seat hidden in the average | A cavity mark on each tip | Full RFQ; note the volume target |
Materials
One primary family per line item. Put commercial grade, fillers, and environment filters in comments.
| Family | Typical use on this part type | Notes for instant quote |
|---|---|---|
| PP | Pipette tips | Field PP; note additive limits if retention matters |
| COC / COP | Only when you specify a clear grade | Name the trade name in the notes |
Filling the end
Most tip defects appear at the end, where the wall is thinnest.
Inspection
A good average can hide one cavity that is drifting.
Avoid these
Two choices that hide a bad orifice until the tips are in use.
Measuring tips as a shot average. One worn seat is diluted by the good cavities, and a volume complaint cannot be traced. Mold a small cavity mark into each tip and measure the orifice by cavity.
Picking a grade with slip or antistatic additives and not asking how the liquid wets. Those additives can migrate to the surface and change how liquid clings. If low retention matters, name a polypropylene grade with few additives on the drawing.
Drawing
The pipettes it fits and the volumes it serves shape the design.
Tip CAD with the orifice, upper bore, and wall near the end
The pipette models the tip must fit
Volume range, and any filter or low-retention requirement
Resin, and any limits on additives
Rack, refill, or bulk packing format
Expected annual volume, which sets the size of the tool
Keep reading
Other lab parts, and the defects that show up at a thin end.
Another long, slender core.
Syringe componentsThin, clear, flat lab parts.
Petri dishesRacks and trays that hold parts in position.
TraysWhy long cores shift, in more detail.
ContainersThe standard resin for tips.
PolypropyleneThin films across a small hole.
FlashReleasing a tapered part from its core.
Draft angleWhen a larger tool often pays off at tip volumes.
Single vs multi-cavityEvery part-type guide, grouped by family.
Molded parts libraryFAQ
Usually the orifice edge or the inside surface. Flash or a ragged edge at the orifice, a rough core, or surface additives in the resin let liquid cling. Check the orifice by cavity and inspect the core seat.
Nose cones differ in size and taper between pipette makers. The upper bore is designed for the models the tip must fit, often with a sealing band that tolerates small differences.
The core was pushed off center during filling, or the tip cooled unevenly. Balanced filling and support at the core end keep the cone straight.
The filter is a separate part pressed into the molded tip. Filter insertion can be quoted as an assembly step with the tips.
Annual volume sets the size of the tool. More cavities still have to fill evenly, and each tip needs a cavity mark so a worn seat can be found. Send the volume target with the CAD. Cavity count is set from your volume target during DFM review.
Next step
Upload the tip and list the pipette models. DFM feedback covers core support, venting at the end, the orifice seat, and cavity marking.