
Thermoformed tray
- Low tooling cost and quick to change
- Formed from one side of a sheet, so walls thin out at deep corners
- Pocket position and stiffness are looser, and trays wear out sooner
Molded part guide: trays
A handling tray looks simple: a flat plate with pockets. When a robot or a fixture picks parts from it blind, every pocket has to be where the drawing says, across the whole tray, on every tray in the stack. That turns shrink, flatness, and datums into the main design questions.
What a tray is for
Component handling trays, lab and sample trays, tool and kit trays, and trays that move parts between machines.
Reusable trays carry parts through production, inspection, and shipping. Some are loaded and unloaded by hand, where the pockets only need to hold the part and protect it. Many are loaded by pick-and-place equipment or robots, and then the tray behaves like a fixture: each pocket has a position and a height that the machine assumes without looking.
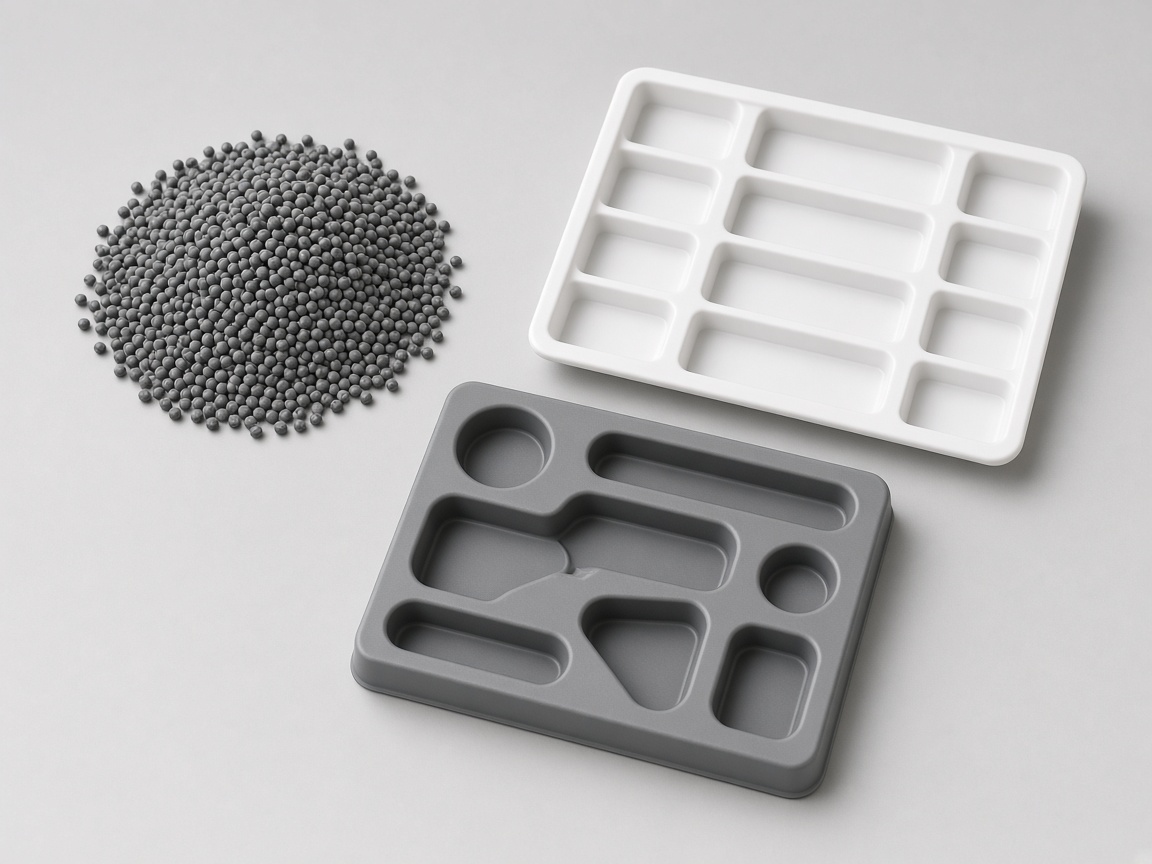
Position errors add up across a tray. The tool is cut larger than the part to allow for shrink, and if that allowance is slightly off, the error grows with distance from the datum corner. A pocket near the datum can still be in place while the pocket at the far end misses the gripper. Resins also shrink differently along and across the flow, so the pitch can be right in one direction and wrong in the other.
Flatness is the other half. A wide, shallow tray behaves like a lid: uneven cooling or uneven shrink lifts the corners or bows the middle. For automation, a lifted corner changes pocket height, and the gripper misses or crashes. A continuous perimeter wall and a grid of pocket walls stiffen the plate, and an even section across the tray keeps shrink uniform.
Trays also have to stack. Corner lugs or a perimeter step locate each tray on the one below and leave room for the parts. Stacks that must also nest when empty need a taper and a way to turn the tray so it drops into the one below instead of sitting on it.
Requirements
Manual trays need the first rows. Automated trays need all of them.
| Requirement | Why it matters | How the design responds |
|---|---|---|
| Pocket fit | The part must sit still and come out cleanly | Clearance sized to the part tolerance, with a lead-in at the top |
| Stacking | Full trays are stacked in carts and racks | Corner lugs locate the tray above and clear the parts |
| Pocket position | A robot or fixture picks each part blind | Datums on the tray, with pockets dimensioned from them |
| Flatness | Lifted corners change pocket height | Perimeter wall, pocket grid, and balanced cooling |
| Orientation | A tray loaded the wrong way round jams the line | A chamfered corner or key that fits one way only |
| Static control | Electronic parts need charge to bleed away | A static dissipative resin grade specified up front |
Service tiers
Part focus: Pocket pitch, flatness, stacking, static options. Upload CAD with critical fits and environment in notes when not modeled.
| Tier | Environment | What matters most | Typical molded route | Quote path |
|---|---|---|---|---|
| 1 Hand load | Loaded and unloaded by hand | The part sits and comes out cleanly | PP tray | Instant quote; field PP |
| 2 Robot pickup | Pick-and-place or a robot | Pocket position from one datum corner | PP, datum on the drawing | Upload CAD with the part |
| 3 Flatness | Gripper height across the tray | Corners that lift | Even section, perimeter wall, pocket walls | Instant quote; note the flatness you inspect |
| 4 Stack or nest | Full stack, empty nest, or both | Lugs or a step, and taper if they nest | Stack features in the CAD | Instant quote; note the stack height |
| 5 Wash or static | A wash cycle, or a dissipative grade | The fluid, or the resistance range you need | Grade named for that wash or range | Instant quote; name the wash or the range |
Materials
One primary family per line item. Put commercial grade, fillers, and environment filters in comments.
| Family | Typical use on this part type | Notes for instant quote |
|---|---|---|
| PP | Reusable handling trays | Field PP; note wash chemicals if any |
| ABS | Indoor kit trays | Field ABS |
Pitch
A small error per pocket becomes a large one across many pockets.

Process choice
Thermoformed trays are widely used. A molded tray is the one used when the tray is a working fixture.
Avoid these
Two choices that show up when the robot misses or the tray rocks.
Dimensioning each pocket from the pocket beside it. Those tolerances add up, and the far pocket is where the gripper misses. Dimension every pocket from the same datum corner.
Making the base a thick solid plate to keep the tray stiff. A thick section cools unevenly, and that is what lifts the corners. A perimeter wall and the pocket walls stiffen the tray. Keep the section even so shrink stays consistent across the tray.
Drawing
The tray is designed around the part it holds and the equipment that handles it.
Tray CAD and the part it holds, with the part tolerance
How trays are handled: by robot, by hand, or in a stacker
Stack height, and whether trays stack full, nest empty, or both
The datum and orientation features your equipment uses
Static control or washing requirements
Resin, color, and any identification marking
Keep reading
Other open packaging parts, and the rules for holding position.
When pocket position has to repeat across the tray, and when a formed sheet is enough.
Injection molding vs thermoformingHolding a product inside its carton.
Packaging insertsDeep tubs, jars, and bins.
ContainersAnother wide part that must stay flat.
LidsWhat molding holds without extra cost.
Standard tolerancesEven walls for even shrink.
Uniform sectionsStiffer trays and direction-dependent shrink.
Glass filled vs unfilledA tough, low cost tray resin.
PolypropyleneRepeat programs on one steel tool.
High volume moldingEvery part-type guide, grouped by family.
Molded parts libraryFlat, clear dishes with stacking rings.
Petri dishesTrays, pushers, and dividers in stores.
Retail displaysFAQ
No. NetProto quotes injection molded trays. Thermoforming suits light, low cost trays; molding suits trays that need exact pockets or many reuse cycles.
Usually a pitch error from shrink that grows with distance, or warp that lifts the corners. Measuring first parts against the datum shows which one, and the steel is corrected from that data.
Yes, with static dissipative resin grades. State the surface resistance range your process needs so the quote uses a grade listed for that range.
A tray that fits several parts usually holds none of them precisely. For automation, one tray design per part family is the usual answer.
Put the datums at one corner and dimension each pocket from those datums, not from the next pocket. Name the position tolerance you inspect to. First articles are checked from that datum, and the steel is corrected from that measurement.
Name the wash chemicals and the temperature the tray sees. The resin has to survive that wash, and the pockets still have to meet the same datums on later trips. Say if you want a stiffer grade. Filled grades can shrink differently along and across the flow, which moves the pocket pitch.
Next step
Upload the tray and the part. DFM feedback covers pocket position, datums, flatness, and stacking.