
Thermoformed insert
- Low tool cost, suited to short runs and simple pockets
- Thin sheet flexes, and pockets are formed from one side only
- Edges are trimmed sheet, and surface detail is basic
Molded part guide: packaging inserts
A packaging insert sits between two things that vary: a product with its own tolerance and a carton that varies far more. It has to hold the product still through shipping, present it well when the box opens, let it lift out easily, and never mark the surfaces the customer sees first.
Between product and box
Device kits, tool cases, vial and cartridge holders, cosmetic sets, and accessory boxes.
Most packaging inserts are thermoformed sheet, foam, or molded pulp, and for many products that is the right choice. Injection molded inserts earn their place when the insert must hold a product precisely, present it as part of a premium unboxing, survive reuse in a carry case, or run at volumes where a steel tool pays back.
Retention is designed, not assumed. A pocket that is simply the shape of the product holds it only if both are exactly nominal. Flexing fingers at the pocket edge, small crush features on the pocket walls, or a snap cradle for round items take up the product tolerance, so every unit is held the same way whether it is at the large or small end of its range.
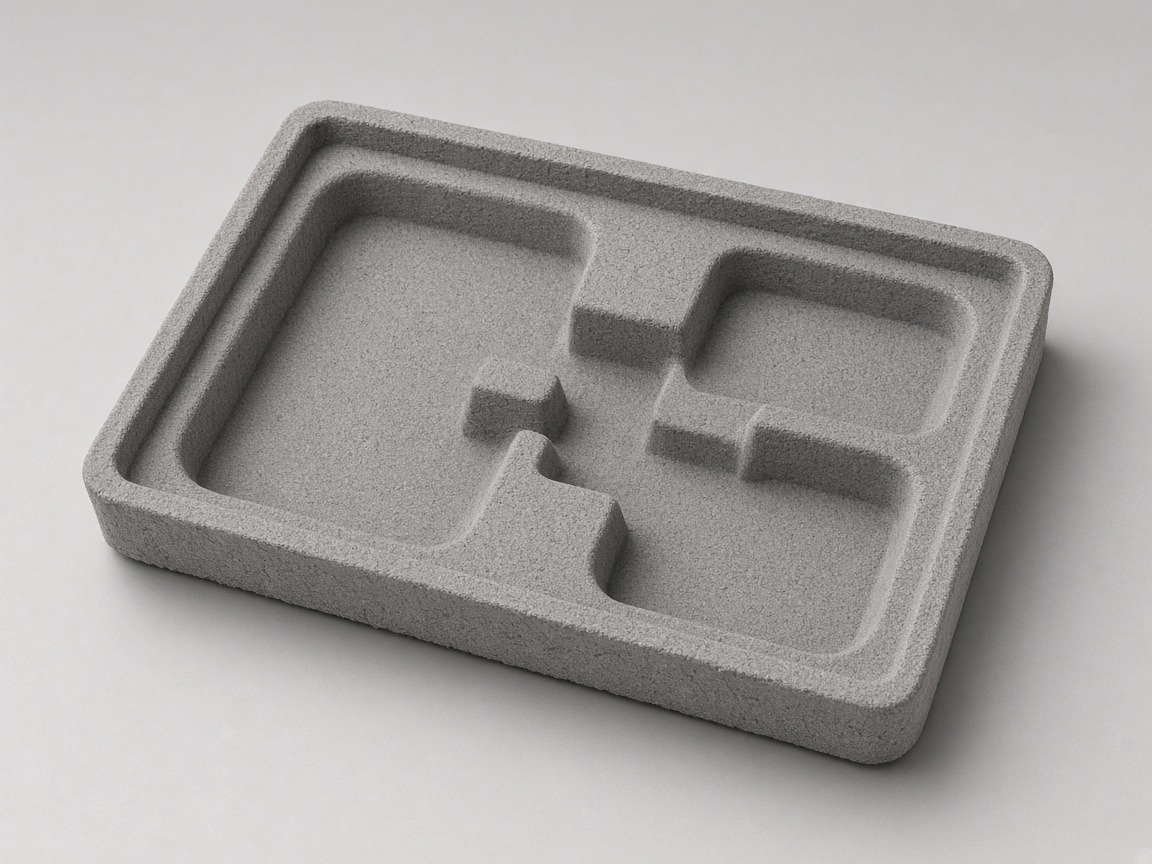
The product surface sets the limits. Anything that grips the product can scuff it, so contact goes on edges, undersides, and faces the customer does not look at first. Where a glossy face must rest on the insert, a textured contact area or a soft TPE pad overmolded onto the insert spreads the load and hides handling marks.
Getting the product out matters as much as holding it. A finger notch beside each pocket, placed so the product tips up rather than drags along a wall, keeps unboxing easy and protects the surface a second time.
Retention
The right method depends on the product shape, its tolerance, and its finish.
| Method | Suits | Watch for |
|---|---|---|
| Pocket with flexing fingers | Products with a firm edge or body | Fingers must land away from cosmetic faces |
| Crush features in the pocket | Products that vary in size | Can mark soft or glossy finishes |
| Snap cradle | Round items like vials, pens, and cartridges | Snap force changes with the item diameter |
| Soft pad by overmolding | Glossy or delicate product surfaces | Adds a second material and a second molding step |
| Finger notch | Every pocket the user empties | Notch position sets how the product lifts out |
Service tiers
Part focus: Carton tolerance, flex fingers, TPE pad inserts. Upload CAD with critical fits and environment in notes when not modeled.
| Tier | Environment | What matters most | Typical molded route | Quote path |
|---|---|---|---|---|
| 1 Push fit cap | Indoor tubes and plugs | Interference and stress relaxation | PP or LDPE-like PP | Instant quote; field PP |
| 2 Threaded closure | Repeated open/close | Thread root strength and release | PP or HDPE family in notes | Upload CAD; include thread standard in notes |
| 3 Hinged lid | Dispensing or snack box | Living hinge or pin hinge | PP hinge or separate pin design | Instant quote; field PP if living hinge |
| 4 Thin-wall tub | Deep draw container | Core shift and ejection vacuum | PP or PET depending on clarity need | Upload CAD; expect thin wall DFM |
| 5 Seal critical | Linerless or seal pin | Seal surface and warp on lid | PP or PE; TPE seal bead in notes | Full RFQ; describe seal intent |
Materials
One primary family per line item. Put commercial grade, fillers, and environment filters in comments.
| Family | Typical use on this part type | Notes for instant quote |
|---|---|---|
| PP | Caps, tubs, and living hinges | Field PP; most common for containers |
| HDPE | Chemical-resistant caps and bottles | Field HDPE in notes when specified |
| PET | Clear clamshells and jars | Field PET; gate on non-show area |
| ABS | Structural caps with snaps | Field ABS |
| TPE | Overmolded seal liners | Field TPE; 2K noted in comments |
Carton fit
Paperboard and corrugated cartons vary far more than a molded part.

Process choice
Thermoforming covers most inserts. Molding covers the ones that have to do more.
Drawing
The insert is designed against the product and the carton, so send both.
Product CAD or samples, with their size range
Carton inside dimensions, tolerance, and carton style
Cosmetic surfaces on the product that must not be touched
How the product is loaded: by hand or by automation
Any drop or shipping test the pack must pass
Color, texture, and any logo or text on the insert
Keep reading
Other packaging parts, soft contact materials, and pack-out services.
Reusable trays for handling and automation.
TraysTubs, jars, and boxes.
ContainersSnap-on lids for tubs and cases.
LidsSoft pads for glossy products.
TPETextures that hide handling marks.
Molding texturesInsert and lid from one tool.
Family injection moldingPrinting, assembly, and packaging.
Secondary operationsPackaging programs NetProto supports.
PackagingEvery part-type guide, grouped by family.
Molded parts libraryFAQ
No. NetProto quotes injection molded inserts. Foam, pulp, and thermoformed sheet suit low cost protection; molded inserts suit products that need precise retention, presentation, or reuse.
Keep contact on edges and hidden faces, texture the contact areas, or overmold a soft TPE pad where the product rests.
If the variants share a body, flexing fingers can hold a small size range. Larger differences usually need separate pockets or a separate insert.
Assembly and packaging are secondary operations that can be quoted with the insert. Describe the kit contents and pack-out in the upload.
Next step
Upload the insert, the product, and the carton size. DFM feedback covers retention, cosmetic contact, carton fit, and release from the tool.