
Overmold fit
Many grades bond to PP, ABS, PC, and PA with the right pairing.
TPE
Thermoplastic elastomer hub for overmolds, seals, and soft-touch parts. Compare families, prepare your RFQ, and upload CAD for an instant quote.
TPE
Hub page for the thermoplastic elastomer family. Process details live on SEBS, TPU, and TPV spoke pages.
Thermoplastic elastomers (TPE) are injection moldable materials that combine rubber-like flexibility with thermoplastic processing, making them a common choice for overmolded grips, seals, and soft-touch components. They fit programs that need tactile parts without vulcanized rubber tooling, including first-article validation and ongoing production with no minimum order quantity on the same hardened steel tool. TPE is a poor default when you need long-term high heat, transparent structural windows, or outdoor UV stability without a rated grade. If your part needs overmolding onto PP, ABS, or PC, TPE is often the first family to evaluate. Not sure it fits? Use the RFQ checklist below or upload CAD for DFM feedback on the instant quote platform. For a thermoset comparison, see the Silicone (LSR) page. For soft cushioning parts, see EVA . For flexible tubing and fatigue-resistant straps, see Pebax .
Key traits
Selection facts for engineering and sourcing. No machine settings on this page.
Overmold fit
Many grades bond to PP, ABS, PC, and PA with the right pairing.
Hardness band
Shore A roughly 30 to 90 across common TPE families (confirm on TDS).
Program fit
First articles through production on one hardened steel tool, no MOQ.
NetProto platform
Upload CAD for instant quoting and DFM feedback before tooling release.
Tooling lead time
Hardened steel tool build in about 10 business days on qualified programs (part complexity dependent).
Common grades
Pick one of these on the instant quote, or name any other commercial grade in the RFQ notes. Bonding success varies by the substrate resin. Confirm the bond on T1 samples before locking the grade.
| Use case | Example grade | Typical parts |
|---|---|---|
| Overmold to ABS / PC / ASA | Santoprene 8191-55 | Soft touch grips, seals, and consumer overmolds |
| Overmold to PP | Dynaflex G6713C | Flexible grips, gaskets, and PP overmold applications |
| Overmold to PC / ABS | Versaflex CE 3115 | Consumer electronics grips with silky feel |
| Overmold to nylon | Versaflex OM 6240-1 | Power tool and appliance grips on PA substrates |
| General soft touch | Dynaflex G7660-1 | General purpose grips and flexible consumer parts |
| TPU ether grade | Desmopan 3660DU | Shoe soles, hoses, and wear-resistant flexible parts |
Learn more
How to read supplier data and specify the grade on your RFQ.
What the TDS (Technical Data Sheet) values mean for a molded part.
Reading a material datasheet
How to write grade, color, and fillers so the quote matches the part.
Specify resin grade on an RFQFamily routing
Route to the spoke page for grade detail. Example trade names are illustrative only; final resin choice follows DFM and your datasheet requirements.
| Material | Typical hardness | Main applications | Common overmold substrates | Service temperature (indicative) | Example grades (reference only) |
|---|---|---|---|---|---|
| TPE-S (SEBS) | Shore A ~30-80 | Soft-touch grips, consumer seals | PP, PE, ABS | Moderate; avoid sustained high heat | Kraton G-series and similar SEBS TPEs (DFM to confirm) |
| TPU | Shore A ~60 to Shore D ~55 | Abrasion-resistant grips, strain reliefs | ABS, PC, nylon | Higher than SEBS; fluid exposure matters | Estane, Elastollan families (DFM to confirm) |
| TPV | Shore A ~45-75 | Automotive seals, weather strips | PP, EPDM-like feel on PP | Better heat/weather than many SEBS grades | Santoprene 101-XX style grades (see TPV page) |
| Flexible PVC | Shore A ~50-90 | Tubing, gaskets (non-overmold compare) | Often standalone or insert molded | Chemistry-dependent | Generic flexible PVC compounds (not a TPE) |
| Note | — | — | — | — | Common choices only; final material recommendation follows DFM analysis. |
RFQ
Prepare these details for engineering and sourcing. Upload CAD on the instant quote platform when your geometry is ready.
Target hardness (Shore A or D range) or a reference sample
Overmold substrate resin (PP, ABS, PC, PA, etc.)
Service environment: temperature range and chemical or oil exposure
Cosmetics: texture, gloss, and color match requirements
Commercial grade, or the use case to match (Shore hardness, overmold substrate (PP, ABS, PC, nylon), UV or chemical exposure)
Expected annual volume (helps cavity and tool planning)
Optional: target piece-price band for sourcing discussions
Next step
Material not finalized? Upload CAD and note TPE on the BOM. Engineers can suggest a family route after DFM review.
Go deeper
One-line differences only. Detailed performance sits on each material page.
Higher abrasion and tear resistance; route here when fluids or wear dominate.
Learn more
Dry soft-touch feel and cost-friendly overmolds on PP and ABS.
Learn more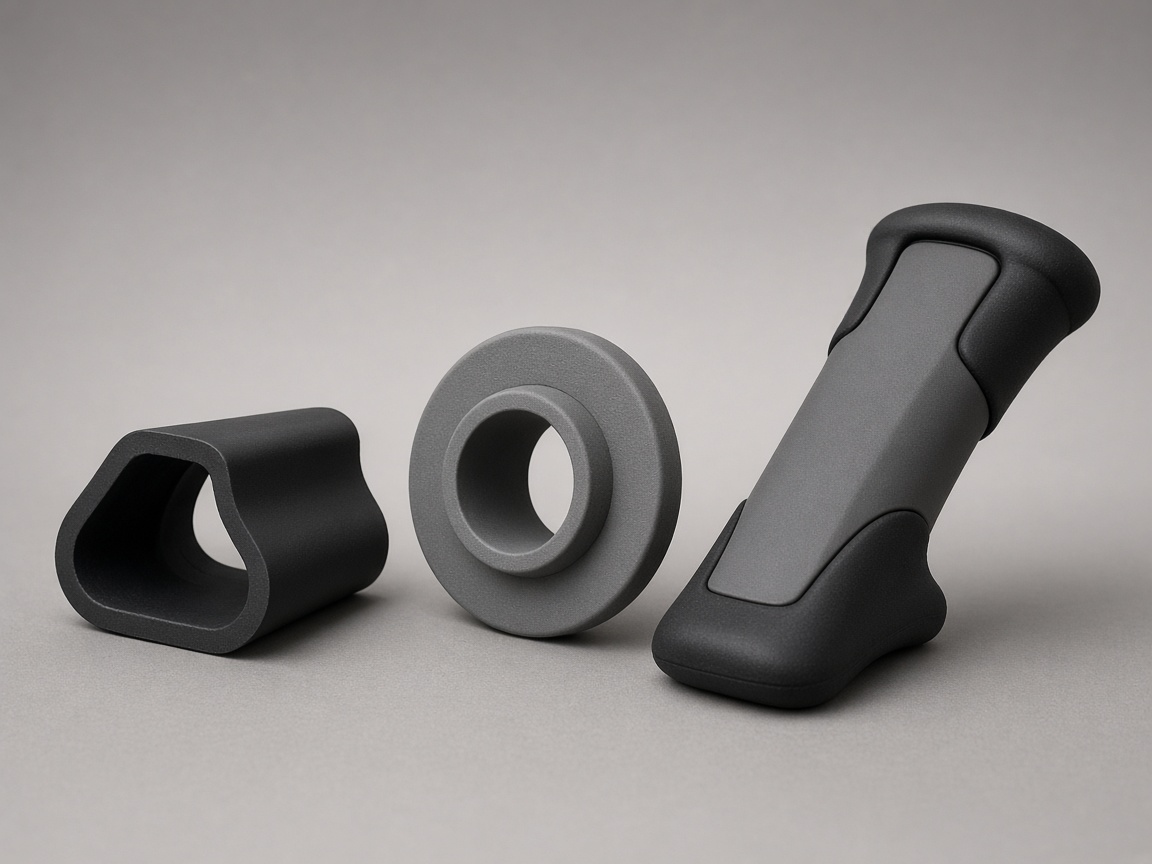
Heat and weather oriented dynamic vulcanized elastomer on PP.
Learn more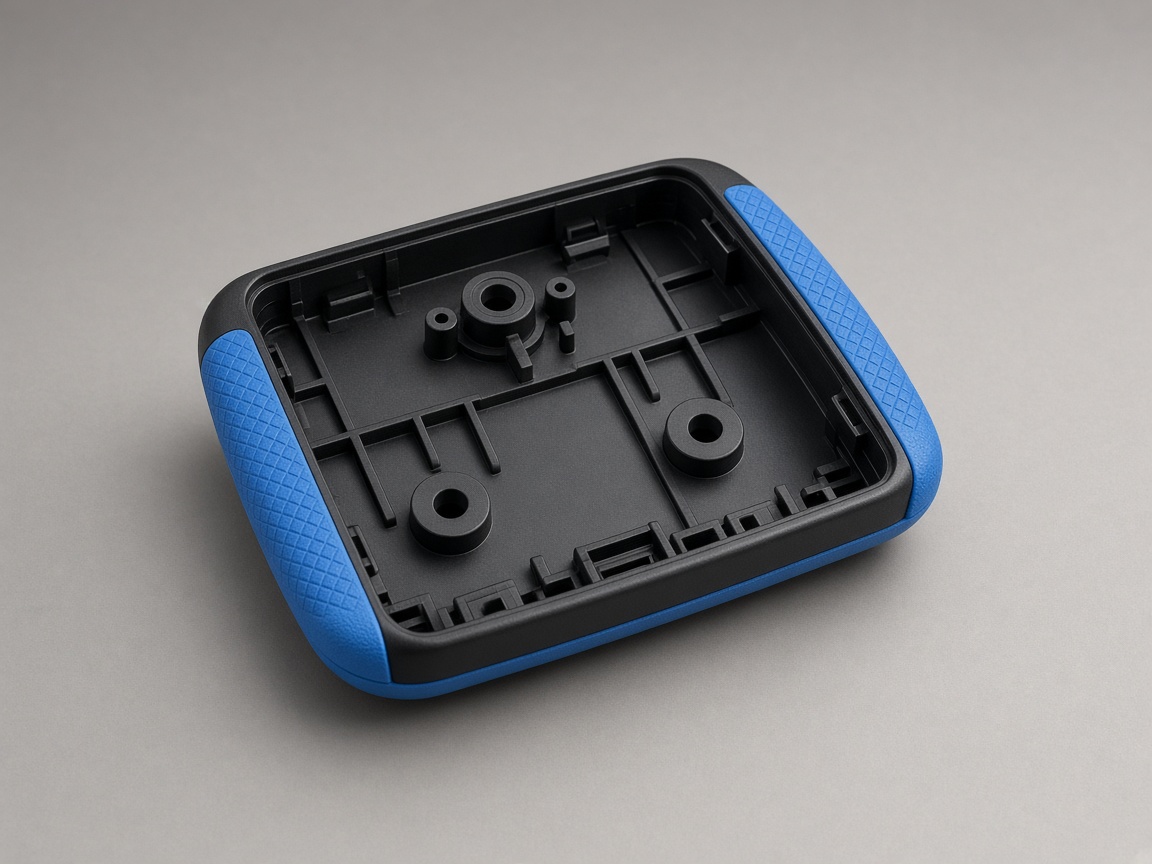
Two-material programs, bond lines, and when to pair rigid + elastomer.
Learn moreFAQ
TPE is the family name. It covers SEBS, TPU, and TPV. Choose TPU when abrasion and tear strength dominate. SEBS is the usual dry soft-touch route. The TPU page covers the wear case.
TPV is the TPE sub-family with vulcanized rubber domains. Choose it when heat, weather, or under-hood exposure matters more than a dry soft touch. Confirm the grade on the supplier TDS.
Yes, many TPE and TPV grades are formulated to bond to PP and ABS in the same cycle when the substrate and elastomer are paired correctly. At NetProto, we recommend listing both resins on the RFQ, sharing hardness targets, and validating peel strength on T1 samples before you approve cosmetics.
It depends on the specific grade: some TPEs are tolerant while hygroscopic types need drying per the supplier TDS. At NetProto, we do not publish a single drying recipe on this hub page; confirm moisture limits on the SEBS, TPU, or TPV spoke for your chosen grade and attach the TDS to your project.
TPE and TPU are thermoplastics molded in standard injection machines, while LSR is a thermoset silicone with different tooling and curing. NetProto focuses on thermoplastic injection molding and overmolding; we explain LSR for comparison but do not quote LSR molding as a NetProto service.
Some TPE grades are marketed for regulated uses, but compliance comes from the resin supplier documentation, not from NetProto certifications. At NetProto, ask your compliance team for the required statements, list them on the RFQ, and we mold to the specified commercial grade you supply or approve.
NetProto has no minimum order quantity on molded parts from your production tool. That helps TPE programs start with small validation runs and scale without a separate prototype tool. Upload CAD on the instant quote platform to scope tool and part pricing for your volume.
TPE prototyping uses the same hardened steel injection tool as production, so early shots reflect real fill and bond behavior. Silicone prototyping usually means LSR thermoset processing and different tooling, which is not the same workflow as thermoplastic injection molding. At NetProto, upload CAD on the instant quote platform for TPE overmold programs and DFM feedback on the steel tool you keep.
Next step
List TPE or the target hardness on your RFQ notes. We route detailed grade questions to DFM.