
Clarified polypropylene
- Low cost and tough, the standard for disposable syringes
- Translucent to clear, good enough to read graduations
- Some grades yellow or lose toughness after radiation sterilization
Molded part guide: syringe components
A syringe barrel is a long, thin tube molded over a long, slender core, and the stopper has to slide the full length of that bore with an even force. Small variations in bore diameter or wall that would not matter on most parts show up here as sticking, leaking, or a dose that is hard to control.
The barrel
Barrels, plunger rods, tip caps, and finger flanges for disposable and prefilled syringes.
The barrel core is long compared with its diameter, so it behaves like a cantilever in the tool. If melt reaches one side before the other, the pressure bends the core and the wall comes out thicker on one side. A thin side and a thick side shrink differently, and the bore ends up slightly oval or bowed. Most barrels are gated at the tip end, on the axis, so the melt flows down all sides of the core together.
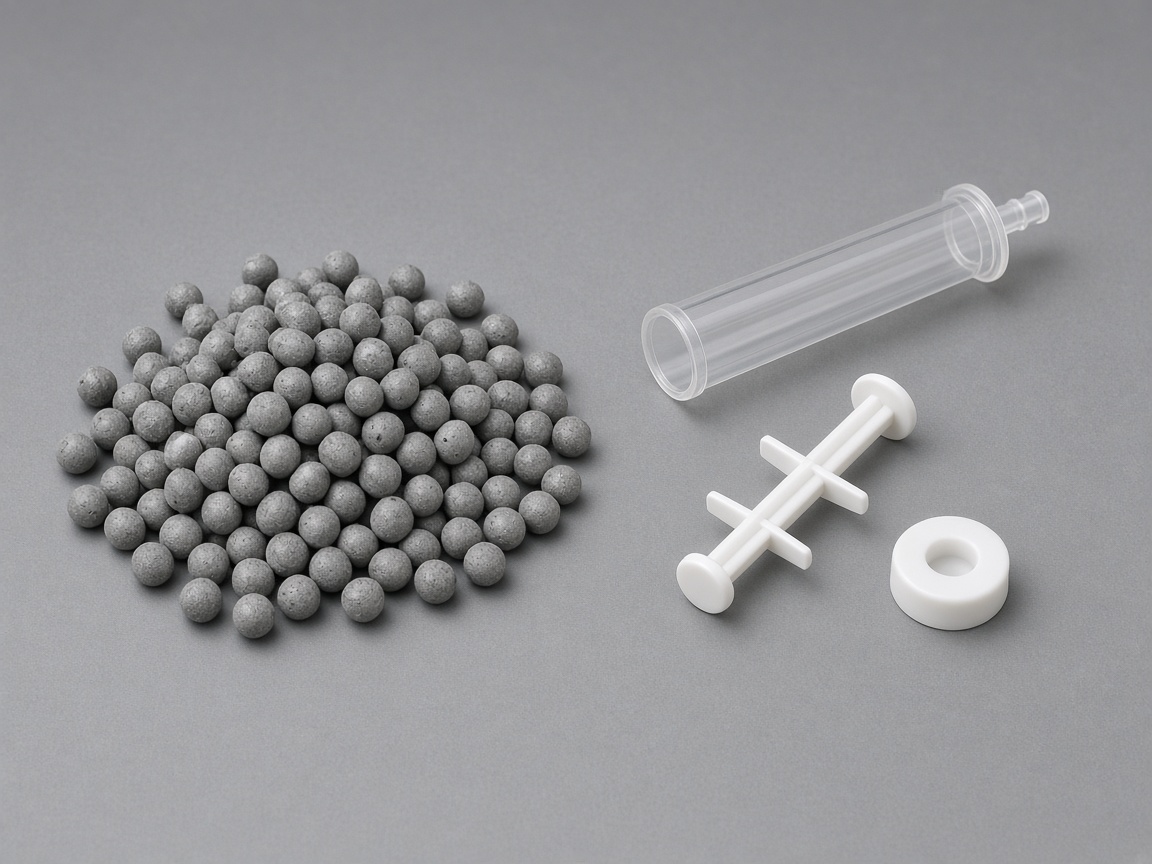
The stopper is an elastomer part that seals by being squeezed into the bore. Glide force, the push needed to move it, depends on how much it is squeezed, and that depends on the bore. A bore that tapers, goes oval, or varies between cavities gives a syringe that starts hard, jumps, and then runs easy. Consistent bore size along the length and from cavity to cavity is the main quality target.
Release is the other constraint. The barrel shrinks onto the core, and the bore wants as little taper as possible for an even glide. A highly polished core, careful cooling of the core, and a stripping action that pushes the barrel off evenly around the flange keep the part from scuffing or stretching on ejection.
Clarity matters because users read the dose through the wall. Clarified polypropylene is the common barrel resin for disposable syringes. Cyclic olefin polymers and copolymers are used where glass-like clarity, low moisture pickup, or low interaction with the drug is needed. Plunger rods are usually polypropylene, molded with a cross-shaped section for stiffness at low weight.
Parts and priorities
Each part has one or two features that decide whether the syringe works.
| Part | Critical feature | What controls it |
|---|---|---|
| Barrel bore | Even diameter along the length and between cavities | Core alignment, balanced gating, and core cooling |
| Luer tip | Taper that seals with a mating connector | Tip geometry cut to the luer standard, and no flash at the end |
| Finger flange | Carries the thumb load without cracking | Rounded junction between flange and barrel |
| Plunger rod | Straight and stiff enough not to buckle | Cross-shaped section and balanced cooling |
| Graduations | Readable scale aligned to the bore | Pad printing located from a molded datum |
Service tiers
Tiers describe molded lab and device parts only. NetProto does not claim biocompatibility or certifications in marketing copy. Confirm regulated requirements with your compliance team. Part focus: Barrel core shift, glide force, luer tip geometry.
| Tier | Environment | What matters most | Typical molded route | Quote path |
|---|---|---|---|---|
| 1 Non-fluid contact | Housing exterior, handles | Disinfectant stress cracking | PC/ABS or PC | Instant quote; note wipe-down cleaners in comments |
| 2 Fluid path plastic | Barrels, tips, trays | Fill, core shift, and clarity | PC, COP, or PP per program notes | Upload CAD; material pending common early |
| 3 Thin end feature | Pipette tip or orifice | Venting and end fill | PP or specialized clear PP in notes | Upload CAD; expect thin feature DFM |
| 4 Repeated sterilization | Handles and enclosures | Heat and chemical aging | Heat-resistant family on supplier TDS | Full RFQ; attach target grade when known |
| 5 High cavity count | Multi-tip racks or trays | Balance fill and marking | Family TBD with tooling layout | Full RFQ; note cavity count target |
Materials
One primary family per line item. Put commercial grade, fillers, and environment filters in comments.
| Family | Typical use on this part type | Notes for instant quote |
|---|---|---|
| PC | Clear components and housings | Field PC; supplier docs for regulated programs |
| PP | Lab trays and low-cost disposables | Field PP; confirm fluid compatibility in notes |
| COC / COP | Optical lab consumables when specified | Name trade name in RFQ notes only |
| PC/ABS | Device housings without fluid contact | Field PC/ABS |
| ABS | Non-critical covers and internals | Field ABS |
The tip
A slip or lock luer tip must seal against connectors from any supplier.

Barrel resin
Both mold well. They differ in clarity, stiffness, barrier, and price.
Drawing
The bore and tip carry most of the requirements.
Barrel, plunger rod, and tip cap CAD, with the stopper drawing
Bore diameter tolerance and how it is measured along the length
Tip type: slip or lock luer, or a staked needle design
Resin, and the sterilization method the product uses
Graduation artwork and its position relative to the bore
Target glide force, if the stopper and lubricant are already chosen
Keep reading
Other fluid path parts, and the tooling behind long bores.
Luer connectors, stopcocks, and clamps.
IV componentsSmall dosing parts with tight holes.
Inhaler componentsAnother long, slender core.
Pipette tipsWhy deep cores shift, in more detail.
ContainersReleasing internal threads from the core.
Threaded capsThe common barrel and plunger resin.
PolypropyleneWhy the tip must be flash free.
FlashPrinting graduations after molding.
Secondary operationsEvery part-type guide, grouped by family.
Molded parts libraryFAQ
Usually the bore is tighter at one end or slightly oval, so the stopper is squeezed harder there. Check bore size along the length before changing the stopper or lubricant.
The core deflected during filling because melt reached one side first. Gating on the axis at the tip end and keeping the core well supported and cooled prevent it.
Raised or recessed marks can be molded, but they are hard to read on a clear barrel. Most barrels use pad printed graduations located from a molded feature.
They are usually separate tools because the parts differ so much in shape and fill. A barrel and its tip cap, being more alike, sometimes share a family mold.
Next step
Upload the syringe parts and the stopper. DFM feedback covers core support, gating, bore consistency, tip geometry, and printing.