
Stripped caps
- Simple tool with no rotating core
- Needs PP, PE, or a similar resin and a shallow rounded thread
- Thread fit varies a little more, since the skirt stretches on every ejection
Molded part guide: threaded caps
An internal thread is an undercut all the way around. The cap cannot simply be pulled off the core that formed it. How the thread is released, by stretching over the core, by unscrewing, or by a core that shrinks inward, decides which resins you can use, what thread shape you can have, and much of the tool cost.
The release problem
Jar lids, container caps, tube caps, and industrial caps all have a thread molded on the inside.
An external thread, like the one on a jar neck, can be formed by two cavity halves that open sideways, leaving a faint parting line across the threads. An internal thread in a cap is formed on the core, inside the part, and the core cannot be split the same way. Something has to give: the cap, the core, or the motion of the part leaving the core.
For many polyolefin caps the cap gives. The part is pushed off the core while still warm, the skirt stretches over the thread crests, and it snaps back. This is called stripping, and it keeps the tool simple. It only works when the thread is shallow and rounded, the resin can stretch without permanent damage, and nothing outside the skirt stops it from expanding as it leaves.
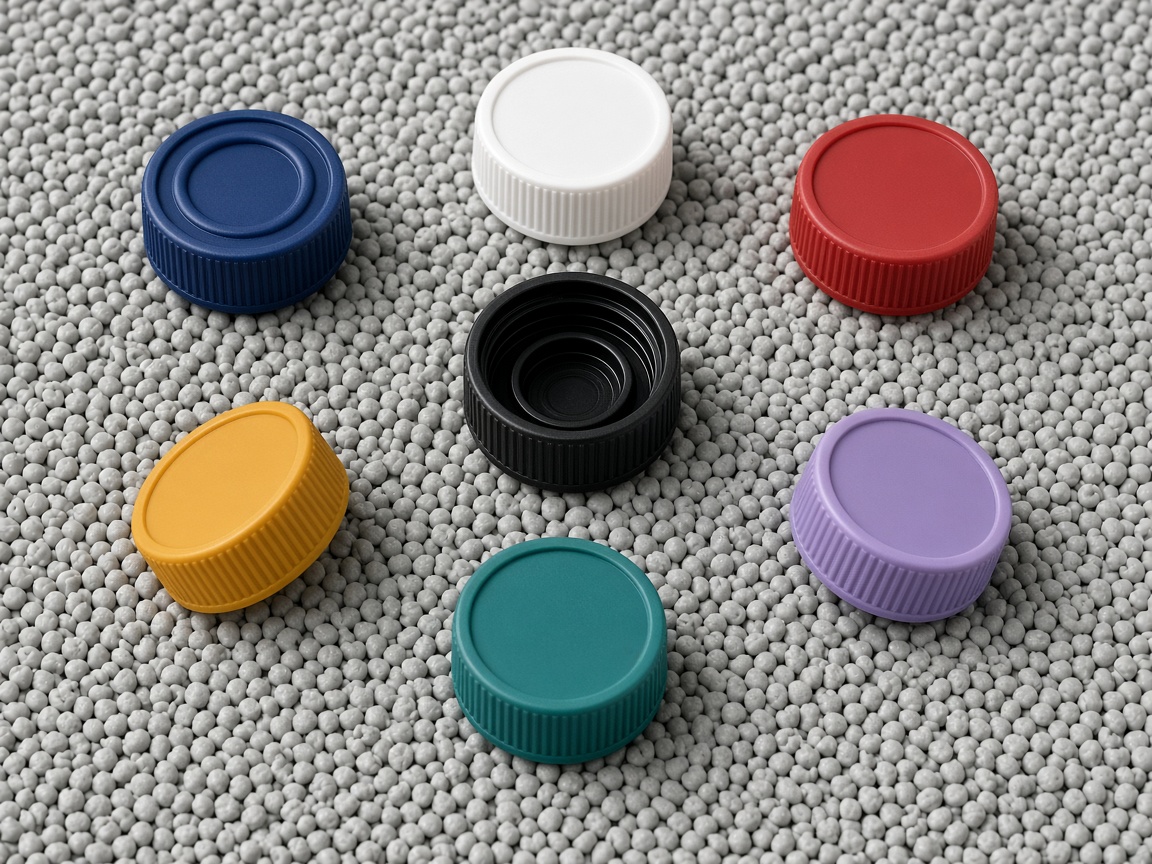
When the cap cannot stretch, because the resin is stiff, the thread is deep or square, or the form must stay exact, the core has to move. An unscrewing core rotates out of the part while the cap is held from turning. A collapsible core is built from segments that fold inward, releasing the thread without rotation. Both add mechanism and cost to the tool, and unscrewing usually adds cycle time.
That is why the thread is worth settling early. A rounded, shallow thread in PP or PE can often be stripped, while a sharp buttress thread in a stiff resin almost never can. Changing the thread profile after the tool is built can mean changing the whole release mechanism.
Release methods
Each method trades tool cost against resin and thread freedom.
| Method | Suits | Trade-off |
|---|---|---|
| Stripping off the core | PP, PE, and soft resins with shallow rounded threads | Simplest tool, but limits thread depth and resin |
| Unscrewing core | Stiff resins, deep or square threads, several turns | Holds exact thread form; more tool cost and cycle time |
| Collapsible core | Larger diameters and interrupted threads | No rotation needed; faint marks where segments meet |
| Move the thread outside | Designs where the cap can become a plug or sleeve | External thread forms in split cavity halves or side actions |
Service tiers
Part focus: Thread release: collapsing cores and outside threads. Upload CAD with critical fits and environment in notes when not modeled.
| Tier | Environment | What matters most | Typical molded route | Quote path |
|---|---|---|---|---|
| 1 Strip off the core | PP or PE, shallow rounded thread | The skirt must be free to expand | PP or PE | Instant quote; field PP or PE |
| 2 Unscrewing core | Stiff resin, deep or square thread | The cap must not turn with the core | Knurl or grip teeth on the drawing | Upload CAD; note pitch and turns |
| 3 Collapsible core | Large diameter or interrupted thread | Segments fold inward | Faint marks where segments meet | Full RFQ; note the diameter |
| 4 Seal | Liner, plug, or gasket | The seal surface on the cap | Method named on the drawing | Instant quote; describe the seal |
| 5 Thread outside | Cap can be a plug or sleeve | Thread forms in the cavity halves | No internal undercut | Upload CAD; say if the thread can move outside |
Materials
One primary family per line item. Put commercial grade, fillers, and environment filters in comments.
| Family | Typical use on this part type | Notes for instant quote |
|---|---|---|
| PP | Shallow rounded threads that strip | Field PP |
| HDPE | The same stripped caps when you specify HDPE | Field HDPE |
Holding the cap still
A cap will turn with the core unless the tool holds it.

Tool choice
The cheaper tool is the right one only if the cap can live with its limits.
Avoid these
Two choices that decide the release mechanism.
Asking a stiff resin, or a deep or square thread, to strip off the core. Stripping works when the thread is shallow and rounded and the skirt can stretch and come back. A sharp buttress thread in a stiff resin almost never can. Settle that before the tool is built, because it decides how the thread is released.
An unscrewing cap with a smooth outer skirt and nothing else for the cavity to grip. The core will try to spin the cap with it. A knurl or grip teeth on the skirt stop that. A smooth skirt needs teeth on the top face or the rim.
Drawing
These decide the release method, so they are needed before a tool quote.
Cap CAD with the thread profile, pitch, and number of turns
The mating neck, or the thread standard it must fit
Resin, or the service conditions if the resin is still open
Whether the outer skirt can carry a knurl or grip teeth
Sealing method: liner, plug, or gasket
Expected annual volume, which drives cavity count and release method
Keep reading
Other caps, threaded parts, and the tooling behind them.
Neck finish, seal, and tamper bands.
Bottle capsFlip-tops and dispensing tops.
ClosuresPush-on caps with no thread at all.
CapsThreaded bowls under pressure.
Filter housingsFeatures that lock a part in the tool.
UndercutsMoving steel for external features.
Side actionsWhen a metal thread is the better answer.
Molded threads vs insertsHow cavity count changes cap cost.
Single vs multi-cavityEvery part-type guide, grouped by family.
Molded parts libraryTooling for caps with full threads.
Unscrewing moldsThread protectors for pipe ends.
Oil and gasFAQ
Generally no. PC and other stiff resins crack or deform permanently when forced over the thread. Stiff resins need an unscrewing or collapsible core.
Stripping stretches the thread on every shot, and how fully it recovers varies with temperature and timing. For a tighter fit, review thread depth and profile, or move to an unscrewing core.
It adds tool cost and usually some cycle time. Whether that pays back depends on volume and on what the thread has to do, which is reviewed in DFM before the tool is quoted.
Sometimes. If the cap can become a plug or sleeve that screws into the container, the thread is external and forms in split cavity halves, which is often simpler than releasing an internal one.
When the diameter is large or the thread is interrupted, and the cap should come off without rotating. The core is made of segments that fold inward. They can leave a faint mark where the segments meet.
Liner, plug, or gasket. Name which one the cap uses, along with the thread profile, pitch, and number of turns. The seal surface is part of the same quote as the release method.
Next step
Upload the cap and its mating thread. DFM feedback covers thread profile, release method, anti-rotation features, and cavity count.