
Molded thread
- No extra parts, and the port is sealed in one molded wall
- Tapered pipe threads push the plastic outward as they tighten, which is where overtightening cracks start
- Straight threads with an O-ring or flat seal load the plastic far less
Molded part guide: filter housings
A filter housing is a pressure vessel that someone unscrews by hand every few months. The thread, the seal, and the plastic around them have to survive both the pressure and the person.
The job
The bowl rarely bursts in the middle. Cracks start where the housing is joined, sealed, or connected.
A typical housing has two molded parts: a head with the inlet and outlet ports, and a bowl that threads onto it and holds the cartridge. An O-ring between them makes the seal. Every time the cartridge is changed, the bowl is unscrewed and tightened again, often with a wrench, and often too hard.
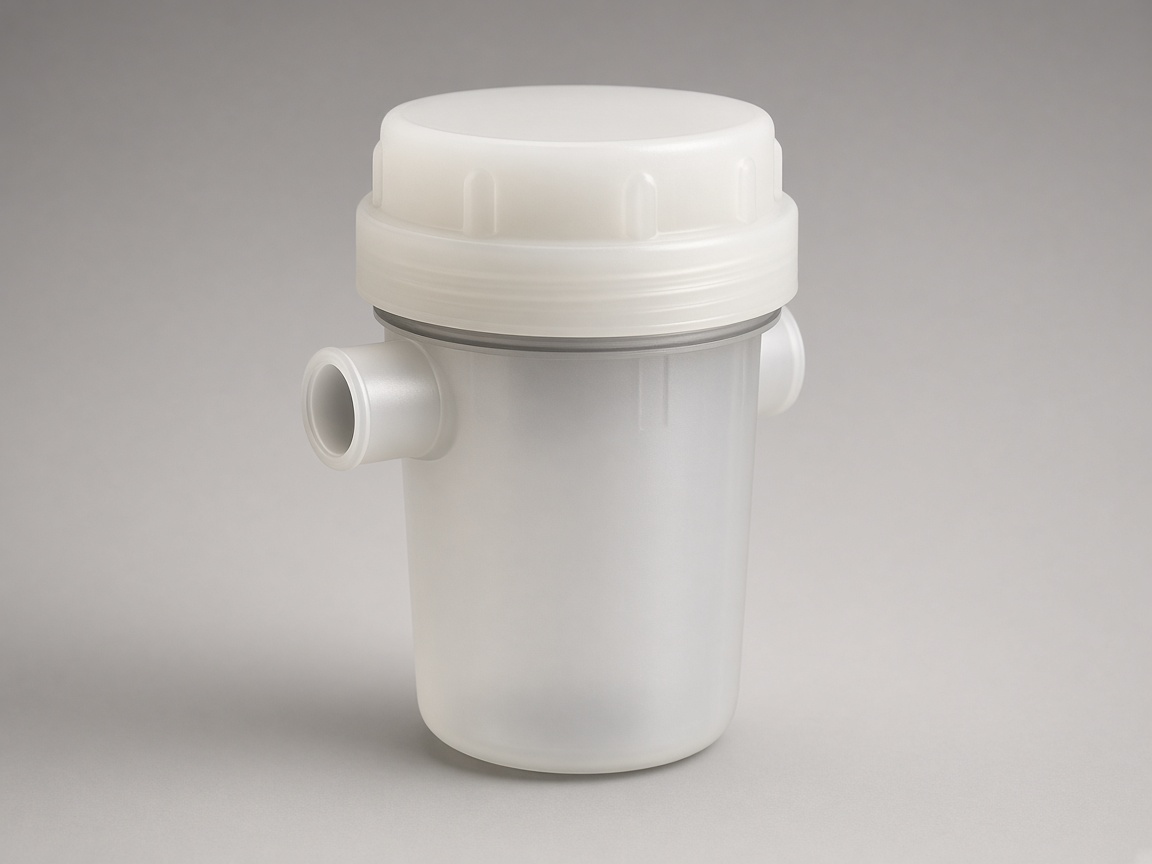
A case published by the Society of Plastics Engineers describes molded filter bodies that cracked just below their internal pipe thread in the field. The parts had been molded properly and passed pre-production testing. The cause was a weld line sitting in the thread, combined with installers tightening the fitting harder than the test technician had. The test was right about the part and wrong about the user.
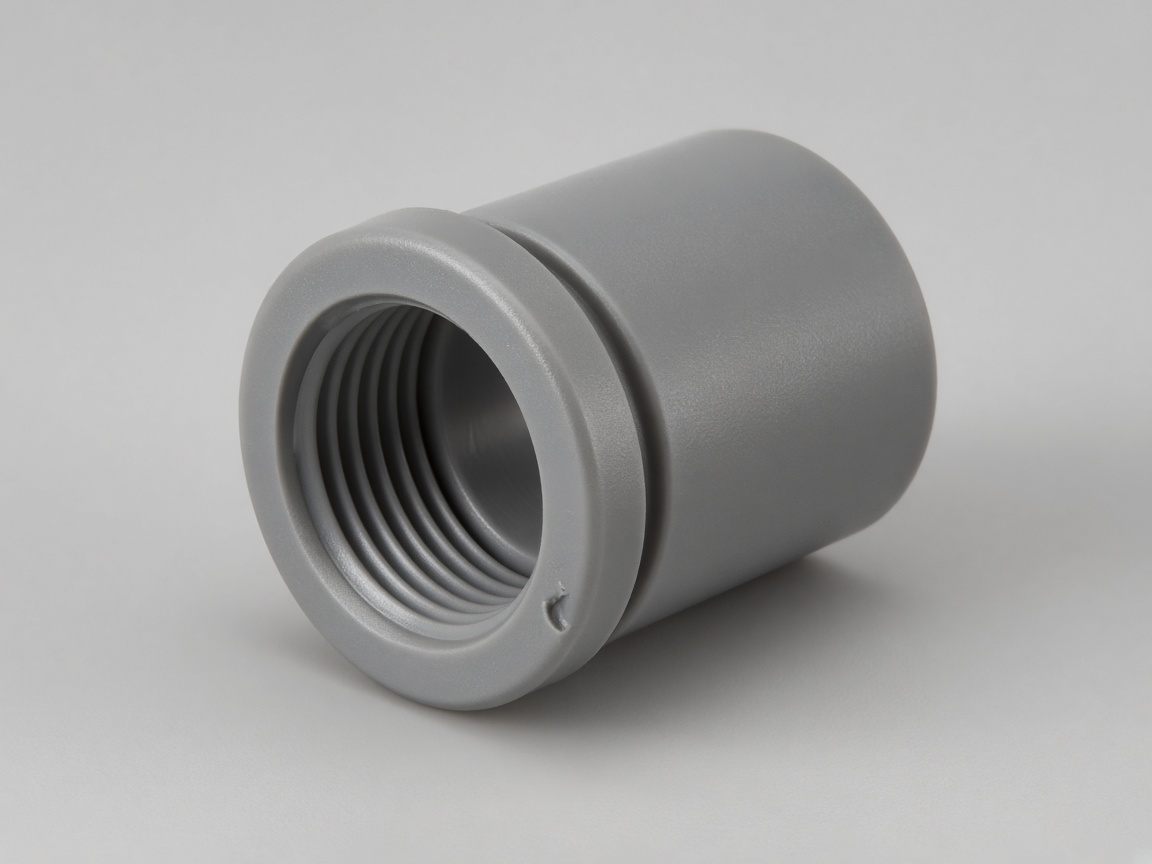
The lesson carries over to any filter housing: keep weld lines out of threads and sealing faces, give the thread a positive stop so it cannot be overtightened, and test the way the product will really be installed.
Resin
General behavior. The fluid, temperature, and any drinking water listing decide the grade.
| Resin | Where it fits | Trade off |
|---|---|---|
| Polypropylene | Opaque bowls and heads for water and many chemicals | Chemical resistant, but you cannot see the cartridge |
| Glass-filled polypropylene or nylon | Heads and bowls for higher or pulsing pressure | Stiffer and more creep resistant, and glass makes weld lines weaker |
| SAN or copolyester | Clear bowls so the user can see when the cartridge is dirty | Clear resins are more sensitive to chemicals and notches, so thread roots need care |
| Polycarbonate | Clear, tough bowls for air and industrial fluids | Some drinking water and food programs restrict it, so check your specification first |
| Polysulfone | Transparent amber bowls for hot water | Handles heat and hydrolysis well |
Service tiers
Filter bowls and heads see pressure, threads, and O-ring grooves. Pick tier by fluid temperature and whether the sight window must stay clear.
| Tier | Environment | What matters most | Typical molded route | Quote path |
|---|---|---|---|---|
| 1 Low pressure indoor | HVAC-style filtration | Bowl stiffness and thread roots | PP or ABS bowl | Instant quote; field PP or ABS |
| 2 Clear bowl | Visual inspection of media | Stress in clear walls and gates | Clear PC or PET family | Instant quote; field PC; gate location review |
| 3 Warm wet service | Hot water or chemical rinse | Creep at threads and barbs | PP or PA-GF head | Instant quote; note temperature in comments |
| 4 O-ring groove head | Replaceable cartridge seal | Groove fill and roundness | PP or PA with O-ring groove in CAD | Upload CAD; include O-ring size in notes |
| 5 Pressurized line | Higher hold pressure | Weld lines at ports and creep | Glass-filled PA or PPS target | Full RFQ; attach pressure range qualitatively |
Materials
Housings are rigid thermoplastics. O-rings may be purchased separately; molded TPE seals use the TPE or TPV field.
| Family | Typical use on this part type | Notes for instant quote |
|---|---|---|
| PP | Opaque bowls and caps for water | Field PP; watch thread brittleness when cold |
| PC | Clear bowls and sight glasses | Field PC; check the fluid against the resin |
| PA (nylon) | Threads and stiff heads | Field Nylon; say if the head is glass filled |
| ABS | Indoor filter covers | Field ABS; general purpose housings |
| TPV | Molded-in gasket bead on lid | Field TPV; note compression groove in CAD |
Threads and seals
A molded thread is an undercut, and the way it releases from the mold drives tool cost and cycle.
External threads on a bowl can often be formed by splitting the cavity across the thread, which leaves a fine parting line along it. Internal threads on the head need a core that unscrews or collapses, or, for a shallow rounded thread in a flexible resin, a stripping action that pushes the part off. Unscrewing tools cost more but give a clean thread with no parting line.
The O-ring groove should sit where the tool forms it in one piece, away from the parting line. Flash or a step across a sealing face is a leak path. Axial seals, where the O-ring is squeezed between the bowl rim and the head, are more forgiving of thread wear than seals that depend on the thread pulling the parts tight.
A round bowl gated at the center of its bottom fills evenly with no weld line in the wall. A drain port or a hole in the bottom changes that, so its weld line has to be steered to a spot that does not carry pressure.
Threads
The bowl thread is almost always molded. The choice comes up on the head's pipe connections.
Avoid these
Two choices that show up after the first cartridges are changed.
Gating the bowl in the center and treating the weld line as solved. A center gate keeps a weld line out of the side wall, but a drain hole or a port in the bottom creates a new one. That line has to sit off the wall that holds pressure. Mark every hole on the drawing.
Using a tapered pipe thread on the plastic head with nothing to stop the wrench. The taper wedges outward as it tightens, and the stress grows with each extra turn. A straight thread with an O-ring face seal, plus a shoulder that stops the bowl, keeps the seal off that load.
Drawing
Send both halves, even if you only need one of them molded.
Head and bowl CAD, plus the cartridge that goes inside
Working pressure, peak pressure, and the fluid temperature
Whether the bowl must be clear, and why
Port connection type, and whether it is a tapered or straight thread
The O-ring size and compound you plan to use
Any drinking water or food contact listing the product needs
Keep reading
Threads, weld lines, and resins for pressurized housings.
Thread forms and how they release from the mold.
Molded in threadsWhere they form and how to move them.
Weld linesChoosing how the head takes a fitting.
Molded threads vs insertsA clear, stiff option for bowls.
SANTransparent and suited to hot water.
PolysulfoneThe opaque workhorse for water filtration.
PolypropyleneWhy a step on a sealing face leaks.
FlashThe other pressurized housing in the system.
Pump housingsEvery part-type guide, grouped by family.
Molded parts libraryFiltration and dosing equipment.
Water treatmentFAQ
Yes, if you send the cartridge or its drawing. The bowl length, the seal surfaces, and any center post are designed around the real cartridge.
Clear resins are prone to stress cracking when a chemical meets a stressed area. Common triggers are cleaning agents, thread lubricants, or O-ring grease that the resin does not tolerate, acting on the thread root or the gate. Check every chemical that touches the bowl.
Pressure and burst testing is normally run by your team on molded samples. DFM feedback before the tool is built shows where weld lines are expected, so the test can target the right spots.
No. There is no MOQ, and you own the tool.
Yes. The head is often a stiffer resin, such as glass-filled polypropylene or nylon, and the bowl is unfilled polypropylene or a clear resin when the cartridge has to be visible. The thread pitch has to match. Note the fluid temperature so both resins are chosen for the same service.
Give the bowl a shoulder or flange that meets the head before the thread bottoms. That stops the wrench from loading the thread without a limit. Put the maximum installation torque on the drawing so the test matches how the bowl will be tightened.
Next step
Upload both parts with the cartridge and pressure details. DFM feedback flags weld lines at threads and ports, and how each thread releases from the tool.