
Molded orifice
- One part, no insert to load
- The orifice is molded with the body
- Wears open where the liquid carries grit
Molded part guide: nozzles
A nozzle turns pressure into a pattern. Whether that pattern is a fine cone, a flat fan, or a straight jet is decided by a handful of features smaller than a grain of rice, and by whether they are exactly where the drawing says. A tiny shift in the opening sends the whole spray off to one side.
Small features
Spray nozzles, fan nozzles, misting nozzles, garden nozzles, and dispensing tips.
The opening is formed by a small pin meeting a matching seat when the tool closes. Where those two meet decides the opening size and whether it is centered. If the pin sits slightly off, the opening is no longer concentric with the passage behind it, and the spray leaves at an angle instead of straight ahead. A nozzle that sprays off to one side is almost always this.
Keeping the pin centered is a tooling problem. The pin is thin, it sticks out into the flow, and melt rushing past pushes it sideways. Supporting the pin at both ends, feeding the nozzle so the melt arrives evenly around it, and checking the first parts for concentricity rather than just opening size are the ways this is controlled.
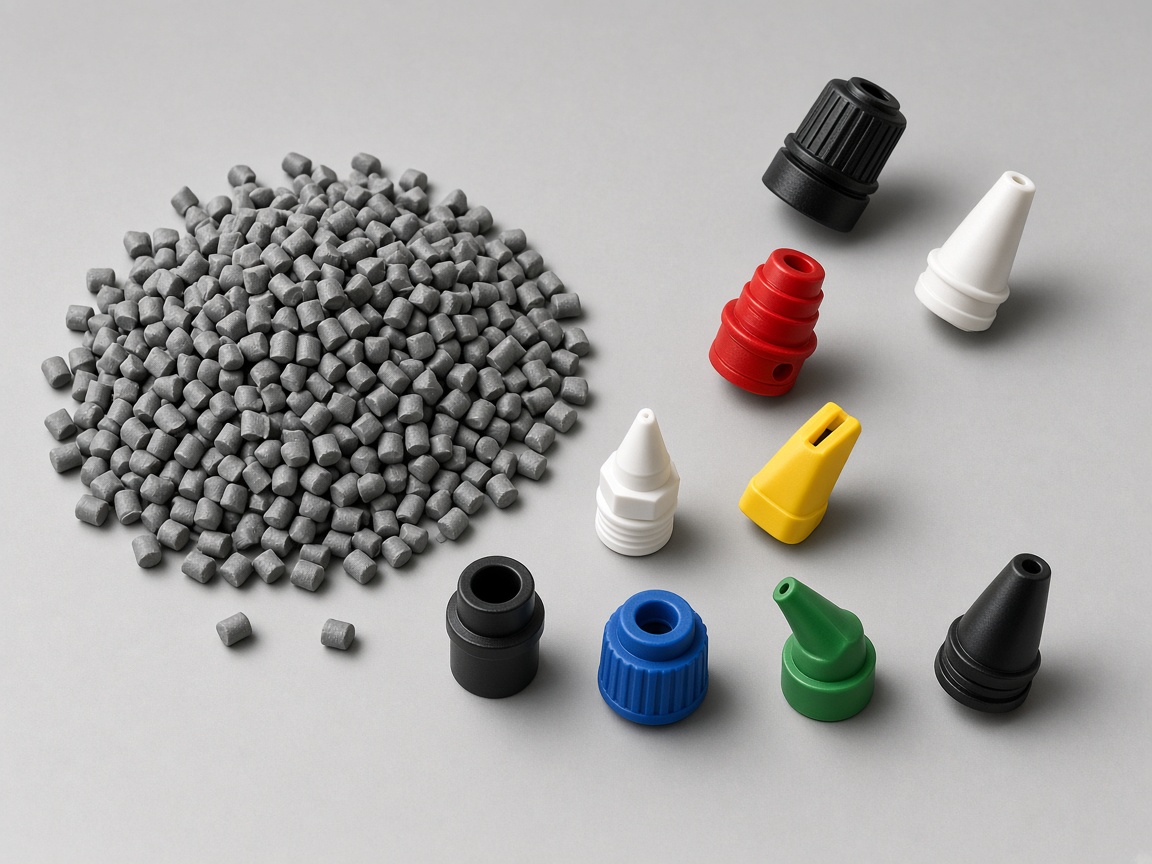
The pattern itself comes from what happens just before the opening. Slots or angled passages set the liquid spinning so it leaves as a hollow cone. A flat chamber across the opening spreads it into a fan. A straight passage gives a jet. Those features are small, so any flash across them changes the pattern, which is why the parting line is kept away from them.
Then there is wear. Water carries grit, cleaning chemicals attack, and every particle that passes through the opening takes a little material with it. As the opening wears it gets bigger and the pattern spreads, so the nozzle uses more liquid and covers less well. Where that matters, the opening is a hard metal insert molded into a plastic body.
Features
Every feature sits within a few millimeters of the tip.
| Feature | Purpose | Design note |
|---|---|---|
| Orifice | Sets flow and pattern size | Must stay centered with the passage behind it |
| Swirl features | Make a hollow cone | Slots or angled passages just behind the opening |
| Fan chamber | Makes a flat fan | Shallow chamber across the opening |
| Body passage | Feeds the tip | Smooth, with no sharp turn just before the opening |
| Thread or bayonet | Fits the wand or the line | Sealed by a gasket or by a tapered thread |
Service tiers
Part focus: Orifice concentricity, swirl features, wear inserts. Upload CAD with critical fits and environment in notes when not modeled.
| Tier | Environment | What matters most | Typical molded route | Quote path |
|---|---|---|---|---|
| 1 Centered orifice | The spray has to leave straight | The pin stays concentric with the passage | Supported at both ends | Upload CAD; name the pattern |
| 2 Cone or fan | A hollow cone or a flat fan | Slots, angled passages, or a shallow chamber | Parting line kept off those features | Instant quote; name cone, fan, or jet |
| 3 Straight jet | A straight passage to the tip | No sharp turn just before the opening | Same body | Upload CAD; say it is a jet |
| 4 Grit in the liquid | The opening has to keep its size | Wear makes the opening larger | Metal insert in a plastic body | Instant quote; name the grit |
| 5 Attachment | Thread or bayonet on the wand | Sealed by a gasket or a tapered thread | Same body | Upload CAD; note the connection |
Materials
One primary family per line item. Put commercial grade, fillers, and environment filters in comments.
| Family | Typical use on this part type | Notes for instant quote |
|---|---|---|
| Filled nylon | Nozzle body | Field the filled grade; name the grit and the cleaner |
| POM (acetal) | Nozzle body | Field POM; name the grit and the cleaner |
Concentricity
The pin that forms the opening is thin, and melt pushes it around.
Orifice
How long the pattern has to stay the same decides this.
Avoid these
Two choices that send the spray sideways or change the pattern.
Supporting the orifice pin at one end only. Melt rushing past pushes the thin pin off center, so the opening is no longer concentric with the passage and the spray leaves at an angle. Support the pin at both ends, and feed the melt evenly around it.
Putting the parting line across the swirl slots or the fan chamber. Flash there changes the pattern. Keep the parting line away from those features.
Drawing
The pattern and the liquid set everything else.
Nozzle CAD, or the pattern and flow you need
Working pressure at the nozzle
Liquid type, and anything abrasive in it
How the nozzle attaches, thread or bayonet
Expected service life before the pattern shifts
Expected annual volume
Keep reading
Other fluid parts, small openings, and the flash that spoils them.
Barbs, threads, and sunlight.
Irrigation fittingsCored passages and seal seats.
Valve bodiesCones, stems, and air channels.
FunnelsThin tips and clean openings.
Pipette tipsThin films across small features.
FlashMetal orifices in plastic bodies.
Insert moldingWhen small features need control.
Tight tolerancesHow we support industrial programs.
Industrial and transportationEvery part-type guide, grouped by family.
Molded parts libraryHose nozzles and sprinklers.
Lawn and gardenFAQ
The opening is not concentric with the passage behind it, usually because the pin that forms it moved. Supporting the pin at both ends and feeding evenly around it brings the spray straight. Spraying onto a marked card at a fixed distance makes a sideways pattern obvious in seconds.
Small differences in the opening and in the swirl features are enough. Checking concentricity as well as opening size on the first parts shows which one is moving. Keeping the parting line away from the swirl features means flash never lands where it would change the pattern.
Grit in the liquid slowly wears the opening open. A metal insert orifice holds its size where the liquid is abrasive.
Acetal and filled nylon are common for their stiffness and wear. Where strong cleaning chemicals are used, a more resistant grade is worth checking against that specific chemical. A grade that shrugs off the chemical but wears quickly is no better than the reverse, so both are checked together.
Slots or angled passages just behind the opening set the liquid spinning, and it leaves as a hollow cone. A shallow chamber across the opening spreads a flat fan. A straight passage gives a jet.
When the liquid carries grit. Wear opens a plastic orifice, the pattern spreads, and the nozzle uses more liquid. The hard metal insert is molded into the plastic body.
Next step
Upload the nozzle, or describe the pattern and pressure. DFM feedback covers orifice concentricity, swirl features, flash risk, and insert options.