
Tandem molds
Two levels that fill in turn, not together.
Tandem moldsProcess guide
When a plant needs more caps or lids per cycle and the platen is already full, the next step is not always a bigger press. A stack mold builds upward instead, putting another set of cavities behind the first.
The layout
The trick is that the injection pressure on the two faces pushes in opposite directions.
A stack mold has parting lines that fill together. Tandem molds let one level cool while the other ejects. Thin wall molding is a common reason to stack lids and containers. Parting line placement still decides the flash. A hot runner carries melt into the center block.
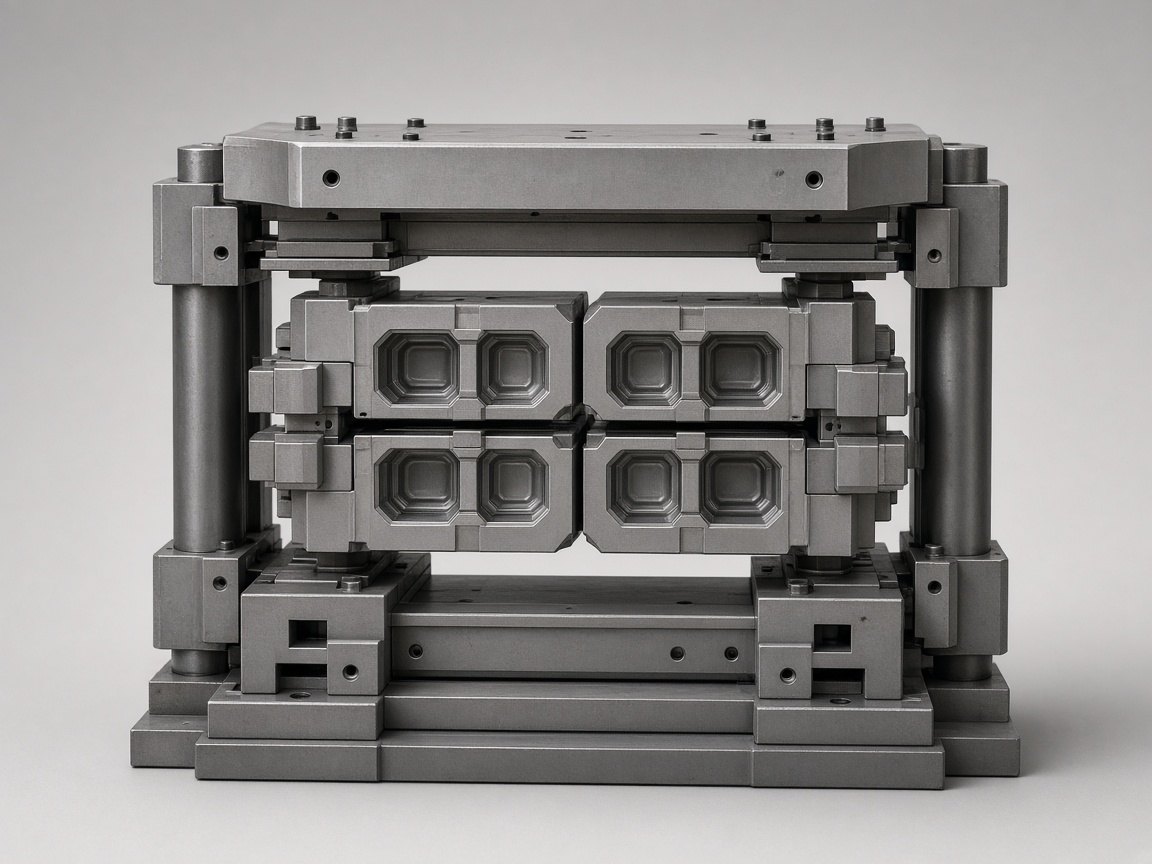
A normal mold has one parting line between the fixed half and the moving half. A stack mold adds a floating center section between them, with cavities or cores on both of its faces, so there are parting lines on each side of it. When the mold closes, both sets of cavities fill in the same shot.
Clamp force is set by the projected area of the parts on one parting line, and the pressure on the two faces of the center block balances out. So the clamp needs only a little more force than for a single level of the same parts. What the press needs more of is opening stroke, shot size, and room between the tie bars and platens for a much thicker mold.
Roles
A stack fills every parting line together. A tandem alternates. Thin wall design covers the part.
| Page | Use it for |
|---|---|
| Stack molds (this page) | Parting lines that fill in one shot |
| Tandem molds | Levels that take turns |
| Thin wall molding | The fill race on a thin part |
| Parting line | Where the mold splits |
| Hot runner | Melt path into the center block |
Inside the tool
Each one solves a problem the extra parting line creates.
The nozzle cannot reach the center block directly, so a heated bar carries melt through the fixed half into the center. It has to separate cleanly every time the mold opens.
The center section carries a manifold that feeds both faces. Cold runners are rare, because there is nowhere to eject them from the middle of the tool.
Racks and pinions, toggle links, or cylinders make both parting lines open by the same amount at the same time, so parts on each face have room to eject.
The heavy center section rides on the tie bars or on its own carriage. Without support it sags, and the parting lines stop meeting squarely.
Press fit
A stack mold can be right for the part and wrong for every press in the building.

Fit
Shallow, flat, high volume parts are the natural candidates.
| Part trait | Why it matters |
|---|---|
| Shallow depth | Deep parts need long opening strokes on each level, which most presses cannot supply |
| Large flat area | Area is what drives clamp force, so this is where stacking saves the most press |
| Short cycle | Lids, caps, and thin wall containers already run fast, and stacking multiplies that output |
| Stable, long running design | A stack is costly to change; it pays back over long runs of an unchanging part |
| Side actions and slides | Possible, but crowded; heavy side action work is usually a sign to stay single level |
Keep reading
The alternating variant, the runner system that feeds a stack, and the parts that usually justify one.
Two levels that fill in turn, not together.
Tandem moldsWhy stacks almost always run hot.
Hot runner vs cold runnerCavity economics on one parting line.
Single vs multi cavity costThe fast cycle parts stacks are built for.
Thin wall moldingCaps, hinges, and dispensing tops.
ClosuresFlat parts with snap beads.
LidsHow press size is described.
TonnageEvery molding process and secondary operation.
All processesFAQ
The melt pressure on each face of the center block pushes in opposite directions and largely cancels out. The clamp resists the projected area of one level, plus a margin, not the sum of all levels.
Yes. Multi level stacks exist for very high volume flat parts. Each level adds mold height, stroke, and complexity, so they are rare outside packaging.
It can, as long as the parts fill and cool on a similar timeline. Lids on one face and matching bases on the other is a known layout.
It has more moving parts: the linkage, the sprue bar, and a hot runner inside a moving block. Maintenance is more involved than on a single level tool, and downtime stops every level at once.
Stack fills every parting line in one shot. Tandem lets one level cool while the other ejects.
No. Cavitation is set on the program.
Next step
Upload CAD for DFM review and an instant quote on the injection molded part.