
Stack molds
Levels that fill together.
Stack moldsProcess guide
On a thick part, most of the cycle is spent waiting for it to cool, and the press injection unit sits idle. A tandem mold keeps it busy by filling a second level while the first one is still cooling.
The idea
The hardware looks similar. The sequence is what makes it a tandem.
A tandem mold has two levels that fill in turn. Stack molds fill both parting lines in the same shot. Family molding puts different parts in one shot. The family tooling article compares that with separate tools. A hot runner switches melt from one tandem level to the other.
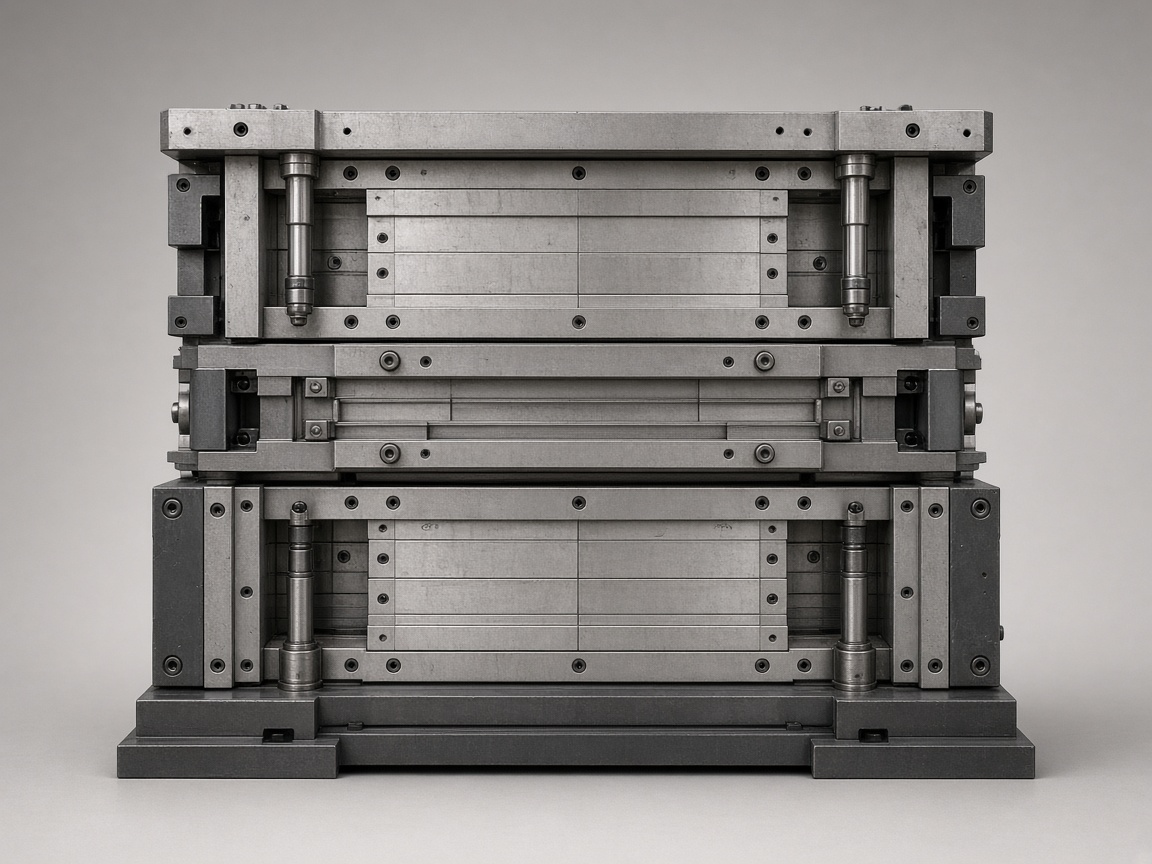
A tandem mold has two parting lines on either side of a center section, like a stack mold. The difference is that the levels never fill together. The press injects into one level, and while that level holds and cools, the other level opens, ejects, closes, and waits for its own shot.
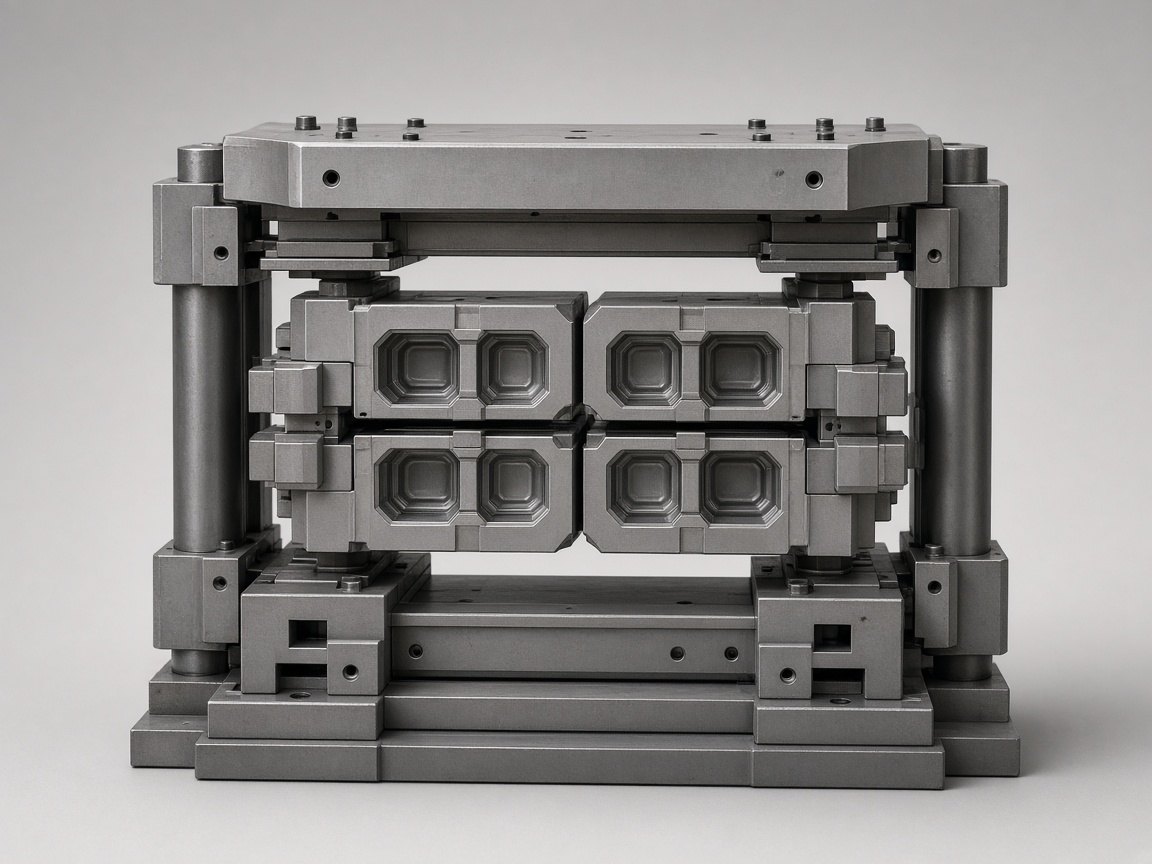
Latches lock whichever level is cooling, so the press can open the other. A hot runner with valve gates switches the melt from one level to the other. The clamp only ever resists one level's injection pressure, and the injection unit, which would sit idle through a long cooling time in a normal mold, works for most of the cycle.
Roles
Tandem fills one level at a time. A stack fills both levels together. A family mold puts different parts in one shot.
| Page | Use it for |
|---|---|
| Tandem molds (this page) | One level fills while the other ejects |
| Stack molds | Both parting lines fill in one shot |
| Family molding | Different parts in one shot |
| Family tooling article | Family tool versus separate tools |
| Hot runner | How melt is switched between levels |
Sequence
Level A and level B swap roles every time the press opens.
Valve gates open to level A only. Level B is closed and its parts are still cooling from the previous shot.
A latches shut to hold level A closed. The press opens and only level B parts, now cool, are ejected.
The press closes, the valves switch, and level B takes its shot while level A keeps cooling.
The latches swap. Level A opens and ejects, and the cycle repeats from the start.
Three layouts
All three put more than one part in a cycle. They solve different problems.
| Point | Tandem mold | Stack mold | Family mold |
|---|---|---|---|
| When levels fill | In turn | Together | One level; all cavities together |
| Best suited to | Long cooling times | Short cycles and flat parts | Sets of related parts at moderate volume |
| Different parts in one tool | Easy, since each level has its own shot and timing | Only if they fill and cool alike | Yes, if volumes and sizes are close enough to balance |
| Clamp force | One level at a time | About one level, since faces oppose | All cavities on one face |
| Tool complexity | Highest: latches, valve gates, sequencing | High: linkage, sprue bar, center manifold | Close to a standard mold |
Where it helps
A family mold fills every cavity in one shot, so a big thick part and a small thin one fight over pressure and cooling time. Tandem levels do not share a shot.

Caveats
The idea is simple. Running one well is not.
The press controller has to sequence latches, valve gates, and ejection for each level
A latch that fails to hold can open a level with hot parts inside
Each level is ejected every other opening, so part handling has to follow the alternation
Few mold makers and molders run them, so support and second sources are limited
The gain only exists when cooling is long compared with the rest of the cycle
Keep reading
Other layouts for more than one part per cycle, and where cycle time goes.
Levels that fill together.
Stack moldsRelated parts in one single level tool.
Family injection moldingWhy cooling usually takes the most time.
Cycle timeManifolds and valve gates.
Hot runner moldingWhat holds the mold shut during a shot.
Clamping forceHousings and covers made as matched sets.
EnclosuresEvery molding process and secondary operation.
All processesFAQ
It is often described that way, since the hardware is similar. The alternating fill is what sets it apart, and that changes the controls, the runner, and which parts suit it.
It needs enough mold height and stroke for a two level tool, and a controller that can handle the extra sequencing. Many presses need added control outputs rather than a different machine.
That is often the simpler answer. A tandem mold makes sense when press capacity or floor space is the limit, not when there are free presses available.
In most tandem molds, yes, because both levels are fed by the same injection unit. Color and resin are shared across the tool.
A stack fills both levels in the same shot. A tandem fills one level while the other cools and ejects.
Upload CAD for DFM and an instant quote.
Next step
Upload CAD for DFM review and an instant quote on the injection molded part.