
Shift during fill
The insert must stay put under melt pressure. Call out location and count.
Molded-in inserts
The insert must survive fill without shifting. Plan knurl or undercut retention and mold shutoff. DFM review comments on CAD before quoting.
Design guideline
A molded-in insert is loaded in the cavity and the plastic locks around it during fill. Retention and shutoff must be planned before steel is cut.
Location must survive fill without shifting. Retention knurls or undercuts hold the insert after demold. Insert molding is the capability when metal is in the shot. DFM review needs insert type, count, and tolerances on CAD.
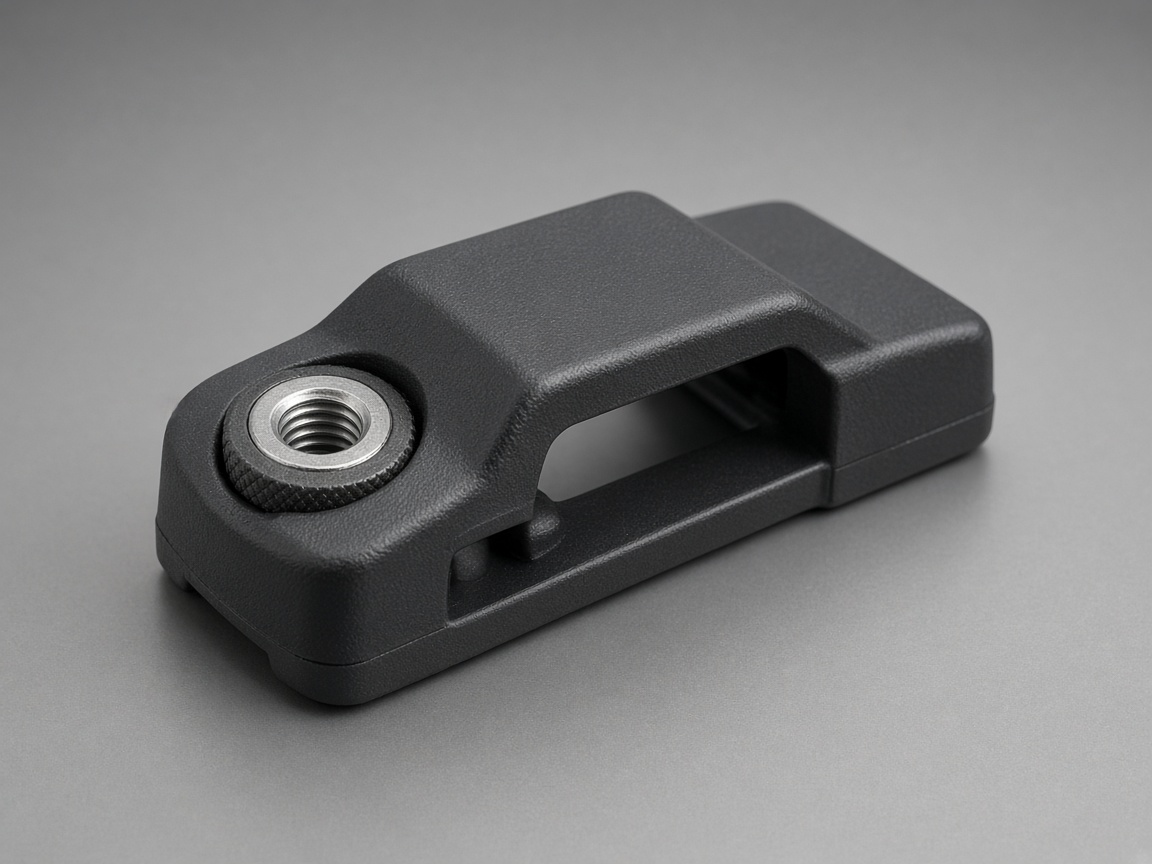
This spoke owns in-cavity inserts. Post-mold inserts go in after the shot. Insert retention owns pull-out. Bosses own the post. The design guide hub lists every topic.
Roles
Stay here for inserts loaded during fill. Open a sibling for after-the-shot or the post.
| Page | Use it for |
|---|---|
| Molded-in inserts (this page) | Metal in the cavity during fill |
| Post-mold inserts | Heat-set or press-in after the shot |
| Insert molding | The capability page |
| Insert retention | How the insert stays put |
| Boss design | The plastic around the insert |
| Self-tapping screw bosses | Skip metal when a screw can cut plastic |
| Molded-in threads | Plastic threads instead of an insert |
| Wall thickness | Nominal wall around the insert boss |
| DFM review | CAD check before steel |
Checks
Qualitative checks. No figure on this page is a NetProto specification.
Shift during fill
The insert must stay put under melt pressure. Call out location and count.
Retention geometry
Knurl or undercut holds after demold. The retention page owns pull-out.
Shutoff on metal
Cavity steel must seal around the insert. Plan witness on cosmetics.
Warp and pack
Metal and plastic cool differently. Mark critical fits near inserts.
Decision
Wrong: add inserts after T1 with no steel plan. Right: pick in-cavity or after-the-shot before the tool is cut.
RFQ
The quote can start from CAD alone. These notes make the DFM pass specific.
Insert type, material, and count
Who supplies the inserts
Retention feature: knurl, undercut, or hex
Location and position tolerance
Cosmetic faces near insert shutoff
Fits that cannot warp around the insert
Related
Stay on this spoke for its question. Open a sibling for the neighbor topic or the CAD check.
Capability page for metal in the shot.
Insert moldingHow NetProto checks insert programs before steel.
DFM reviewFAQ
It is metal loaded in the cavity so plastic locks around it during fill. Retention and shutoff must be in the tool plan.
Say on the RFQ. Programs quote when insert type, count, and tolerances are defined on CAD. Do not leave supply as an assumption.
A late add usually needs steel work. Decide in-cavity versus post-mold before the tool is cut.
Yes. Metal and plastic cool at different rates. Mark critical fits near inserts and keep walls even around the boss.
Insert molding puts metal in the shot. Post-mold install happens after. This page owns the in-cavity path.
Bosses own the plastic post. Retention owns pull-out. This spoke owns loading metal during fill. DFM review checks CAD.
Next step
Share insert type, count, location, and who supplies the metal so review can check retention, shutoff, and warp before quoting.