Skip to content
NetProto

Molded part guide: spur gears

Injection Molded Spur Gears

A spur gear looks simple because the teeth are straight. In molding, straight teeth still shrink unevenly in the plane of the gear, and a small pinion still needs profile shift before the steel is cut.

Straight teeth

Spur is the default, and the first place shrink shows up

Most molded gear trains start with spur pairs because the tool can pull straight along the bore.

A spur gear ejects like any round part: the mold opens, the part stays on the core or the cavity, and it comes off in a straight line. That is why spur pairs dominate printers, meters, small actuators, and appliance drives. The tooth form still has to be corrected for plastic shrink, which is not the same as scaling the whole disk evenly.

Involute teeth shrink differently along the flow than across it. If the cavity is cut from a metal gear drawing with only a single shrink percentage, the molded teeth often come out too thin at the tips and too heavy at the roots, and the effective pressure angle climbs. Mesh feels tight, noise goes up, and wear concentrates at the tips.

Tooling practice is to enlarge the cavity module using the resin shrink rate, then inspect sample gears and adjust the tooth profile before the production cavity is finalized. Send the gear data listed below with your CAD so DFM review starts from numbers, not guesses.

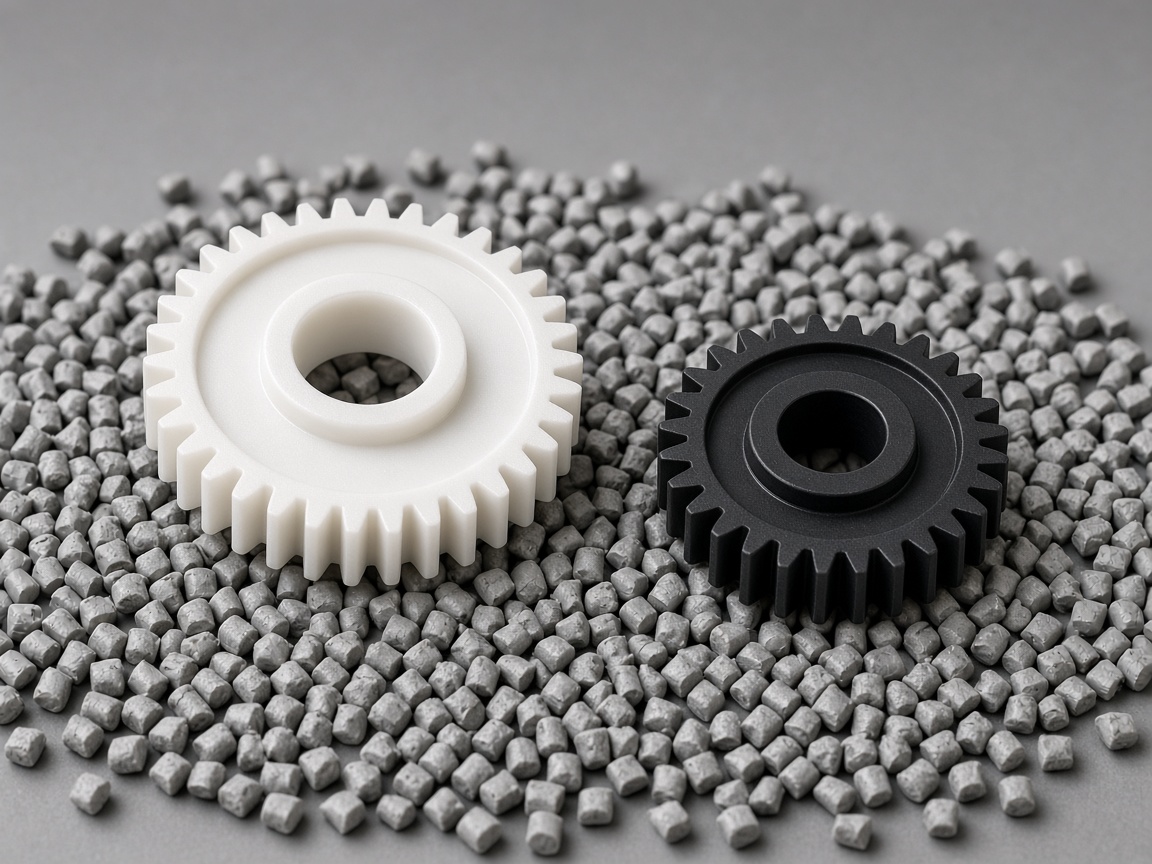
A white and a black molded spur gear on a bed of gray resin pellets

Geometry

Parameters that change before the mold is cut

Typical design levers on spur pinions. Final values come from your load, center distance, and resin.

ParameterWhy it matters in moldingCommon adjustment
Tooth count on the pinionVery small pinions risk undercut at standard pressure anglePositive profile shift, or a higher pressure angle
Module or diametral pitchSets tooth size and how much plastic sits between teethSmaller module fills faster but leaves less material at the root
Pressure angleSteeper angles resist undercut but are less forgiving of center distance errorA commonly used pressure angle is the usual starting point on plastic pairs
Profile shiftMoves material from tip to root without changing the ratioPositive shift on the pinion is the usual fix for undercut
Tooth form standardRoot fillet and tip relief change bending stress and contactModified forms with full fillet roots are common on molded plastic gears

Service tiers

Spur gear service tiers and quote path

Motion part focus: Straight teeth: profile shift, shrink-corrected cavities, and gating. Upload CAD with module, pressure angle, and tooth count in notes when the model does not show them.

TierEnvironmentWhat matters mostTypical molded routeQuote path
1 Module prototypeFirst article spur pairProfile shift and shrinkPOM spur on hubInstant quote; field POM
2 Enclosed gearboxLubricated or greased boxWear and heat from frictionPA or PBT spurInstant quote; note lube type in comments
3 Small pinionFew teeth on a small pinionFill and vent at rootPOM high flow family in notesUpload CAD; expect thin tooth DFM
4 Wide face widthWide face on a spur pairHub stiffness and warpGF PA hub with POM teeth if splitFull RFQ if split materials
5 Quiet runningNoise-sensitive driveTooth profile and concentricityStable POM; gate off pitch lineUpload CAD; note noise goal qualitatively

Materials

Resin families: quick reference for quote notes

Pick one primary family per molded part line. Put commercial grade or wear filters in comments.

FamilyTypical use on this part typeNotes for instant quote
POM (acetal)Precision gears and low frictionField POM; note moisture if long service
PA (nylon)Loaded gears and wear resistanceField Nylon; note GF for stiffness
PPLow-load gears and cost-sensitive drivesField PP; watch creep under load
PC/ABSHousings with integrated gear featuresField PC/ABS; separate line if distinct part
PBTGears near moderate heat and humidityField PBT; note glass fill in comments

Gating

Keep the gate off the working flank

The gate location sets flow direction, roundness, and where the weld line lands.

  • Gate into the hub, a thick web, or the parting line land, not into a tooth flank that mates
  • Glass-filled grades need balanced fill so the bore and pitch diameter stay round
  • Vent the tooth tips on deep gears so air does not trap between teeth
  • Measure runout and tooth spacing on molded samples, not only on the CAD model
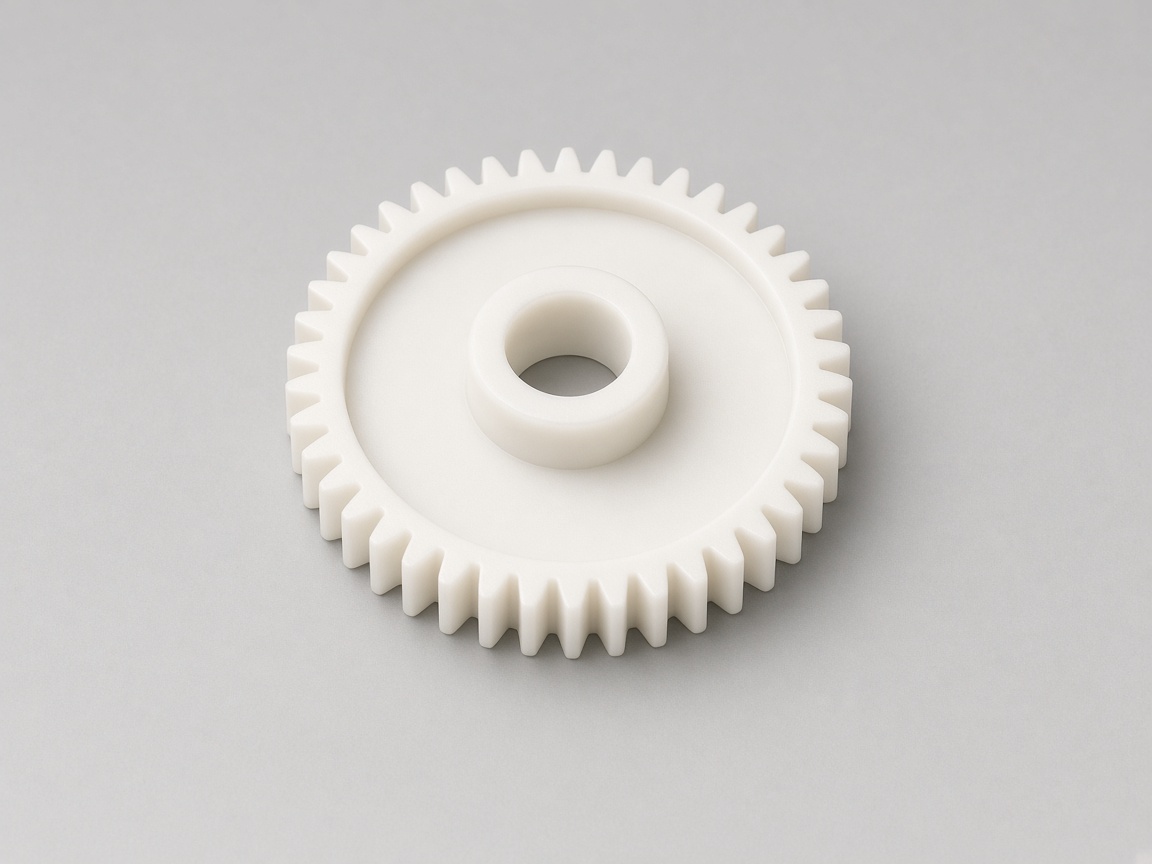
An off-white molded spur gear showing the hub, the web, and straight teeth

Validation

Why mesh tests on a stand-in gear do not carry over

The tooth form of a molded spur gear belongs to the cavity it came from.

Prototype gears from another process

  • Tooth profile comes from a different process, or from a cavity with its own shrink correction
  • Noise, backlash, and wear results describe that part, not the production gear
  • The production tool still has to be sampled and the mesh proven a second time

First gears from the production steel

  • The profile you measure is the one cut into the tool you keep
  • Corrections to the tooth form happen once, on the tool that runs production
  • The hardened steel tool is completed in 10 business days on qualified programs

Avoid these

Common design mistakes on molded spur gears

Two choices that are hard to undo after the steel is cut.

Cutting the cavity from the gear drawing with only one shrink percentage. Involute teeth shrink differently along the flow than across it. Tips then come out thin, roots come out heavy, and the effective pressure angle climbs.

Gating into a tooth flank that meshes with the mate. Put the gate in the hub, a thick web, or the parting line land. The working flank should not carry the vestige.

Drawing

Gear data to send with spur gear CAD

A STEP file alone rarely carries the tooth specification the mold needs.

  • Module or diametral pitch, tooth count, pressure angle, and profile shift on each gear

  • Center distance and backlash target in the assembly

  • Mating gear material, whether metal or plastic

  • Resin grade and any glass fill

  • Accuracy class or inspection method you plan to use on samples

  • Hub features molded in the same shot: bore, key, cam, or snap features

Keep reading

Related guides

Parent gear topics and supporting design rules.

Molded gears

Resin pairing, general gating, and gear train context.

Molded gears

Worm gears

Helical teeth and rotational demolding.

Worm gears

Warpage

When a thin web warps and opens backlash.

Warpage

FAQ

Questions about molded spur gears

Can you mold a spur gear and a metal gear as a pair?

Yes. Pinion in plastic and gear in metal is common. Send both parts so center distance and backlash are checked against the actual metal tooth form, not a generic catalog.

Do you cut the cavity with hobbing equipment?

Cavity details depend on the shop process. What matters for you is that the involute profile is shrink corrected for your resin and verified on molded samples before production release.

Our pinion has very few teeth. Can it still be molded?

Often yes, with profile shift or a steeper pressure angle. DFM review flags undercut risk and suggests geometry changes before tooling is cut.

Can the hub include a metal insert in the same shot?

Yes, when the insert suits the resin and the tool can load it each cycle. Send the insert drawing with the gear CAD.

Is there a minimum tooth count before a molded spur pinion undercuts?

There is no single tooth count. It depends on the pressure angle and any profile shift. Very small pinions at a standard pressure angle are the ones to check. Positive profile shift is the usual fix, and it belongs on the drawing before the steel is cut.

How do I know if the pinion needs profile shift?

When the tooth count is low enough that a standard pressure angle would undercut the root, or when a fixed center distance does not fit the standard tooth form. Put tooth count, pressure angle, and any shift on the drawing. DFM review flags undercut risk before tooling is cut.

Next step

Quote the spur gear with its gear data

Upload CAD plus module, tooth count, pressure angle, and mating gear details. DFM feedback covers undercut, gate location, and shrink correction.