
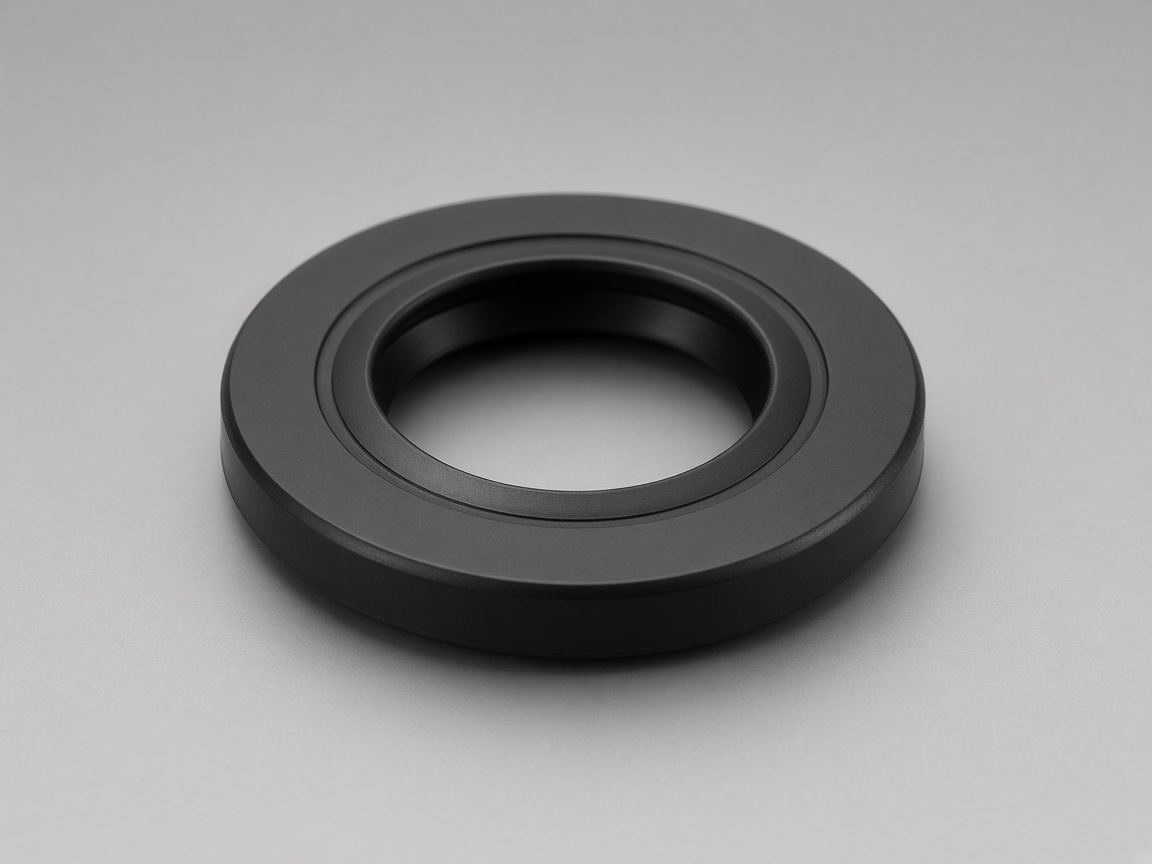
Molded lip
- No separate ring to buy or assemble
- Lip shape tuned to the pressure and direction
- Sealing force depends on the molded shape staying true
Molded part guide: seals
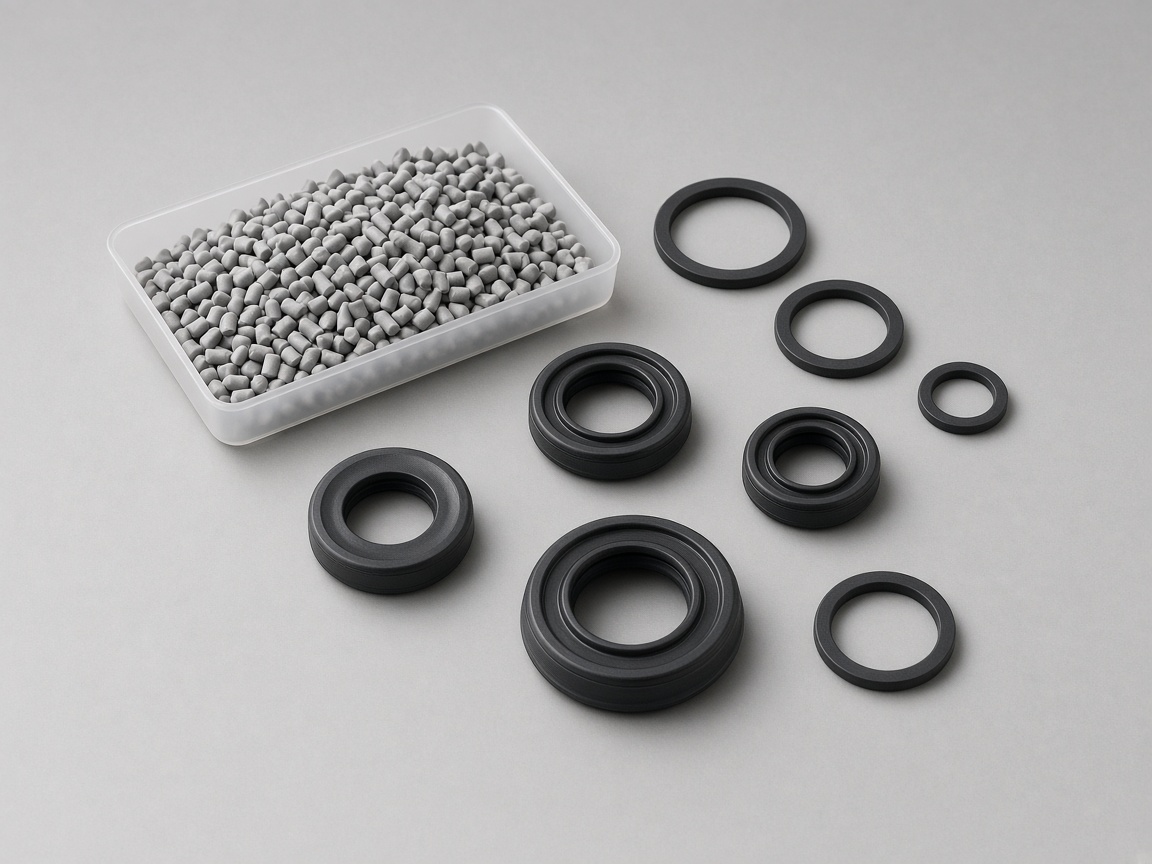
A seal that works against a moving surface has a harder job than a gasket. It has to press hard enough to keep fluid in, and lightly enough that it does not drag, heat up, and wear away the very surface it is sealing against. Those two demands are in direct conflict, and the lip is where they meet.
Interference
Lip seals, wiper seals, plunger seals, sealing beads, and O-ring grooves in molded parts.
A lip seal is a thin flexible edge that sits slightly inside the shaft it surrounds, so it has to stretch onto it. That interference is what holds the lip against the surface, and how much of it there is decides everything else. More interference seals better against pressure and against surface imperfections. Less interference drags less, runs cooler, and lasts longer.
Friction is not just an efficiency question. A lip running dry heats up, and a warm lip loses stiffness, so it presses less and seals worse while wearing faster. Low friction materials such as acetal and lubricated grades, a smooth counter surface, and the film of fluid the seal is holding back all keep the lip cool enough to keep working.
The counter surface matters as much as the seal. A shaft that is too rough tears the lip. A shaft that is polished mirror smooth can be worse, because it gives the lip nothing to hold a lubricating film in, so it runs dry. A moderate finish with fine marks running around the shaft rather than along it is what seals best.
Many molded parts do not carry a seal at all, they carry a groove for one. That groove is a precision feature: its depth sets how much the O-ring is squeezed, its width gives the ring somewhere to move, and its corners keep the ring from being pinched or rolled during assembly. A lead-in taper into the bore stops the ring being cut as the parts come together.
Features
Interference, finish, and groove geometry are the three levers.
| Feature | Purpose | Design note |
|---|---|---|
| Lip interference | Holds the lip on the surface | Traded off between sealing and wear |
| Lip section | Lets the lip follow the surface | Thin and flexible, with a clean edge |
| Counter surface finish | Keeps a lubricating film | Neither rough nor mirror smooth |
| O-ring groove depth | Sets the squeeze on the ring | Sized so the ring is never squashed solid |
| Lead-in taper | Protects the ring on assembly | Stops the ring being cut or rolled |
Service tiers
Pick the tier that matches your part in service, then use the quote path column when you upload CAD. Tiers describe molded TPE, TPU, or TPV seals unless notes call for LSR review on the RFQ.
| Tier | Environment | What matters most | Typical molded route | Quote path |
|---|---|---|---|---|
| 1 Indoor / low pressure | Dry housings, cable entries, static joints | Compression set and groove fill | TPE or TPV in the groove or as a lip | Instant quote; material field TPE or TPV |
| 2 Outdoor / weather | UV, ozone, rain, seasonal temperature swing | Elasticity after aging | UV-stable TPV or outdoor TPE grades | Instant quote; note exposure in comments |
| 3 Fluids (intermittent) | Oil, fuel, or water splash in service | Swelling and compression set | TPV or TPU; commercial grade TBD on TDS | Instant quote; name fluid in notes |
| 4 High heat or aggressive media | Continuous hot or chemical contact | Material survival before geometry tuning | Often needs supplier grade review | Full RFQ; attach target TDS when known |
| 5 Lip or sliding contact | Shaft, bore, or dynamic lip | Interference vs wear and ejection | Molded lip in TPV or TPE | Upload CAD; expect DFM on lip and draft |
Materials
Drawings often name thermoset rubbers such as NBR or FKM. NetProto quotes injection molded seals in TPE, TPU, TPV, and LSR when the program is scoped on the RFQ. Name the fluid and whether you need a lip or a groove.
| Material | Notes for instant quote | On this part |
|---|---|---|
| TPE | Field TPE; name the fluid | Static joints and lips |
| TPU | Field TPU; name the fluid | Intermittent fluid contact |
| TPV | Field TPV; note weather if it sits outside | Outdoor seals and molded lips |
| LSR | Only when the RFQ scopes it | Not the default lip |
Friction
Interference buys sealing and costs friction, heat, and wear.
Sealing method
One part with a lip, or a simple part carrying a standard ring.
Avoid these
Two choices that make a lip seal at first and leak after it warms up.
Adding interference until the leak stops, and leaving it there. More interference holds the lip on the shaft, and it also drags and heats. A warm lip loses stiffness, presses less, and wears faster.
Polishing the shaft to a mirror finish. A rough shaft tears the lip. A mirror finish gives the lip nothing to hold a fluid film, so it runs dry. Use a moderate finish with fine marks running around the shaft, not along it.
Drawing
The moving surface and the fluid decide almost everything.
Seal and housing CAD with the groove or lip shown
Shaft or bore size and its surface finish
Pressure, speed, and direction of motion
Fluid, temperature, and lubrication available
Service life and whether the seal is replaceable
Expected annual volume
Keep reading
Gaskets, bearings, and the wear resins that run against metal.
Static face sealing and groove fill.
GasketsPlain bearings running on a shaft.
BushingsSealed pass-through parts.
GrommetsSeal seats inside a body.
Valve bodiesLow friction against metal.
Acetal (POM)Choosing a running surface.
Acetal vs nylon for wearWhen the groove has to be exact.
Tight tolerancesHow we support industrial programs.
Industrial and transportationEvery part-type guide, grouped by family.
Molded parts libraryFAQ
Usually the lip wore quickly because the interference was too high, or the counter surface was too rough. Easing the interference and correcting the shaft finish are the first two things to try. Running early seals on the real shaft finish, rather than on a polished test bar, gives a far more useful result.
Yes. A mirror finish leaves nothing to hold a lubricating film, so the lip runs dry and wears. A moderate finish with marks running around the shaft seals best.
Deep enough that the ring is squeezed but never squashed solid, and wide enough that it has room to move. The exact numbers come from the ring size and the pressure, and we check them against your ring.
A molded lip removes a part from the assembly and can be tuned to the pressure. A standard O-ring in a groove is easier to replace and lets the seal material be chosen on its own.
Friction heats a dry lip. The lip loses stiffness, presses less, and wears faster. Less interference, a low-friction grade, and a counter surface that holds a fluid film are what keep it cool.
A lead-in taper into the bore. Groove corners should not pinch or roll the ring. The depth still has to squeeze the ring without squashing it solid. Send the ring so the groove can be checked against it.
Next step
Upload the seal or the housing with its groove. DFM feedback covers lip interference, friction, groove geometry, and resin choice.