
Separate gasket
- Replaceable during service
- Material chosen freely, and changed without tool work
- Can be misplaced, stretched, or fitted crooked
Molded part guide: gaskets
A gasket seals because it is squashed. It keeps sealing because it keeps pushing back. Every molded gasket eventually stops pushing back as hard as it did on the first day, and how quickly that happens decides whether the joint still holds. The rest is geometry.
Squeeze
Enclosure gaskets, cover gaskets, face seals, and overmolded seal beads.
Clamping two faces onto a gasket squashes it, and the squashed material pushes outward against both faces, filling every small irregularity in them. That outward push is the seal. As long as the material keeps pushing hard enough to follow the surfaces, the joint stays closed. When the push fades below what the surfaces need, the joint leaks, even though nothing looks different.
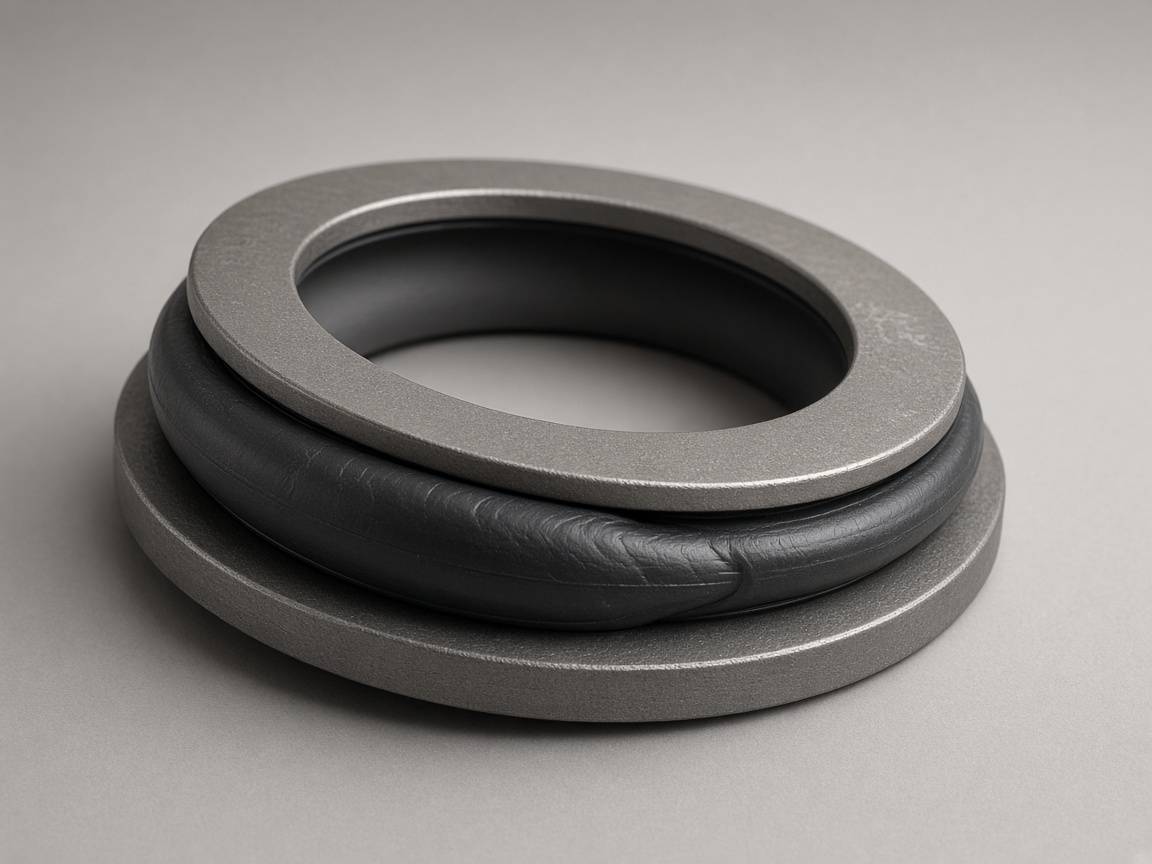
The fading is called compression set: the fraction of the squeeze that the material never recovers. Thermoplastic elastomers take a permanent set faster than the silicone and rubber compounds used for demanding static seals, and heat speeds it up a great deal. A gasket that is fine at room temperature can lose most of its push after a summer in a hot cabinet.
Geometry decides how much squeeze there is to lose. The gasket sits in a groove, and the groove needs to be deep enough that the gasket is not squashed solid, and wide enough that the material has somewhere to bulge. A groove filled too full leaves the gasket nowhere to go, so the clamping load goes into forcing the plastic apart instead of into sealing.
There is also a choice about where the gasket lives. It can be a separate molded part dropped into a groove at assembly, or a bead of soft material overmolded directly onto the housing. The overmolded bead cannot be lost, misplaced, or fitted crooked, which removes the most common assembly errors, but it ties the seal to the part.
Features
Groove and gasket are designed as one thing.
| Feature | Purpose | Design note |
|---|---|---|
| Gasket section | Provides the squeeze | Sized so it is never squashed solid |
| Groove depth | Sets the squeeze | Leaves the gasket room to recover |
| Groove width | Gives the material somewhere to go | Never filled completely by the gasket |
| Corners | Where gaskets usually leak | Generous, with even section round the turn |
| Clamping points | Apply the load | Spaced so the squeeze is even along the joint |
Service tiers
Tiers describe molded gasket compression and environment. Upload CAD with groove width, depth, and mate surface finish in notes when available.
| Tier | Environment | What matters most | Typical molded route | Quote path |
|---|---|---|---|---|
| 1 Static indoor | Enclosure lids that stay closed | Compression set and groove fill | TPE or TPV cord or ring | Instant quote; field TPE or TPV |
| 2 Outdoor service | UV and rain on the seal line | Aging and elastic recovery | UV-stable TPV | Instant quote; note outdoor exposure |
| 3 Fluid splash | Oil, coolant, or detergent nearby | Swelling and stress relaxation | TPV family; grade on TDS | Instant quote; name fluid in comments |
| 4 Overmolded bead | Seal bonded to rigid cover | Bond line and bead size | 2K TPE on ABS or PC/ABS | Upload CAD; note substrate in comments |
| 5 High temperature | Hot air or steam nearby | Softening and permanent set | Heat-rated family TBD | Full RFQ; attach temperature range |
Materials
Molded gaskets are thermoplastic elastomers, not sheet die-cut rubber. Put target media and hardness in notes.
| Family | Typical use on this part type | Notes for instant quote |
|---|---|---|
| TPE | Soft gasket lips and beads | Field TPE; name the fluid |
| TPV (Santoprene) | Compression gaskets and seals | Field TPV; note the fluid and any outdoor exposure |
| TPU | Flexible gasket rings | Field TPU; note UV if outdoor |
| Drawing callout NBR/EPDM | Legacy rubber names on prints | Describe media in notes; map to TPE/TPV on RFQ |
Compression set
Every squeezed elastomer keeps some of the squeeze permanently.
Where the gasket lives
Assembly reliability against flexibility later.
Avoid these
Two choices that leave a joint looking closed after it has stopped sealing.
Filling the groove until the gasket has nowhere to bulge. The clamping load then tries to force the joint open instead of sealing it. Leave width for the material to move, and do not squash the section solid.
Expecting a thermoplastic elastomer to keep pushing like a rubber compound in a hot cabinet. These gaskets take a permanent set, and heat speeds that up. A joint that is fine at room temperature can lose its push after time in the heat.
Drawing
The joint, the load, and the temperature decide the material.
Housing and cover CAD showing the groove
Clamping method and how many fasteners
Service temperature, especially the high end
Fluids or gases the joint has to hold back
Service life and whether the joint is opened
Expected annual volume
Keep reading
Seals, soft resins, and the housings they close.
Lips and interference on moving parts.
SealsSealed boxes and covers.
EnclosuresSealed pass-through parts.
GrommetsCovers that clamp onto a rim.
LidsA common gasket material.
TPEA softer sealing grade.
SEBSBeads shot onto a housing.
OvermoldingHow we support industrial programs.
Industrial and transportationEvery part-type guide, grouped by family.
Molded parts libraryFAQ
The gasket took a permanent set and stopped pushing back hard enough. Heat is the main accelerator, so a grade rated for the peak temperature, or a deeper groove with more squeeze in reserve, is the fix. Heat aging a joint under its real clamping load, then measuring how much push is left, is the practical test.
Enough to follow the surface irregularities, and not so much that it is squashed solid. The groove also has to leave room for the material to bulge sideways, or the clamping load forces the joint open instead. A groove that is nearly full at room temperature leaves no room at all once the material warms and expands.
For many enclosure joints, yes. For joints that stay hot for years or see aggressive chemicals, rubber and silicone compounds still hold their push longer, and are worth comparing against. For those joints, a molded gasket is often used for the enclosure and a rubber one for the hot section.
It removes the assembly errors, which are a common source of leaks. A separate gasket is better where the joint is opened for service, or where the seal material may need to change later. Some designs use both, with an overmolded bead on the housing and a separate gasket only where service access is needed.
The section changes as the gasket turns the corner. Keep the section even around the turn, and space the clamps so the squeeze stays even along the joint.
The gaskets covered here are thermoplastic elastomers. The seal is the material pushing back after it is squashed. Name TPE, TPU, or TPV, and the fluid the joint has to hold.
Next step
Upload the housing and cover with the groove shown. DFM feedback covers gasket section, groove depth and width, corners, and overmolding options.