Skip to content
NetProto

Molded part guide: connector housings

Injection Molded Connector Housings

A connector housing is small, thin, and full of holes, and it still has to hold every terminal in the right place through mating cycles. That combination makes it one of the more demanding parts to mold well.

The job

The plastic decides where every pin ends up

Terminals are stamped metal. Their position, retention, and alignment all come from the molded housing around them.

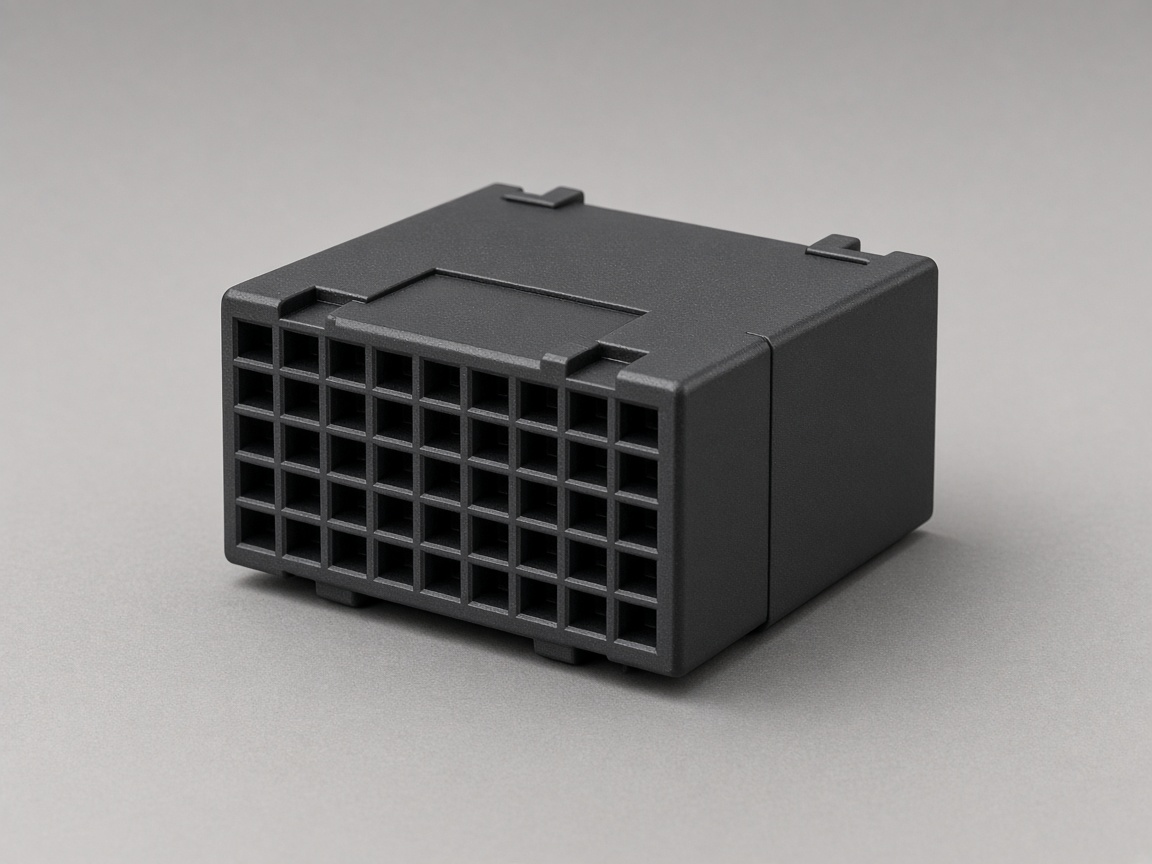
Each terminal cavity in the housing is formed by a thin steel core pin. The more cavities, the more pins, and the thinner the walls between them. Those walls are where short shots, weld lines , and sink tend to show up, and they are also the walls that hold the terminals in place.

A black molded connector housing with a grid of square cavities on one face

Long, narrow housings add a second problem: they want to bow. Glass-filled resins shrink differently along the flow than across it, so a housing gated from the wrong place can come out of the mold curved even though every wall is the right thickness. Pin alignment on a board-mount connector suffers first.

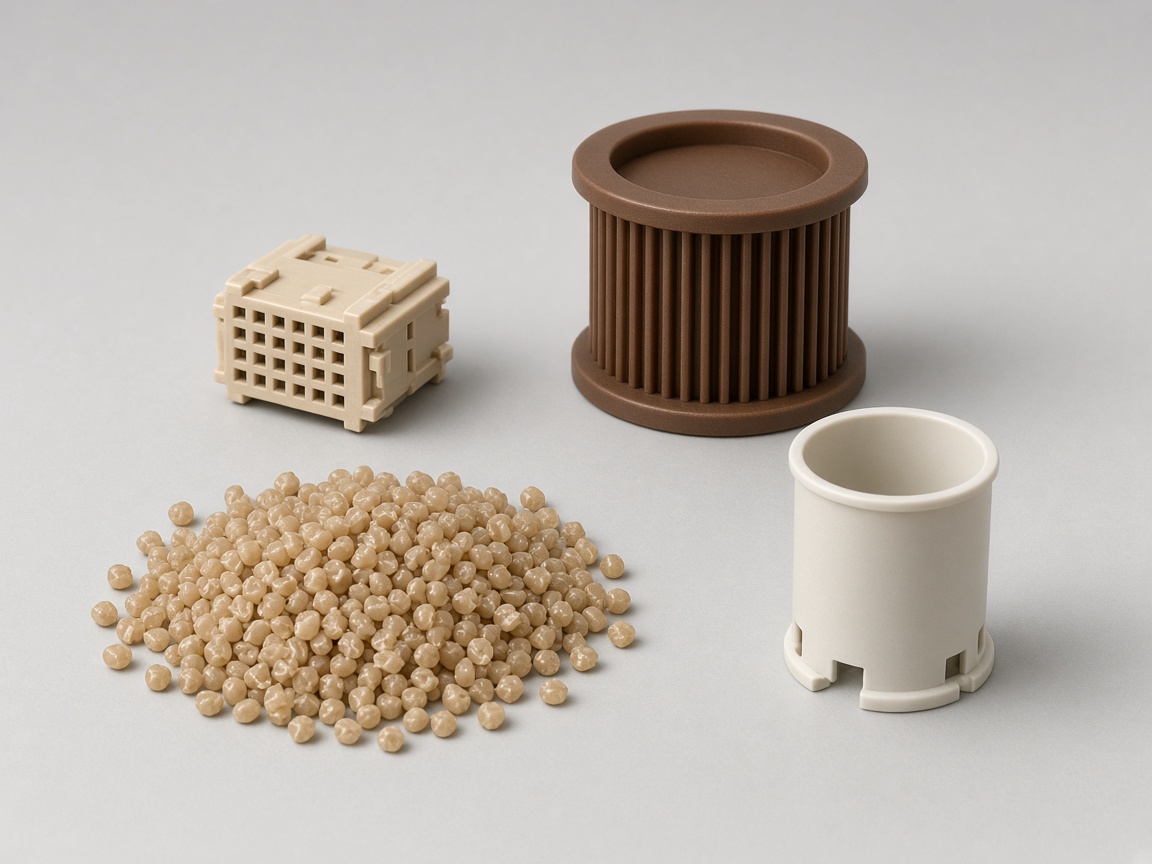
Beige pellets, a small beige grid housing, a brown ribbed cylinder, and a white slotted cup

If your connector mates with an off-the-shelf part, send that part number with the CAD. Mating geometry is not something to redraw from a catalog sketch.

Features

What each feature does and where it goes wrong in molding

General behavior across connector designs. DFM review looks at these on your geometry.

FeatureIts jobMolding risk
Terminal cavityLocates the terminal and guides the mating pin inLong slender core pins deflect under injection pressure, shifting the cavity
Retention finger or lance seatStops the terminal backing out when the wire is pulledThin, flexing plastic that cracks if the resin is brittle or the corner is sharp
LatchHolds the two halves matedFatigue over many mating cycles, and an undercut that may need a slide or lifter
Polarization keyMakes the connector impossible to mate the wrong wayLow risk, as long as the key survives the drop test
Secondary lock (TPA or CPA)Confirms terminals are seated, or that the connector is fully matedA separate small part that must slide or snap with the right force, molded to match the housing

Service tiers

Connector housing service tiers and quote path

Housing tier for this family: Terminal cavities, latches, and keeping long housings flat. Upload CAD with seal path, fasteners, and heat sources called out in notes when they are not modeled.

TierEnvironmentWhat matters mostTypical molded routeQuote path
1 Terminal cavitiesLocate the terminalThin walls and long core pinsCores that can shift under pressureUpload CAD; send the terminal
2 LatchHolds the halves matedA sharp root or a weld line through the beamA fillet at the root, and the weld line off the beamInstant quote; note the latch
3 KeyStops mating the wrong wayIt still has to survive handlingA key molded with the housingUpload CAD
4 Secondary lockConfirms the terminals are seatedIt has to slide or snap with the housingSame resin in one tool, or its own tool if the resin differsInstant quote; name the lock
5 Long housingPin alignment on a board-mount partGlass-filled resin can bow itGate so the flow runs along the lengthUpload CAD; note the gate

Materials

Resin families: quick reference for quote notes

One primary family per shell line item. Put latch and solder-heat notes in comments.

FamilyTypical use on this part typeNotes for instant quote
Glass-filled nylonWire-to-wire housingsField nylon; it absorbs moisture
Glass-filled PBTWire-to-wire housings when the drawing names PBTField glass-filled PBT
LCPBoard-mount parts that see reflowField LCP
PPSBoard-mount parts that see reflowField PPS

Resin and heat

Pick the resin for the thinnest wall and the hottest process

Connector resins are chosen for how well they fill thin sections, how they hold up to heat, and what flame rating they carry.

  • Wire-to-wire connectors often use glass-filled nylon or PBT for toughness and flame-rated grades
  • Board-mount connectors that go through reflow solder need resins that keep their shape at solder temperature, such as LCP or PPS
  • Nylon absorbs moisture, which changes latch feel and dimensions between dry and conditioned parts
  • Gate a long housing so the flow runs along its length, and expect DFM review to check the gate against warp
Orange and black molded connector housings, some open, beside a metal enclosure

Terminals

Insert molded terminals or terminals stitched in after molding

Both are common. Volume, sealing, and how many terminals the housing carries usually decide.

Insert molded

  • Plastic flows around the terminals, so they are located and sealed in one step
  • No retention features needed, which frees up space in a dense layout
  • Terminals must be loaded into the tool every cycle, and a damaged terminal scraps the part

Stitched or pressed after molding

  • Housing and terminals are made separately and joined at assembly
  • Retention fingers or press-fit features have to be molded into the housing
  • Sealing needs a separate seal or a potting step

Avoid these

Common design mistakes on connector housings

Two choices that crack a latch, or bow a long housing.

A weld line through the latch beam, or a sharp corner at its root. The beam cracks where it flexes. Move the gate so the weld line lands off the beam, and add a fillet at the root.

A long housing gated from the side. Glass-filled resin shrinks differently along the flow than across it, so the housing bows and the pins miss the board. Gate so the flow runs along the length.

Drawing

What to send with a connector housing

The mold needs the terminal and the mating half, not only the housing shape.

  • Terminal part number and drawing, or CAD for custom terminals

  • The mating connector, or its part number if it is off the shelf

  • Whether terminals are insert molded or stitched in after molding

  • Solder process for board-mount parts, and the flame rating the product needs

  • Mating cycle target and wire pull requirement, if you have them

  • Any wire seal, grommet, or overmolded boot at the back of the housing

Keep reading

Related guides

Processes and design rules that connector housings lean on.

Insert molding

Molding plastic around terminals and pins.

Insert molding

PPS

Heat and chemical resistance for demanding connectors.

PPS

Warpage

Why long housings bow, and how gating changes it.

Warpage

Micro molding

Where connector parts outgrow conventional presses.

Micro molding

FAQ

Questions about molded connector housings

Can you mold a housing to mate with a standard connector?

Yes, if you supply the mating part's drawing or a sample. The mating features are then designed against the real part rather than a catalog outline, which is where most fit problems start.

Why do our latches crack after a few hundred cycles?

Usually a sharp corner at the root of the latch beam, a beam that flexes too far for the resin, or a weld line running through the beam. Moving the gate so the weld line lands elsewhere, and adding a generous fillet at the root, are common fixes.

Does the same tool make the TPA or CPA lock?

It can, as a family mold with the housing, when both parts use the same resin. If the lock needs a different resin or color, it runs in its own tool.

Do you certify connectors to automotive or agency standards?

No. NetProto manufacturing is ISO 9001 certified. Qualification of the finished connector to a product or industry standard is done by your team or your test lab.

Why does a terminal cavity shift?

The core pin that forms it is long and slender. Injection pressure can deflect it, so the cavity moves.

Why does a nylon latch feel different after the parts sit?

Nylon absorbs moisture. Latch feel and size change between a dry part and a conditioned one.

Next step

Quote the housing with its terminals

Upload the housing CAD with the terminal drawing and the mating part. DFM feedback flags thin core pins, latch undercuts, and warp risk before tooling is released.