

LCP
Very high flow for thin connector walls.
LCPProcess guide
Some parts are small enough that the sprue and runner weigh many times more than the part itself, and a normal screw moves more resin in a slight twitch than the whole shot needs. That is roughly where micro molding begins.
Where it starts
The line is set by what the equipment can control, not by a size on the drawing.
Micro molding handles shots too small for a standard screw to meter. Thin wall molding is a long flow through a thin wall on a normal press. Connector housings covers the part shape. LCP is one resin that fills fine features.
A small connector body or a hearing aid shell can often run on a small conventional press with a careful setup. It becomes a micro molding job when one of three things happens: the shot is too small for a standard screw to meter repeatably, the features are too fine for normal venting and ejection, or the tolerances are too tight to check with ordinary gauges.
Past that line, the process is rebuilt around the small shot. Presses split melting and injection, often with a separate plunger that measures out the exact volume. Molds are built with inserts machined to very tight tolerances. And inspection moves from calipers to microscopes and optical measuring systems.
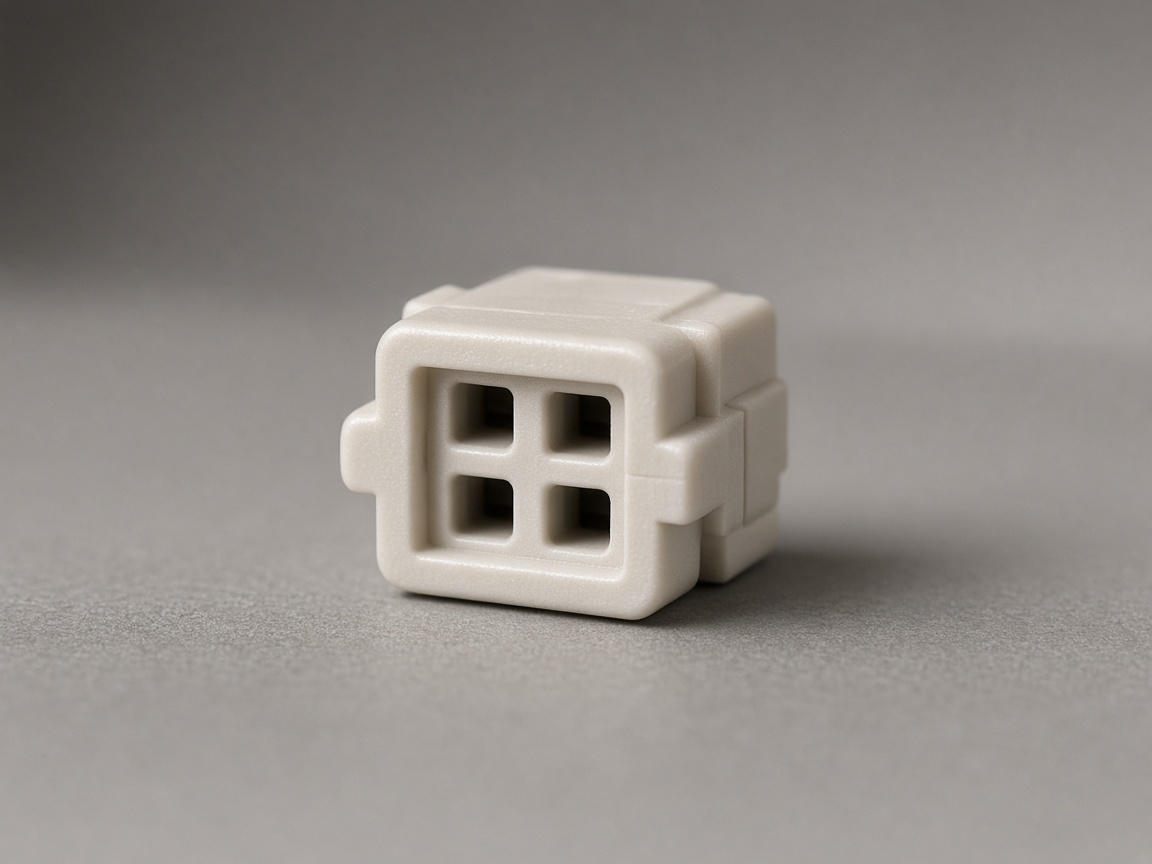
Roles
Micro molding covers shots too small for a standard screw to meter accurately. Thin walls here are a flow length problem, common on micro connectors.
| Page | Use it for |
|---|---|
| Micro molding (this page) | A shot too small to meter on a standard screw |
| Thin wall molding | A long flow through a thin wall |
| Connector housings | The connector body itself |
| LCP | A resin that fills fine features |
What breaks
Each row is a problem that barely matters on normal parts.
| Problem | Why it matters at micro scale | Usual answer |
|---|---|---|
| Shot metering | The shot is a tiny fraction of the screw's stroke, so small variations become large ones | Small diameter plunger or screw sized to the shot |
| Residence time | Resin sits in the barrel for many cycles and can degrade | Tiny melt volume, often melted in a separate stage |
| Runner to part ratio | Most of each shot is runner, which is wasteful with expensive resins | Very short runners, hot runner tips, or direct gating |
| Venting | Air trapped in a fine feature stops fill completely | Vacuum on the cavity before injection |
| Ejection | Pins bend or mark parts that weigh almost nothing | Parts removed with the runner, then separated off the press |
Fit
If the part fits on a small conventional press with standard venting and ejection, micro molding adds cost without benefit. A connector housing , or a thin wall that a normal screw can fill, usually belongs on those pages.
After the press
On micro programs, a large share of the effort goes into what happens after the mold opens.

Materials
The material has to flow into spaces that freeze almost instantly.
LCP is the standard for micro connectors: it flows extremely well in thin sections and holds its shape through reflow soldering. PEEK shows up in implantable and high temperature parts. Acetal and nylon handle tiny gears and mechanisms, and PC, COC, and PMMA are used where clarity matters, such as fluidic chips and optics.
Resin cost counts for less than usual, because the parts weigh so little. Runner waste counts for more. It can cost more than the resin in the parts, which is one reason micro molds work so hard to keep runners short.
RFQ inputs
Micro quotes stall on missing information more than on price.
The features that actually matter, marked on the model, with everything else at looser tolerance
How each critical feature will be measured, and by whom
Whether gate vestige is acceptable on any face
How parts should arrive: on the runner, in trays, or sorted by cavity
The resin grade, since many micro parts are designed around one specific material
Keep reading
Materials, small parts made by conventional molding, and the markets that use micro parts.
Very high flow for thin connector walls.
LCP
High temperature and implant grade parts.
PEEK
Small gears and sliding parts.
Acetal (POM)
Small, precise, and usually conventional.
Connector housings
Enclosures for handheld and bedside devices.
Medical device housings
Tooth form, backlash, and resin choice.
Gears
Long flows through thin sections.
Thin wall molding
Every molding process and secondary operation.
All processesFAQ
No. A small conventional press still meters like a larger one. Micro molding starts when the shot is too small to meter, the features are too fine to vent and eject, or the fit cannot be checked with ordinary gauges.
The work is in the steel: fine cavities, venting, and a way to prove each cavity. Less steel does not mean a simpler mold.
Other methods often show the shape and miss the fit. Many programs start with one cavity so the fit can be checked in the real resin.
Thin wall molding pushes a normal shot through a long thin wall. Micro molding is about a shot, a feature, or a fit that a normal press and gauge cannot handle.
Connector bodies, small gears, and fine mechanism parts. The resin still has to reach the end of the feature. LCP, PEEK, and acetal are common starting points.
No. The line is whether a standard screw can meter the shot and whether the feature can be vented, ejected, and measured. Send the CAD and the fit that matters.
Next step
Upload CAD for DFM review and an instant quote on the injection molded part.