
Gasketed lid
- The sensor can be opened for calibration or repair
- Needs a flat gasket land, screw points, and room for the seal
- Leaves air inside, so condensation needs a plan
Molded part guide: sensor housings
A sensor housing is not just a box. Light, sound, pressure, or a magnetic field has to reach the sensing element through or around it, so the housing becomes part of the measurement.
The job
Every sensor housing trades protection against signal. Where that trade lands depends on what the sensor measures.
An enclosure for a controller can be as closed as the heat allows. A sensor housing cannot. The optical sensor needs a window, the pressure sensor needs a port, the ultrasonic transducer needs a face that passes sound, and the proximity sensor needs nothing conductive between it and the target. The molded part has to leave that path open while still keeping out water, dust, and handling damage. Metal injection molding is a different process. This page covers thermoplastic housings.
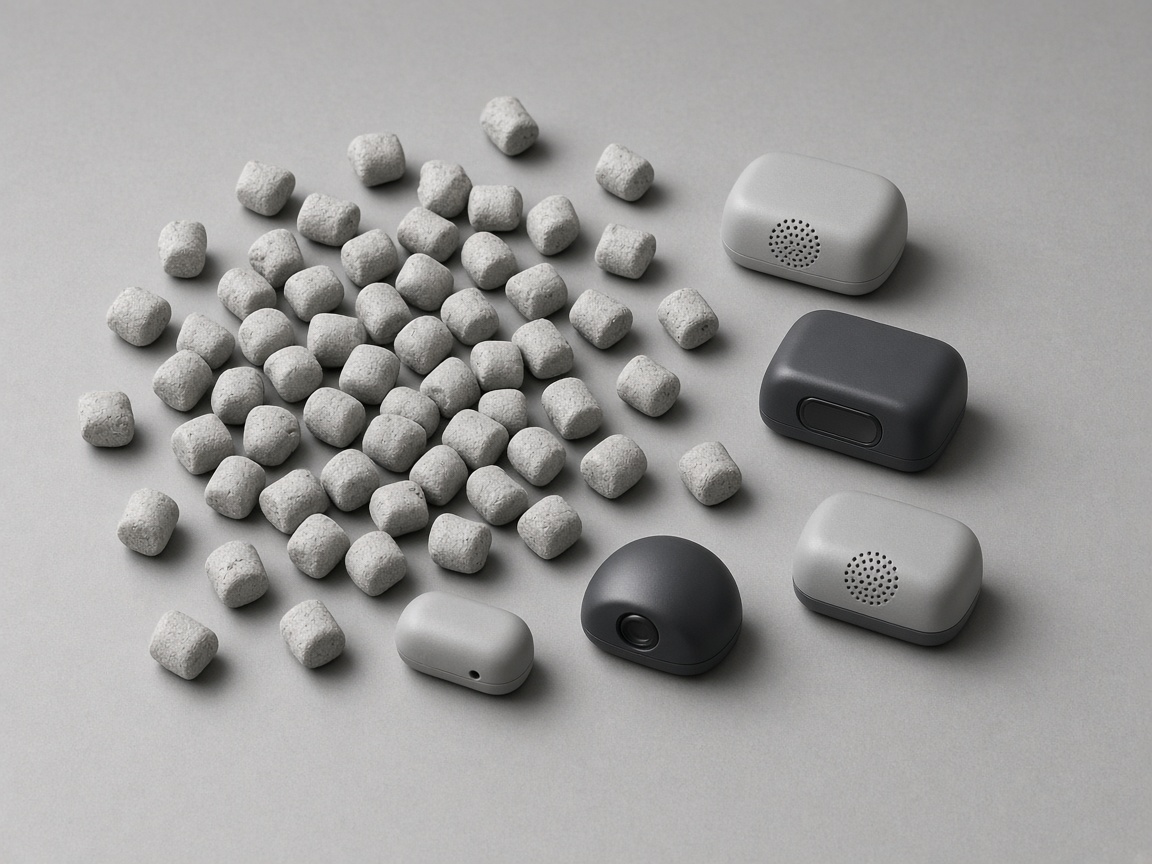
The housing also aims the sensor. Mounting faces, locating pins, and the seat for the sensing element are datums. If they move with warp or shrink, the reading moves with them, which is why these features deserve a place on the drawing with their own callouts rather than being inherited from the general tolerance block.
By sensing type
General design behavior. Your sensor supplier's mechanical notes take priority where they exist.
| Sensor type | What the housing must allow | Common molded solution |
|---|---|---|
| Infrared receiver or proximity | A window that passes infrared while hiding the inside | An IR-transmitting resin that looks black to the eye, kept thin enough over the sensor to limit signal loss |
| Camera or visible light | An optically clear, scratch-resistant window | A separate clear lens seated in the housing, so the lens resin can be chosen, or the lens replaced, without changing the housing |
| Ultrasonic transducer | A face that passes sound, and isolation so the housing does not ring | A controlled front face in front of the element, with a softer overmold or potting behind it to damp vibration |
| Pressure or flow | A port to the medium, sealed from the electronics | A molded port with an O-ring gland, or a membrane seat, with the parting line kept off the sealing surface |
| Hall effect or inductive | Nothing conductive or magnetic between the sensor and the target | A plain plastic sensing face, with metal inserts and fasteners kept away from it |
Service tiers
Housing tier for this family: Windows, potting, and cable exits around the sensing element. Upload CAD with seal path, fasteners, and heat sources called out in notes when they are not modeled.
| Tier | Environment | What matters most | Typical molded route | Quote path |
|---|---|---|---|---|
| 1 Window | IR, or a clear lens | The window is part of the reading | An IR grade, or a separate clear lens | Upload CAD; name the sensor |
| 2 Pressure port | A port to the medium, sealed from the electronics | A parting line on the seal | Keep the parting line off the sealing surface | Instant quote; note the port |
| 3 Ultrasonic face | A face that passes sound | The housing can ring | A controlled front face, with a softer overmold or potting behind it | Upload CAD; note the element |
| 4 Potting | The housing is the pot | PP and PE are hard for the compound to grip | Name the resin and the compound, and give the air a way out | Instant quote; name the compound |
| 5 Cable exit | A boot, a gland, or an overmold | The pull lands on the solder joints | Move the bending load off the board | Upload CAD; note the cable or connector |
Materials
One primary family per shell. Name the window resin and the potting compound in comments.
| Family | Typical use on this part type | Notes for instant quote |
|---|---|---|
| PE | Potting compounds grip it poorly | Field PE; name the compound if the part is potted |
| IR-transmitting | A window that looks dark and still passes infrared | Field the IR grade; the shell can be a different resin |
| Clear lens | A separate window seated in the housing | Field the lens resin separately from the shell |
| PP | Potting compounds grip it poorly | Field PP; name the compound if the part is potted |
Potting
Potting seals and supports the electronics, but only if the compound bonds to the housing and fills without trapping air.
Low surface energy resins such as polypropylene and polyethylene are hard for potting compounds to grip. Housings that will be potted are often molded in resins that bond more readily, and the inner walls can be given a texture or small grooves so the compound locks in mechanically rather than relying on adhesion alone.
Give the compound a way in and the air a way out. A fill opening at one end, a vent at the high point, and no blind pockets under the board let the potting fill in one pour. Mold release left on the part also weakens the bond, so say on the quote that the part will be potted.
Sealing
Both keep water out. They differ in what happens when something goes wrong.
Cable exit
The cable is pulled, bent, and flexed for the life of the sensor. The housing has to take that load instead of the solder joints.
A molded strain relief boot, a cable gland threaded into a molded boss, or an overmold that bonds to the cable jacket all move the bending load away from the board. Overmolding also seals the exit in the same step, which is why it is common on sensors that live outdoors or on machinery.
If the sensor uses a connector instead of a pigtail, the connector cavity is part of the housing. Terminals can be insert molded so the pins are located and sealed by the plastic itself, which removes a separate seal and an assembly step.
Avoid these
Two choices that show up after the first parts are molded.
Tolerancing the housing before the sensing element is chosen. Beam angle, focal depth, and port size decide how tight the mounting face and the window need to be. Pick the element first, then give those faces their own callouts instead of leaving them on the general tolerance block.
Running the gate, the parting line, or ejector pins across the window, the seal land, or the mounting face. Those surfaces are what the reading and the seal depend on. Keep them clear, and say so on the drawing.
Drawing
Most of these come from the sensor datasheet or the mechanical notes from its supplier.
The sensing element part number and its mechanical notes, including any window or port guidance
Which faces are datums for aiming the sensor, and how they are toleranced
Whether the housing is potted, gasketed, or overmolded, and with what compound
Cable jacket material and diameter, or the connector and terminals
The environment: outdoor exposure, washdown, chemicals, and temperature range
Any inserts, and how far they must stay from the sensing face
Keep reading
Processes that sensor housings rely on, and the sibling housing pages.
Seal the cable exit and add a soft damping layer in the same part.
OvermoldingTerminals and threaded inserts located and sealed by the plastic.
Insert moldingAn insert molded mount for a sensor assembly.
Insert molding sensor bracketWhen the sensor plugs in instead of using a pigtail.
Connector housingsBoard mounting, shielding, and heat inside a molded shell.
Electronic enclosuresCalling out the datums that aim the sensor.
GD&T for molded partsChoosing a clear resin for a window or lens.
Polycarbonate vs acrylicWhy mounting faces move after molding, and how to stop it.
WarpageEvery part-type guide, grouped by family.
Molded parts libraryCamera and reader housings.
Security hardwareFAQ
It can, if the whole housing is molded in an IR-transmitting resin. More often the window is a separate part in an IR-transmitting grade, or a second shot, so the housing itself can use a different resin.
The usual cause is the compound pulling away from the housing wall as both expand and contract at different rates. A resin that bonds better, a textured or grooved inner wall, and clean parts without mold release on the bonding surface all help.
Yes. Overmolding bonds a second material over the cable jacket and the housing, forming the strain relief and the seal in one step. Share the cable jacket material, since adhesion depends on it.
No. An ingress rating belongs to the finished, assembled product and is proven by your testing. The molded housing gives the seal the surfaces it needs to pass.
It can sit on the side the product needs, as long as a strain relief or gland boss fits there. The parting line, gate, and ejector pins all use that same area. Mark the exit side on the drawing so the tool is planned around it.
Nothing conductive or magnetic should sit between that sensor and the target. Keep inserts and fasteners off the sensing face.
The lens resin can be chosen on its own, and the lens can be replaced without changing the housing.
Next step
Upload the housing CAD and attach the sensor datasheet or mechanical notes. DFM feedback covers the window, port, and cable exit before tooling is released. NetProto manufacturing is ISO 9001 certified.