
Adhesive mount
- No holes in the panel, and fast to install
- Needs a clean, smooth, room temperature surface
- Bond weakens with heat, oil, and dust
Molded part guide: cable management
Cable trunking, finger ducts, tie mounts, and routing channels are all long parts with the same feature repeated dozens of times. That repetition is what makes them interesting to mold: the last finger has to be as good as the first one, and the whole length has to come out straight enough to screw to a flat panel.
Repeated features
Cable trunking, finger duct, tie mounts, routing channels, and cover strips.
A length of finger duct is a channel with a row of flexible fingers along both sides. Melt entering at one end has to reach the last finger with enough pressure left to pack it properly. Fingers near the feed point pack hard and end up slightly denser and stiffer, fingers at the far end arrive last and pack least, and the spring in them is not the same.
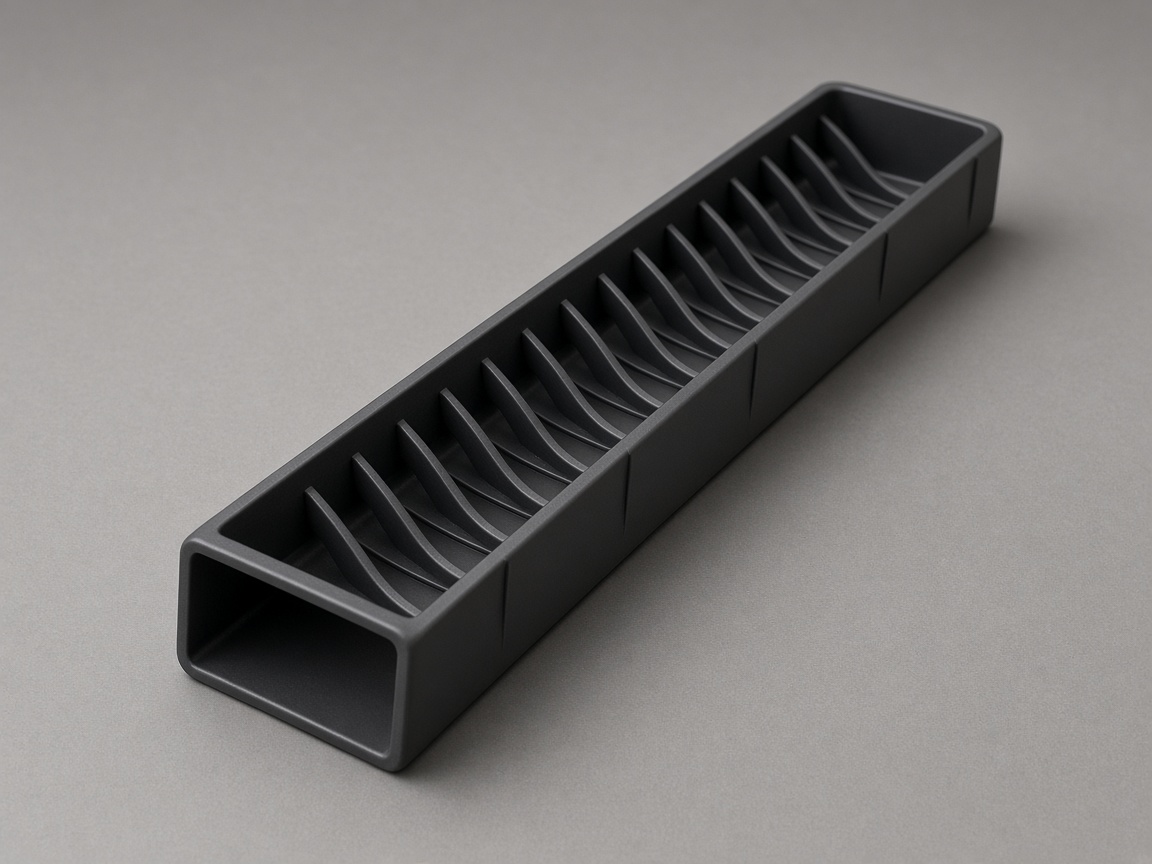
Installers feel that difference immediately. A finger that has been packed less is softer, bends further, and does not close back over the cable, so cables creep out of the duct. Feeding a long part at several points along its length, or at the middle rather than one end, evens out how the fingers behave from end to end.
Straightness comes next. A long part with features on one side only cools unevenly and bows along its length, and a bowed length of trunking will not sit flat against a panel. Keeping the section even across the part, cooling both faces at a similar rate, and supporting the length while it finishes shrinking all keep it flat.
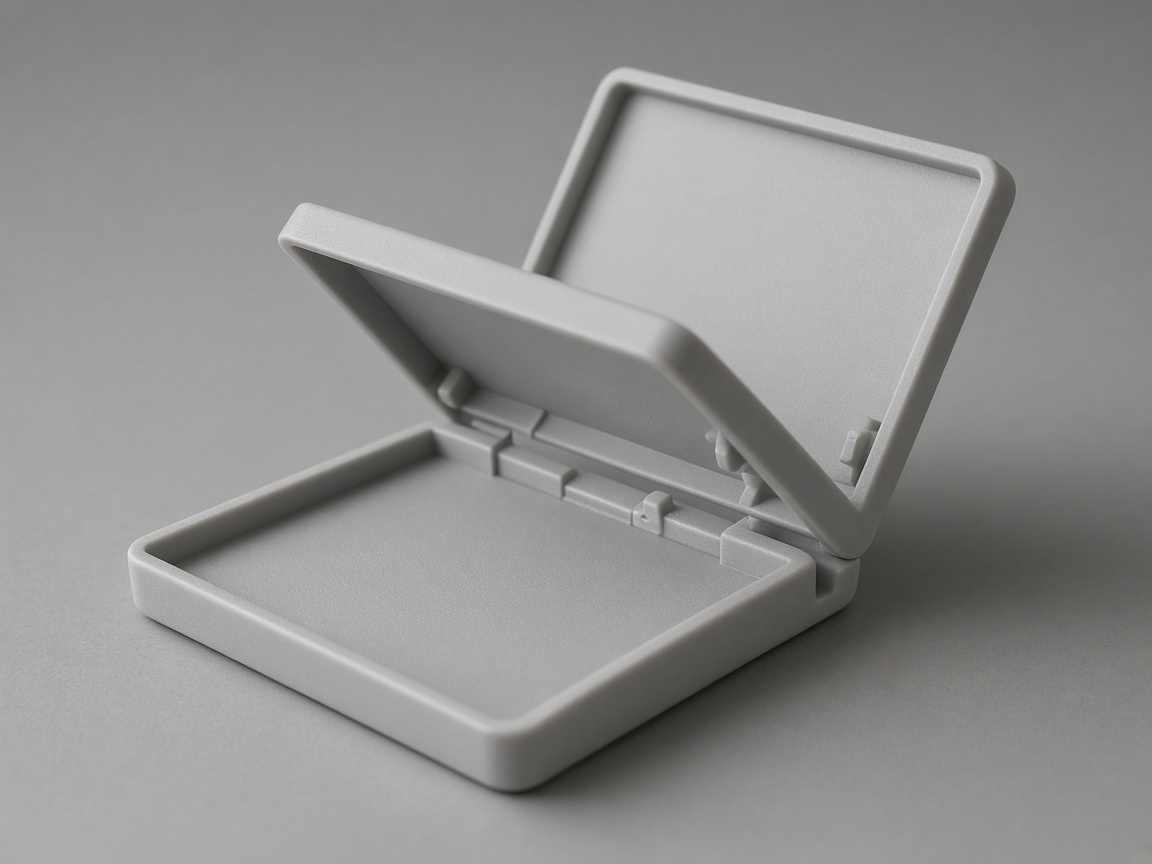
Covers are usually held by a living hinge or by snap edges. A living hinge is a thin strip molded in one piece with the cover, and it only survives repeated opening if the melt flows across it as the part fills, lining up the molecules along the bend. Mounting is by screws, by adhesive pads, or by clips into a panel, and each one changes how the part is designed underneath.
Features
Repeated features and long lengths drive the design.
| Feature | Purpose | Design note |
|---|---|---|
| Flexing fingers | Let cables in and hold them | Even packing from end to end keeps the spring the same |
| Channel base | Carries the cable run | Even section so the length stays straight |
| Living hinge cover | Opens for access | Melt must flow across the hinge as it fills |
| Snap edges | Hold the cover shut | Consistent engagement along the whole length |
| Mount points | Screws, adhesive, or clips | Chosen with the panel surface in mind |
Service tiers
Part focus: Even fill along finger duct, living hinge covers. Upload CAD with critical fits and environment in notes when not modeled.
| Tier | Environment | What matters most | Typical molded route | Quote path |
|---|---|---|---|---|
| 1 Finger duct | Panel or cabinet run | Even finger spring from end to end | PP, with feed along the length | Instant quote; note the length |
| 2 Hinge cover | Cover opened in service | Flow across the bend | PP hinge, or snap edges if it opens often | Instant quote; note how often it opens |
| 3 Mount | Screws, adhesive, or a panel clip | Surface condition and heat | PP or nylon mount | Instant quote; name the mount |
| 4 Outdoor | Sun and weather on a long part | UV along the length | UV-stable PP or ASA | Instant quote; note outdoor exposure |
| 5 Chemical splash | Oils or cleaners nearby | Cracking at the fingers | Resin checked against the fluid | Instant quote; name the fluid |
Materials
One primary family per line item. Put commercial grade, fillers, and environment filters in comments.
| Family | Typical use on this part type | Notes for instant quote |
|---|---|---|
| PA (nylon) | Cable clips and screw mounts | Field Nylon; not for the living hinge |
| PP | Finger duct and living hinge covers | Field PP; flow must cross the hinge |
| PC | Clear covers, not the hinge | Field PC; do not hinge this resin |
| POM (acetal) | A small local feature, not the duct | Field POM; say if it is only a detail |
| PBT / PPS | Hot or chemical service, not the hinge | Name the grade in notes; do not hinge it |
Even fill
A long part packs unevenly, and repeated features show it clearly.

Mounting
Both are used constantly, and they suit different surfaces.
Avoid these
Two choices that show up when the first cables are laid in.
Feeding a long duct from one end and expecting every finger to spring the same. Fingers far from the feed often pack less and stay softer, and cables creep out. A second feed, or a feed near the middle, evens the length. If the tool already runs from one end, check the first and last finger and shape the far fingers so they still close.
Expecting a long living hinge to behave like a short one. Thickness varies along a long hinge, and the thin spot is where it splits. If the cover is opened often, snap edges can outlast the hinge and can be replaced without the whole length.
Drawing
Cable size and the mounting surface decide the shape.
Trunking CAD, or the channel size and length you need
Cable sizes and how many cables go in each run
Mounting method and the surface it attaches to
Whether covers are opened often after install
Temperature, sunlight, and any flame rating you require
Expected annual volume
Keep reading
Clips, hinges, and the long parts that bow.
Single clips along a run.
Cable clipsSealed pass-through parts.
GrommetsClip design in general.
ClipsHolding boards and rails clear.
StandoffsCovers that open again and again.
Living hingeWhen one end packs harder.
Unbalanced fillingThe usual living hinge resin.
PolypropyleneHow we support industrial programs.
Industrial and transportationEvery part-type guide, grouped by family.
Molded parts libraryCable ducts and clips in trains.
RailCovers, sensor housings, and motion parts on automation hardware.
Robotics and automationFAQ
They were packed less because they are furthest from the feed point. Moving the feed to the middle of the length, or adding feed points, evens the spring from end to end. Checking the spring of the first and the last finger on the same part is a quick way to see how even the fill is.
Features on one side cool differently from the plain side. An even section, balanced cooling, and support while the part finishes shrinking keep it flat. Support while the part finishes shrinking matters most on the longest lengths, where a small bow becomes a large gap.
The hinge was not formed by melt flowing across it. A hinge only gains its life when the flow lines up along the bend as the part fills. Where covers are opened often, separate snap edges outlast a hinge and can be replaced without the whole length.
Adhesive is faster and leaves no holes, but it needs a clean, cool, smooth surface. Screws hold on rough, oily, or hot surfaces where adhesive lets go.
A short length often can, because the pressure drop along it stays small. On a longer length the first and last fingers can feel different. Squeeze both on a sample. If they do not match, add feed points.
Polypropylene is the usual choice, because the melt can line up across the bend as the part fills. Some polyethylene grades also hinge. ABS, polycarbonate, and nylon are poor hinge resins. If the rest of the cover needs one of those, the hinge can be a second shot in polypropylene, or the cover can use snap edges instead.
Next step
Upload the part, or tell us the channel size and cable count. DFM feedback covers feed points along the length, finger spring, hinges, and mounting.