
Wire EDM
- Through cuts, insert profiles, and ejector pin holes
- Straight walls when the wire path can enter and exit the block
- Parting plates and slider tracks cut after heat treat
Glossary
Wire EDM uses a traveling wire electrode to through cut hardened mold steel for insert profiles, parting plates, ejector pin holes, and slider tracks. It complements sinker EDM on through geometry.
Definition
Wire EDM uses a traveling wire electrode to through cut hardened mold steel for insert profiles, parting plates, ejector pin holes, and slider tracks.
Wire EDM cuts through hardened steel along a programmed path using a continuously traveling wire electrode.
Mold shops use it for insert outlines, parting plates, ejector pin holes, slider tracks, and through features that need a straight wall or tight corner.
It complements sinker EDM on geometry that can be cut from one side to the other.
Start and stop marks may appear where wire entry and exit are visible unless the process hides them on shutoffs.
Toolmaking
Insert profiles, ejector pin holes, and parting plates are common wire EDM jobs.
Versus sinker
Different geometry problems, not competing labels for the same feature.
Tooling
These features show up on mold build plans, not on part drawings alone.
Wire EDM insert profile cuts after heat treat for pocket fit
Ejector pin holes and through slots in hardened plates
Parting plate and slider track outlines with tight clearance
Review
Wire diameter selection and corner radius drive spark gap and skim time.
Minimum internal corner radius tied to wire diameter and overburn
Whether wire entry marks must land on non cosmetic shutoff steel
Insert clearance and parallelism after wire cut on mating plates
Wire EDM wins over CNC milling when steel is already hardened or internal corners are tighter than end mill radius
Recast layer on shutoff faces may require skim passes; note acceptable finish on drawing
Go deeper
Open the guide that matches your geometry question.
Blind ribs and shaped electrodes.
Sinker EDMWire start holes and deep vents.
Hole-drilling EDMSinker, wire, and hole drilling hub.
EDM overviewRFQ notes for EDM texture on parts.
EDM finishWire cut inserts on the core half.
CoreWire cut inserts on the cavity half.
CavityPlates that receive wire cut inserts.
Mold baseVisual reference
Images are selected from the NetProto Forge media library for this topic.

Wire EDM machine cutting with sparking wire through mold ste
Wire EDM machine cutting with sparking wire through mold steel

Wire EDM finished mold insert profile on steel plate
Wire EDM finished mold insert profile on steel plate
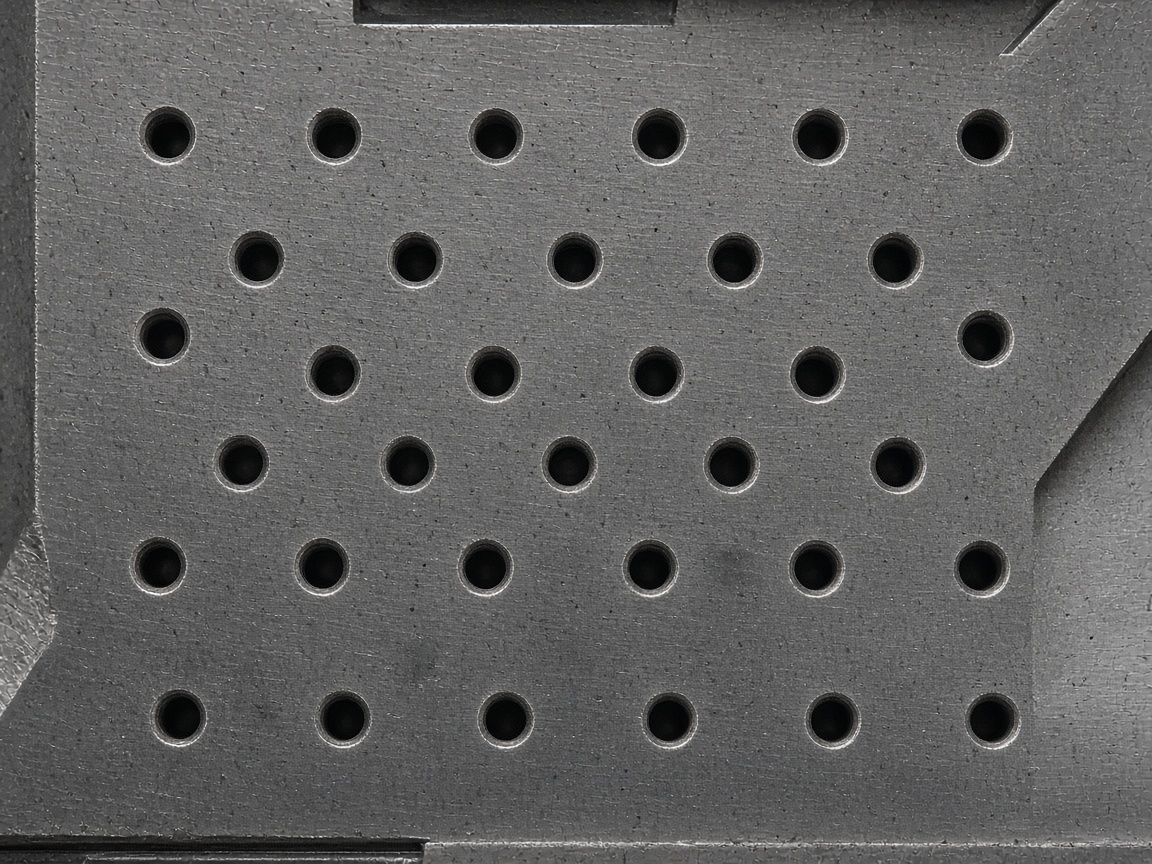
Ejector pin holes cut by wire EDM in hardened mold plate
Ejector pin holes cut by wire EDM in hardened mold plate
FAQ
Corner radius is set by wire diameter plus spark overburn. Finer wire and skim passes tighten corners but add time.
Thicker plates are possible but cut time and wire deflection rise. Shops balance speed, accuracy, and plate stack height on the quote.
Yes when the path begins inside solid steel. Hole drilling EDM often creates the start hole before the wire threads through.
Finer wire suits tighter corners and small insert outlines. Coarser wire suits faster roughing on larger through profiles. The mold maker picks from common shop wire sizes.
Yes. Taper or four axis wire paths cut upper and lower profiles that differ, within machine travel limits.
Wire EDM cuts hardened through features with low cutting force but slower metal removal than milling on open soft steel.
Next step
Upload CAD with through cut features such as insert profiles, ejector pin holes, and parting plates to confirm wire EDM scope and lead time for your program.