
Cavity
Exterior half versus interior half.
CavityGlossary
The mold core is the interior forming half of the tool. It carries ribs, bosses, ejection, and many shutoffs that affect part quality.
Definition
The mold core is the internal forming half of an injection mold, usually on the moving B side.
It shapes interior geometry: ribs, bosses, undercuts, and inside walls.
While the cavity forms the exterior surface, the core defines internal features and often carries most of the ejection system.
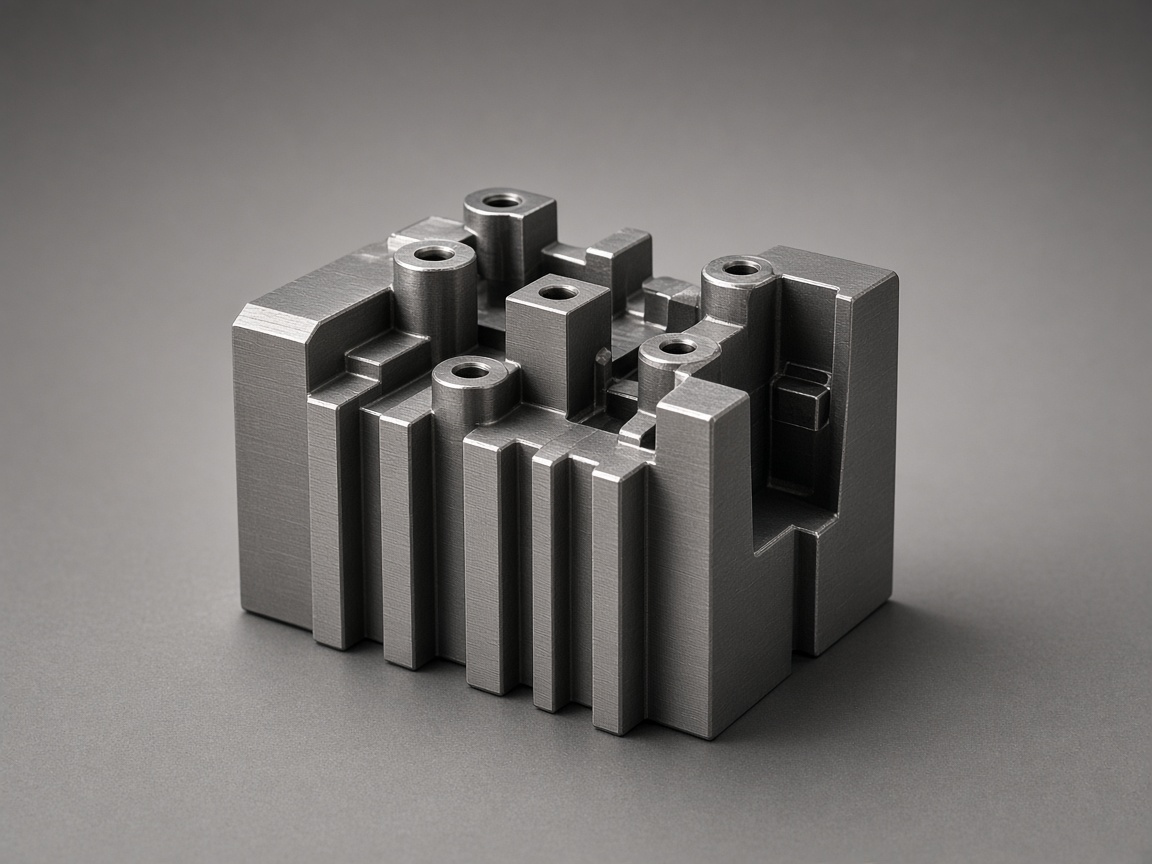
Core steel must survive ejector pin contact, vent channels, and sliding shutoffs when side actions exist.
When buyers ask for zero draft on an interior wall, core pull (drag on release) and scuff marks become the negotiation.
Tooling
Most ejection and vent issues show up on the core before the first sample ships.
Core side red flags
Fix these in CAD before approving steel cut.
Blind ribs with no vent path to atmosphere
Boss stacks thicker than the primary wall without coring
Sharp internal corners that drive stress and polish drag
Undercuts on the core pull without side action budget
Core side features with no practical cooling path. Long cycle time and uneven shrinkage can follow.
Go deeper
Each link is a different angle on the same program, not a duplicate definition.
Exterior half versus interior half.
CavityWhich mold half mounts where.
A side and B sideAir must leave as plastic enters core details.
VentHow parts release from the core after cooling.
Ejector pinVisual reference
Images are selected from the NetProto Forge media library for this topic.
Injection molded production parts on a tray
Injection molded production parts on a tray
Engineer reviewing a molded part drawing
Engineer reviewing a molded part drawing
Plastic housing components from a steel tool
Plastic housing components from a steel tool
FAQ
The cavity forms exterior surfaces customers see. The core forms interiors, ribs, bosses, and inside walls. Ejection pins and many vents usually live on the core half.
Yes. Insert cores and interchangeable pins are standard maintenance paths.
Stick or drag often traces to insufficient draft, polish drag on deep ribs, vacuum in blind features, or resin shrink gripping the core. Venting and ejection layout review usually come first.
Core pull marks are scuff or drag on interior walls during release. Ejector pin marks are localized push points where pins contact the part. Both belong in cosmetic acceptance when interiors are visible.
Interior walls and ribs need draft aligned with the core pull direction. Exact degrees depend on depth, resin, and texture. Document draft on the drawing and confirm in DFM before steel cut.
Thick boss roots on the core side pull material and can show as sink opposite the boss on the exterior.
Not always. Wear and polish requirements differ by region and can use inserts.
Vents let air escape as melt fills ribs and pockets on the core side. Blind ribs without a vent path are a common short fill or burn risk.
Next step
Upload CAD with rib and boss stacks visible before tooling deposit.