
Ultrasonic welding
- Continuous joint that follows every turn
- No extra parts, and nothing to loosen
- Permanent, so the manifold cannot be opened
Molded part guide: manifolds
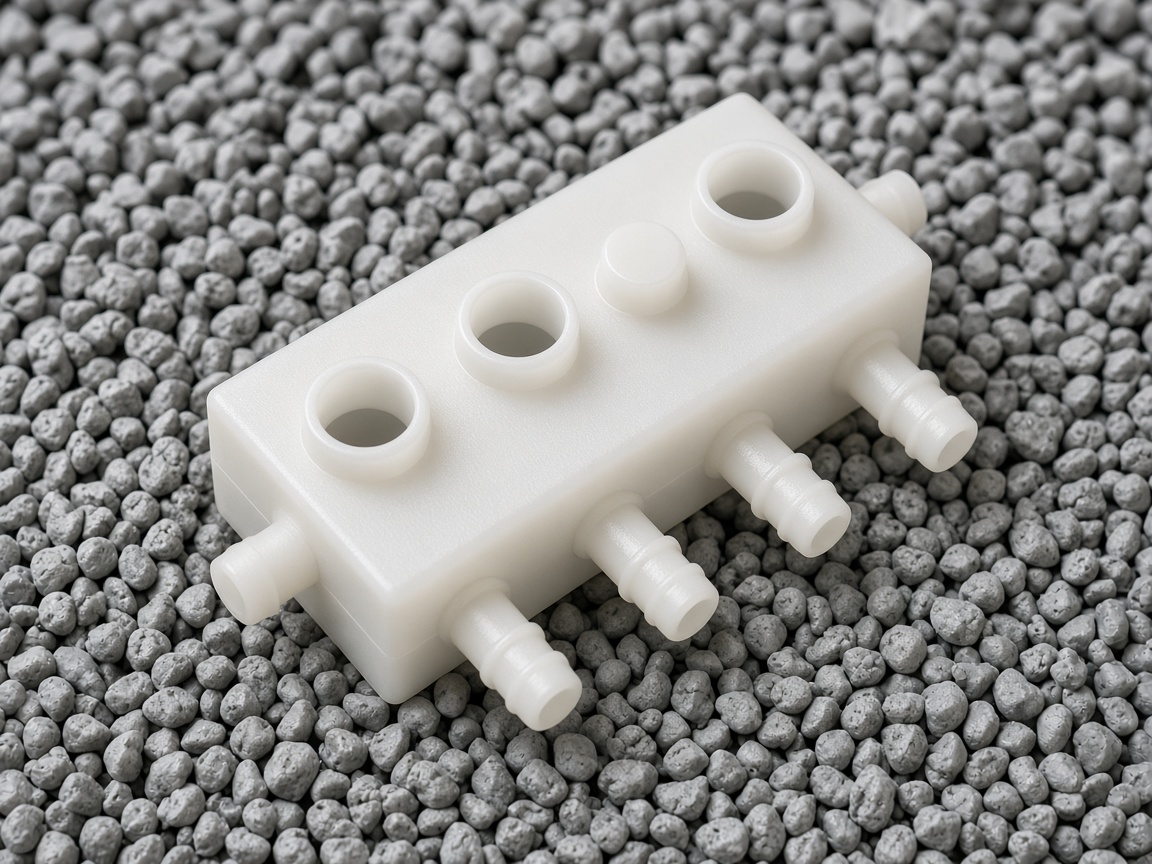
A manifold takes one inlet and feeds several outlets, which means internal passages that branch, turn, and cross each other. Almost none of that can be formed by cores that pull straight out of a tool. So a molded manifold is usually two parts that become one, and the joint between them is the design.
Two halves
Fluid manifolds, air manifolds, distribution blocks, and cooling plates.
A core has to be able to come out. That means every passage a core forms must run along the direction the tool opens, with nothing in the way. A manifold breaks that rule immediately: its passages branch sideways, turn corners, and often pass over and under each other. A few side actions can rescue a simple case, but a branching network cannot be built that way.
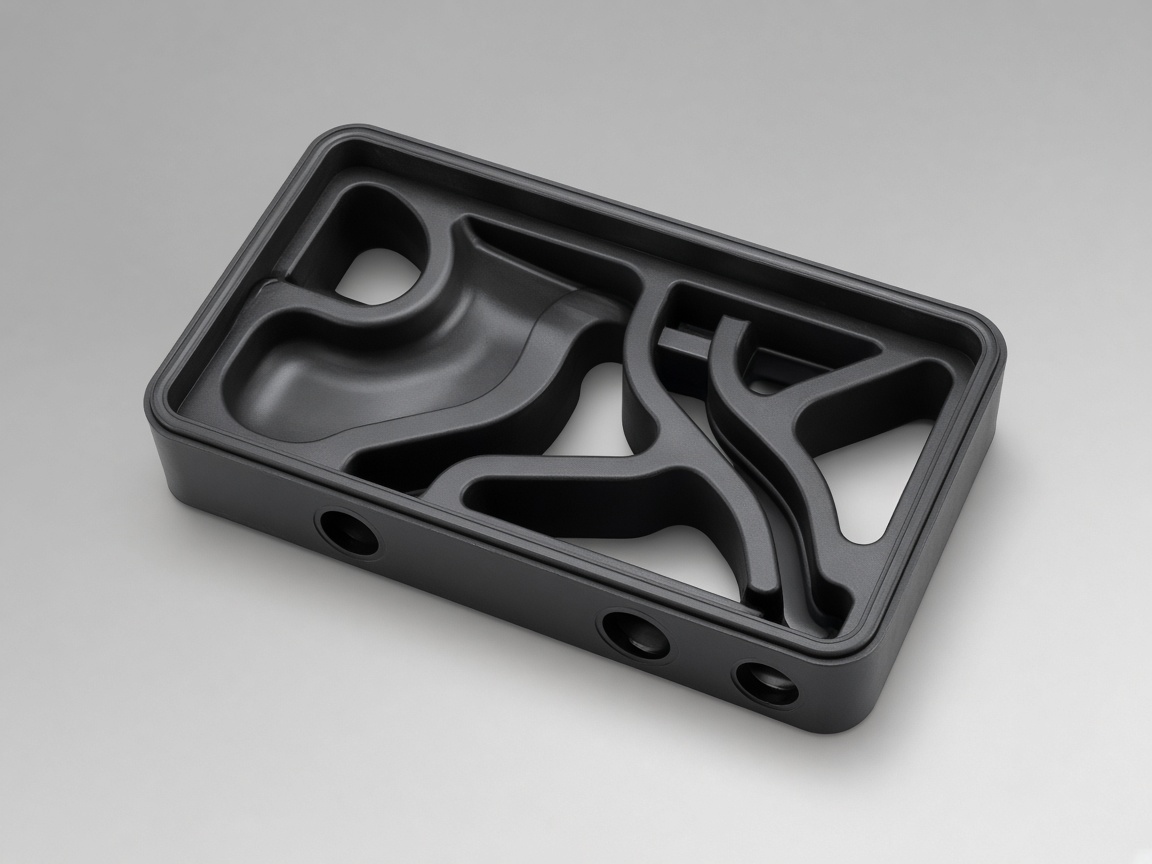
So the manifold is split along the passages. Each half is molded as an open channel, which cores can reach easily, and the two halves are then joined so the open channels become closed passages. Suddenly the hard part is not the passages at all, it is making a joint that holds pressure everywhere along a long, winding seam.
Ultrasonic welding is the usual method. A small raised ridge along the joint on one half melts under vibration and fuses into the other half, giving a continuous bond that follows the passage wherever it goes. The joint has to be designed so that melted material is contained rather than squeezed into the passage, where it would restrict flow or break off later.
Ports are the other weak point. Melt flowing around a port opening splits and closes again on the far side, and that closing line is weaker than the material around it. Under pressure those lines are exactly where a manifold splits. Feeding the part so the lines fall between ports rather than across them, and adding material around each port, keeps them out of trouble.
Features
Split construction turns a tooling problem into a joining problem.
| Feature | Purpose | Design note |
|---|---|---|
| Open channels | Molded passages before joining | Cores reach them easily in each half |
| Weld joint | Closes the passages | Raised ridge with a place for melted material to go |
| Ports | Inlet and outlets | Extra material, flow joints kept between them |
| Mounting points | Holds the manifold | Kept off the seam and off the passages |
| Pressure test feature | Checks the joint | A blanked port or a test boss for leak testing |
Service tiers
Part focus: Split halves, ultrasonic weld seam, port knit lines. Upload CAD with critical fits and environment in notes when not modeled.
| Tier | Environment | What matters most | Typical molded route | Quote path |
|---|---|---|---|---|
| 1 Open channels | Passages that branch and turn | Cores have to pull straight out | Split into two halves | Upload CAD; show the passages |
| 2 Weld joint | Has to hold along the whole seam | Melt stays out of the passage | Raised ridge with a place for the melt | Instant quote; say if it must open |
| 3 Ports | Inlet and outlets | Flow lines fall between the ports | Extra material around each port | Upload CAD; note the ports |
| 4 Serviceable joint | Has to open for cleaning | Screws, a gasket, and a groove | More parts than a weld | Full RFQ; show the fasteners |
| 5 Mounting | Holds the manifold | Kept off the seam and off the passages | Bosses away from the joint | Instant quote; note the mounts |
Materials
One primary family per line item. Put commercial grade, fillers, and environment filters in comments.
| Family | Typical use on this part type | Notes for instant quote |
|---|---|---|
| Drawing resin | Both halves, so the pair can be welded | Field the grade on the drawing; name the fluid |
Joining
A manifold seam follows every branch and turn of the passage.
Joining method
Permanent and serviceable joints suit different products.
Avoid these
Two choices that put melt in the passage or a weak line across a port.
A weld ridge with nowhere for the melted material to go. Vibration pushes it into the passage, where it restricts flow or breaks off later. Give the melt a place to stay, outside the passage.
Letting the flow close across a port. That line is weaker than the wall around it, and pressure opens it. Feed the part so the lines fall between ports, and add material around each port.
Drawing
The passages and the joint plan decide everything.
Manifold CAD with the passage network shown
Working pressure and fluid
Port sizes and how each one connects
Whether the manifold must be serviceable
Leak test method you plan to use
Expected annual volume
Keep reading
Other fluid parts, welded joints, and the lines that leak.
Cored passages and side actions.
Valve bodiesCasings around a rotor.
Pump housingsLarge air paths and seams.
DuctingBarbs and thread sealing.
Irrigation fittingsWhere flow closes behind a port.
Weld linesDesigning a joint to be joined.
Assembly featuresA stiff, chemically steady option.
Glass filled PBTHow we support industrial programs.
Industrial and transportationEvery part-type guide, grouped by family.
Molded parts libraryFAQ
Cores have to pull straight out, and a branching passage network gives them nowhere to go. Splitting the manifold into open channels that are joined afterward solves it. Splitting along the passages also makes each half easy to inspect before the two are joined.
At a corner or a branch, where the two halves fit least well. Checking each half against its mate along the whole seam, rather than at a few points, catches this early. A short pressure test on every assembled manifold is the usual way to catch a joint that did not fuse properly.
Flow closes behind the port opening and leaves a weaker line there. Feeding the part so those lines fall between ports, and adding material around each port, is the fix.
Yes, with screws and a gasket instead of a weld. It adds parts and a groove around the passage, but the manifold can then be opened and cleaned. A serviceable manifold also needs enough room around the fasteners, which usually makes the body a little larger.
A few side actions can rescue a simple passage that still pulls out. A network that branches, turns, and crosses gives the cores nowhere to go. Split that manifold into open channels.
The fit along the whole seam, not just at the ends. Leaks show up at a corner or a branch, where the two halves fit least well.
Next step
Upload the manifold and its passage network. DFM feedback covers the split line, weld joint design, port flow joints, and leak testing.