
Molded halves
- Precise mounting features and joint faces
- Even section under close control
- Needs a seam that is joined and sealed
Molded part guide: ducting
Ducting carries air from one place to another around everything else in the way. That makes it long, curved, thin, and usually the last part anybody has room for. Molding it well is about filling a long thin shell all the way to the end, keeping it straight, and joining sections that never quite line up.
Long and thin
Air ducts, defrost ducts, blower outlets, vent tubes, and cable ducts.
Air ducts have a large surface and a thin section, which is a hard combination. The melt has to travel a long way through a thin space, cooling as it goes, and if it freezes before reaching the far end the duct comes out short. More than one feed point shortens the distance, at the cost of the flow joints that form where the fronts meet.
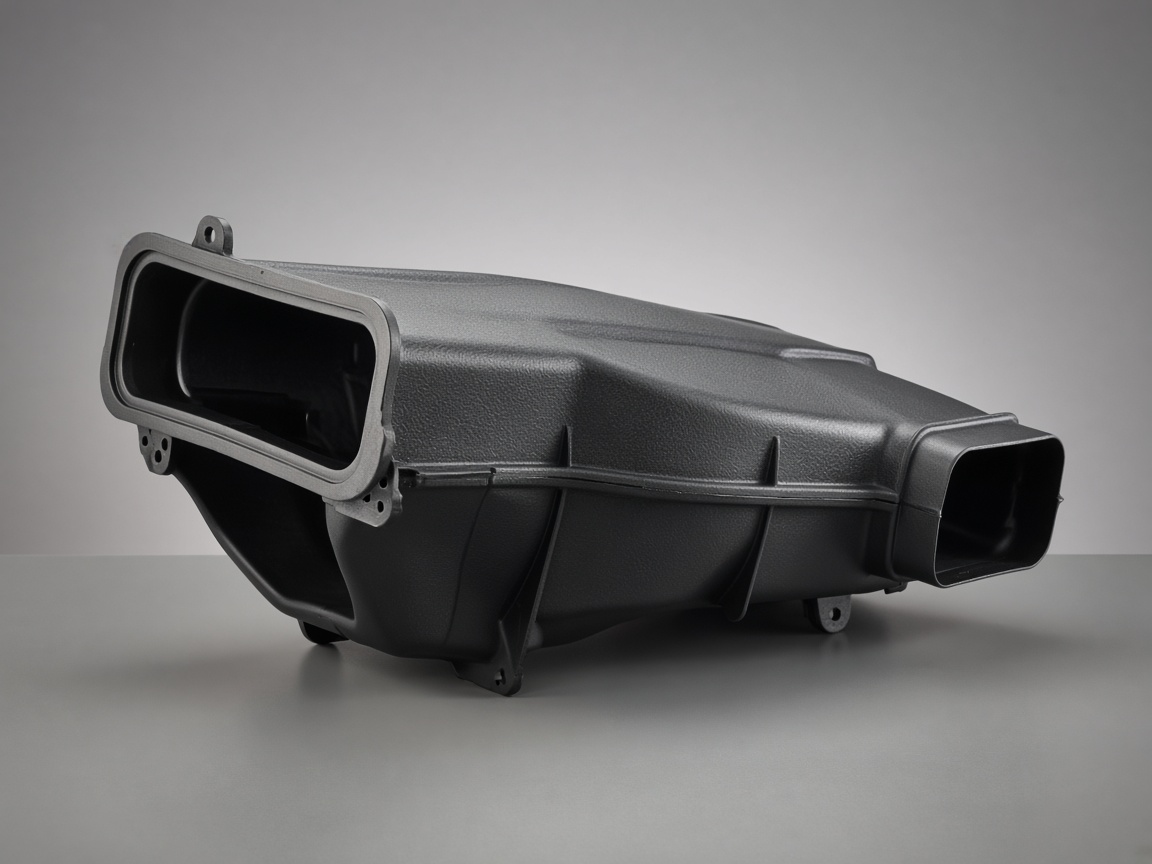
Staying straight is the next issue. A long curved shell cools on the outside of the curve and the inside at different rates, and the part relaxes into a slightly different shape than the drawing. On a duct that has to slip into a fixed opening at both ends, a small bow at the middle turns into a part that will not fit at all.
Ducts are also usually split, because a closed tube with bends cannot be formed by cores that pull straight. Two half shells are molded and then joined, which brings the same problem a manifold has: a long seam that has to seal. Air leaks matter less than a fluid leak, but a leaking duct is noisy and sends air where it is not wanted.
Joints between sections are designed to move. Ducts run between parts that shift with temperature, vibration, and assembly tolerance, so a slip joint with a soft lip or a foam seal lets the sections move without opening a gap. Inside, sharp turns and steps make turbulence, which is heard as rush noise, so the inside surface is kept smooth and the turns gentle.
Features
Filling, fit, and noise are the three constraints.
| Feature | Purpose | Design note |
|---|---|---|
| Long thin shell | Carries the air | Feed points placed to reach both ends |
| Split halves | Allow bends and turns | Joined by welding or by fasteners |
| Slip joint | Absorbs movement between sections | Soft lip or foam so the joint stays closed |
| Smooth inside | Keeps rush noise down | Gentle turns with no steps at the joints |
| Mounting tabs | Holds the duct in place | Slotted so the duct is not forced straight |
Service tiers
Part focus: Long thin fill, slip joints, inside smoothness. Upload CAD with critical fits and environment in notes when not modeled.
| Tier | Environment | What matters most | Typical molded route | Quote path |
|---|---|---|---|---|
| 1 Long thin shell | Air has to reach the far end | Melt cooling in a thin section | More than one feed point | Upload CAD; note the length |
| 2 Split halves | Bends a straight core cannot pull | A seam that has to seal | Welded, or clips and screws | Instant quote; say how the halves join |
| 3 Slip joint | Sections that shift | The joint stays closed while the parts move | Soft lip or foam seal | Instant quote; note the movement |
| 4 Inside path | Rush noise | A smooth inside and gentle turns | No steps where sections meet | Upload CAD; note the noise target |
| 5 Mounting tabs | Holds the duct in place | The duct is not forced straight | Slotted tabs | Instant quote; show both ends |
Materials
One primary family per line item. Put commercial grade, fillers, and environment filters in comments.
| Family | Typical use on this part type | Notes for instant quote |
|---|---|---|
| PP | Long thin shells when the drawing names PP | Field PP |
Filling
The melt cools as it flows, and a long thin path can freeze before the end.
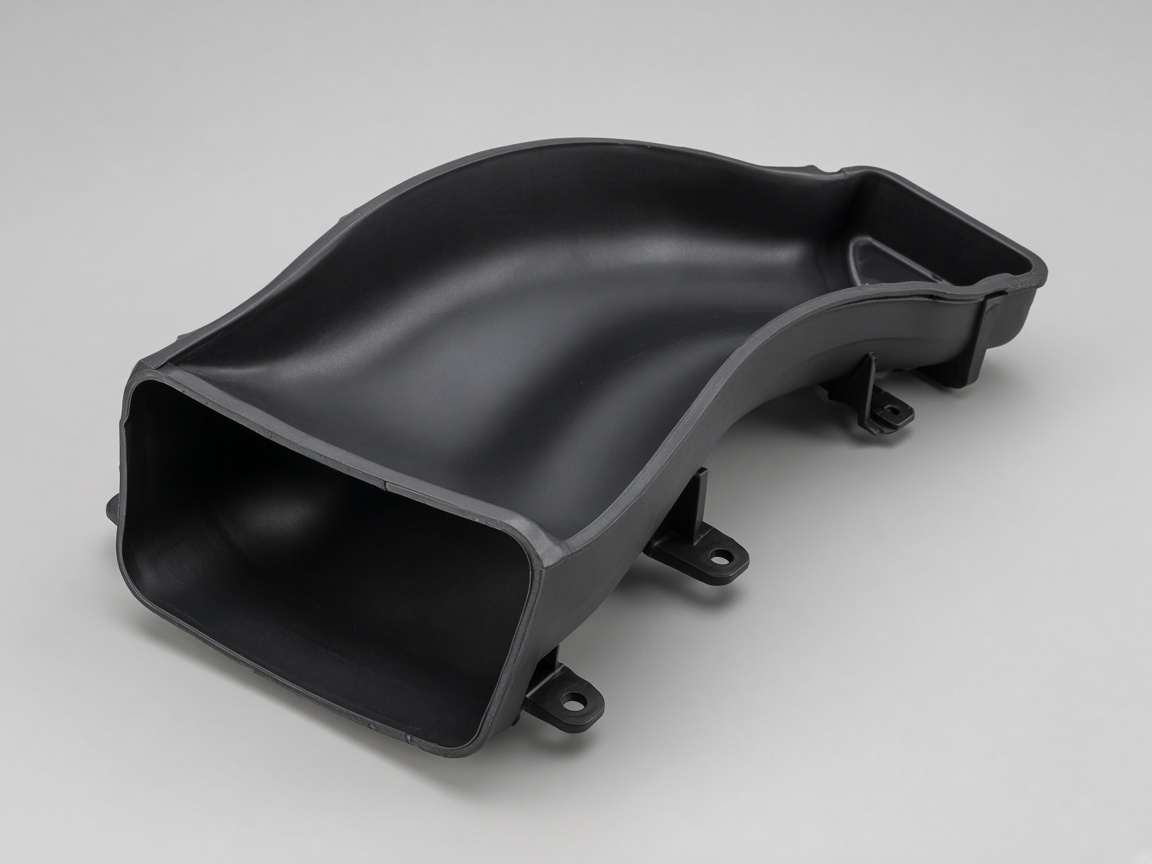
Making the duct
Blow molding makes hollow shapes in one piece. Molding gives precise detail.
Avoid these
Two choices that show up as a short end or a gap that leaks air.
Using one feed point on a long thin shell. The melt cools before it reaches the far end, and the duct comes out short. A second feed point shortens the distance, and it leaves a flow joint where the two fronts meet.
Joining sections with a rigid joint when the parts on either end can shift. Temperature, vibration, and assembly tolerance open a gap. A slip joint with a soft lip or a foam seal keeps the joint closed, and slotted mounting tabs keep the duct from being forced straight.
Drawing
The route and the openings at each end set the shape.
Duct CAD with both end interfaces
Airflow and pressure through the duct
Space available along the route
Movement expected between the parts it joins
Noise target and temperature range
Expected annual volume
Keep reading
Air parts, thin sections, and the shorts that end a long fill.
Vanes and pivots at the outlet.
Air ventsWhat pushes the air along.
Fan bladesSplit construction and welded seams.
ManifoldsFilters in the air path.
Filter housingsWhen the far end does not fill.
Short shotFilling long thin sections.
Thin wall designA common duct resin.
PolypropyleneHow we support industrial programs.
Industrial and transportationEvery part-type guide, grouped by family.
Molded parts libraryFAQ
The melt froze before it arrived. Adding a feed point closer to that end, easing the section, or raising the melt temperature all help, and the first two are usually the durable fix. Checking the fill early, before the tool is cut, shows exactly how far the melt gets and where a second feed point belongs.
A long curved shell usually relaxes a little as it cools. Balanced cooling and a holding fixture reduce the movement, and slotted mounting tabs absorb what is left. A duct that has to reach two fixed openings is usually checked in a fixture that holds both ends at their real positions.
Rush noise comes from turbulence at sharp turns, steps at joints, and edges sticking into the flow. Smoothing the inside and easing the turns is usually enough. Even a small step where two sections meet is enough to be heard once air is moving quickly through it.
Ultrasonic welding for a permanent joint, or clips and screws where the duct has to open. Air joints are more forgiving than fluid joints, but the seam still needs a continuous fit.
Each extra feed point shortens the distance the melt has to travel. The two fronts meet and leave a flow joint. That joint is the trade for getting melt all the way to the far end.
A long curved shell relaxes as it cools, and a small bow at the middle keeps the ends from meeting two fixed openings. Slotted tabs let the duct sit without being forced straight.
Next step
Upload the duct and both end interfaces. DFM feedback covers feed points for a long fill, straightness, joint design, and inside smoothness.