
Ultrasonic welding
- Permanent, sealed joint
- No extra fasteners or cure time
- Parts cannot be opened without damage
Secondary operation
Ultrasonic welding uses high frequency vibration to melt a small joint between two molded parts. The joint fuses in seconds with no adhesive, screws, or cure time.
How it works
Ultrasonic welding is a common way to close housings and join molded halves.
Ultrasonic welding comes down to the energy director, resin fit, and what to send with the RFQ. Ultrasonic welding is a secondary operation on a molding program. Assembly features cover snaps and bosses. Laser welding and solvent bonding are different joints.
A horn presses the parts together and vibrates at ultrasonic frequency. Friction at a small feature called an energy director melts a thin layer of resin, which flows and solidifies into a weld once the vibration stops.
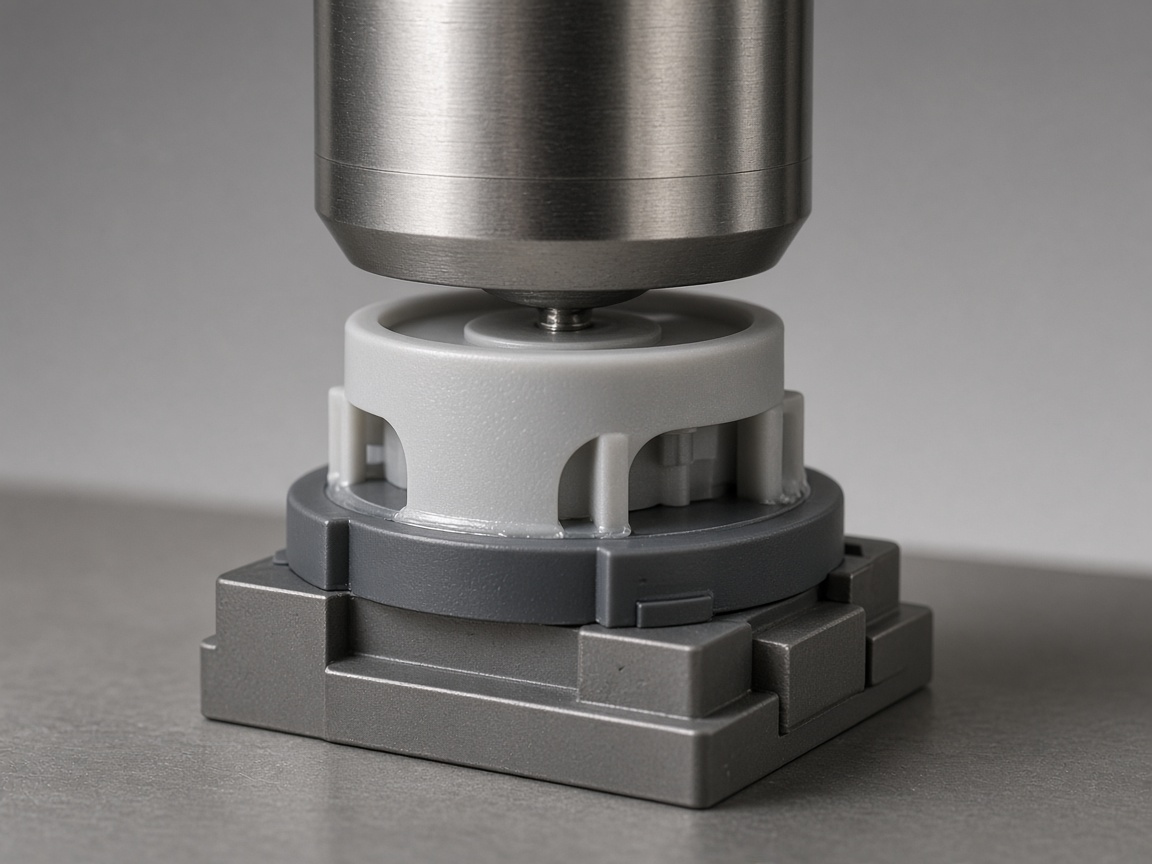
Roles
Ultrasonic welding fuses the joint. Snaps stay on assembly features. Laser welding needs a clear top. Solvent bonding softens the surface.
| Page | Use it for |
|---|---|
| Ultrasonic welding (this page) | Energy director, resin fit, and the RFQ notes |
| Secondary operations | Welding scoped with the molding program |
| Assembly features | Snaps, bosses, and other molded joints |
| Laser welding | Joining through a clear top part |
| Solvent bonding | Joining by softening the surface |
| All processes | The rest of the process index |
Fit check
Qualitative guidance. Confirm the joint design before the tool is built.
| Factor | Tends to weld well | Needs a closer look |
|---|---|---|
| Resin family | Amorphous resins such as ABS and polycarbonate | Semi-crystalline resins such as nylon and acetal |
| Resin pairing | Same resin on both parts | Dissimilar resins |
| Joint | Energy director or shear joint designed in | Flat faces with no joint feature |
| Moisture | Dried, stable parts | Hygroscopic resins that absorb water |
Design notes
Weld quality is decided when the parts are designed, not at the welder.
Add an energy director or shear joint on the mating edge
Keep the horn contact face flat and close to the joint
Leave space around the joint for flash, or add a flash trap
Keep fragile features and electronics away from the joint area
Side by side
Both avoid adhesives. Serviceability usually decides.
Continue exploring
Sibling processes and supporting references.
All specialty processes and secondary operations.
All processesInk transferred by a silicone pad onto curved and recessed surfaces.
Pad printingHeated die and foil for metallic or solid color marks.
Hot stampingCommon operations done after molding.
Secondary operationsChoosing a joint for molded halves.
Ultrasonic welding vs adhesiveLocators, snaps, and joints designed into the part.
Assembly featuresFAQ
It can, when the joint is designed for sealing and the resins weld well. State sealing requirements up front so the joint is designed for them.
CAD for both parts, the resin for each, and any sealing or strength requirement.
A small ridge molded into the joint. The horn vibrates there, so the heat stays at that ridge instead of melting the whole part.
The same family welds more readily. Name both resins on the RFQ. Dissimilar resins need a joint review before steel is cut.
Adhesive adds a bond line and a cure step. Ultrasonic welding fuses the plastic at the joint. If the resins will not weld, review another joint.
Laser welding joins through a clear top part. Ultrasonic welding needs the horn on the joint. The part design is not the same.
Next step
This step can be scoped with the molding RFQ. Upload CAD for an instant quote.