
In mold labeling
- No separate decorating step once the cell is running
- Photo quality artwork over most of the surface
- Needs label handling automation and a mold built for it
- An artwork change means a new label run, not new steel
Process guide
Pick up a margarine tub or a paint pail and try to peel the label. Usually you cannot, because it is not stuck on. It was placed in the mold before the plastic arrived, and the two came out as one wall.
What it is
Decoration and molding happen in the same cycle, so there is no labeling line after the press.
In mold labeling fuses a printed film to the part inside the mold. In mold decorating uses a decorated film for graphics on a housing. Pad printing and hot stamping mark the part after it is molded. Containers covers the tub or lid itself.
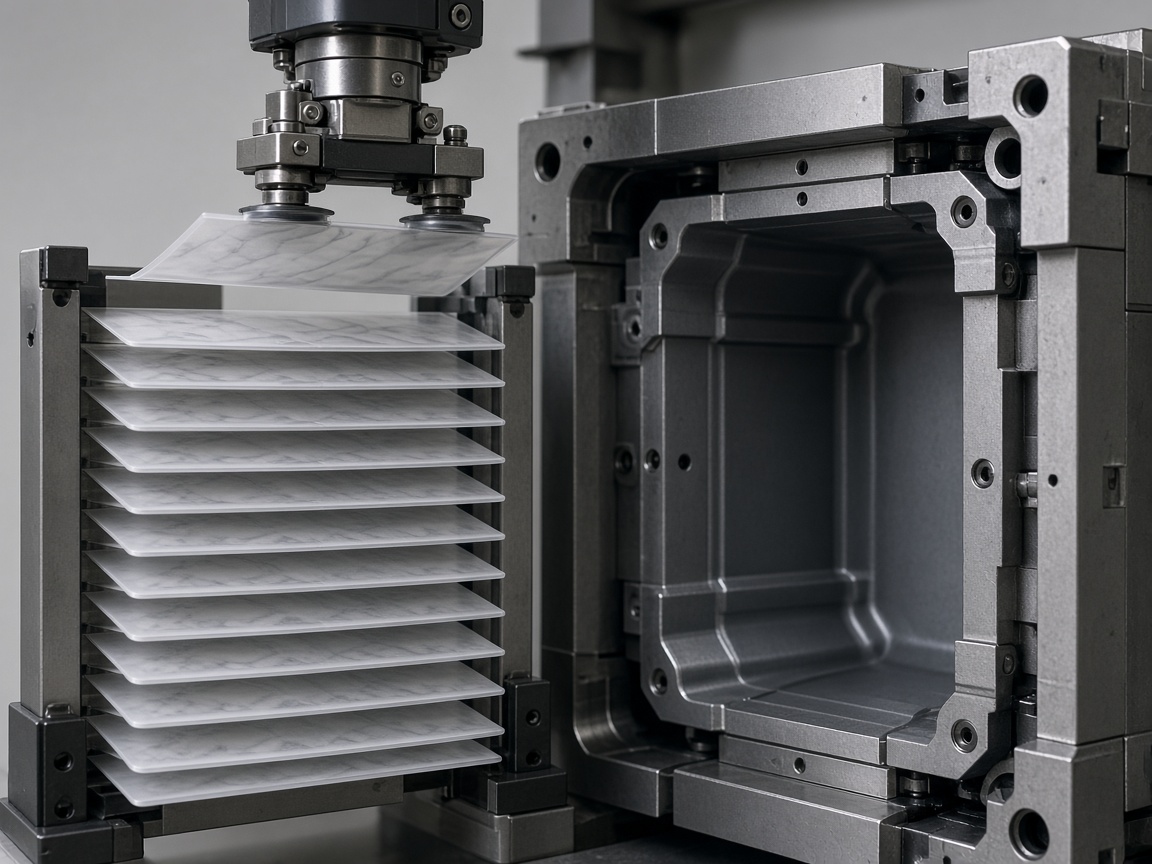
Also called in-mold labeling (IML), in-mold decorating, or mold-in-place labeling. The label sits in the cavity before the resin flows, and the melt fuses with its backside during filling. No post-mold decal, no adhesive failure. An IML label is a thin printed film, usually cut to shape in advance. A robot takes one from a magazine, carries it into the open mold, and holds it against the cavity wall with vacuum or a static charge. The mold closes, hot resin flows in behind the label, and the back of the label melts into the surface of the part. The print sits on the outside, protected by the film it was printed on.
Almost all of it happens in packaging: thin wall tubs, lids, pails, and cups made in large volumes on fast presses. The label can cover most of the outside, stands up to fridges and dishwashers, and does not lift at the edges. Because the label material is normally chosen to match the container, a PP label on a PP tub, the finished pack can go into recycling as one material.
IML needs an automated label handling system, usually a robot with vacuum pickup or a magazine-fed shuttle, that places each label before the mold closes. Static eliminators and ionization bars help with placement. The mold may use vacuum grooves or electrostatic pads to hold the film flat during injection. Cycle time often adds about one to three seconds per shot versus a plain molding cycle, depending on label size and handling speed.
Common fits include home appliance panels (washer lids, AC controls) where graphics must resist scratches and never peel; power tool housings that see oil and drops; food containers and lids when label and container share one resin for recycling; outdoor equipment where UV-stable ink sits behind the film; and medical device housings that need cleanable surfaces without adhesive residue.
Roles
IML fuses a film during the shot. IMD is a decorated film on a housing. Pad printing and hot stamping happen after molding.
| Page | Use it for |
|---|---|
| In mold labeling (this page) | A printed film that becomes the wall |
| In mold decorating | Graphics from a film on a housing |
| Pad printing | Ink transferred after molding |
| Hot stamping | Foil pressed after molding |
| Containers | The tub, cup, or lid the label sits on |
The label's path
Most IML trouble starts before the mold closes. Post-mold finishing options are covered under secondary operations.
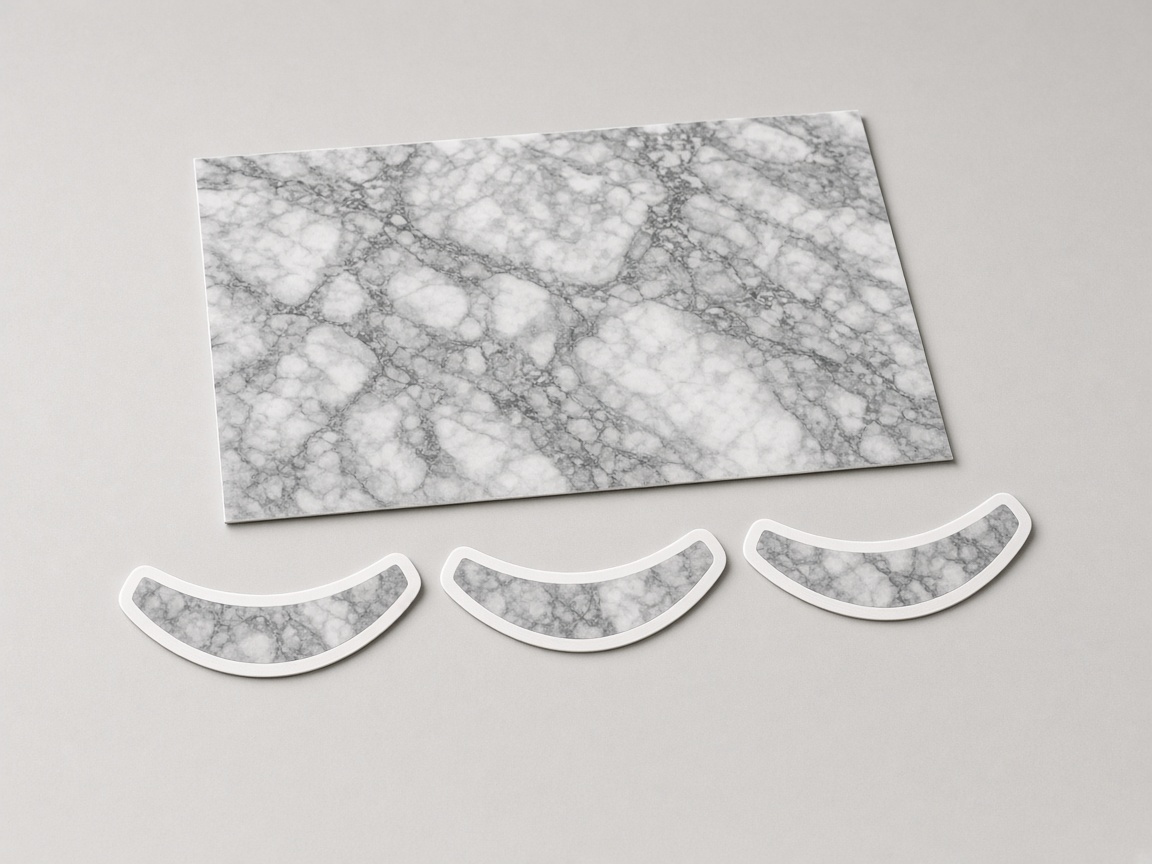
Labels are printed in sheets or on rolls and cut to the flat shape of the surface they will cover. A wrap label for a tapered tub is cut as a curved band, not a rectangle.
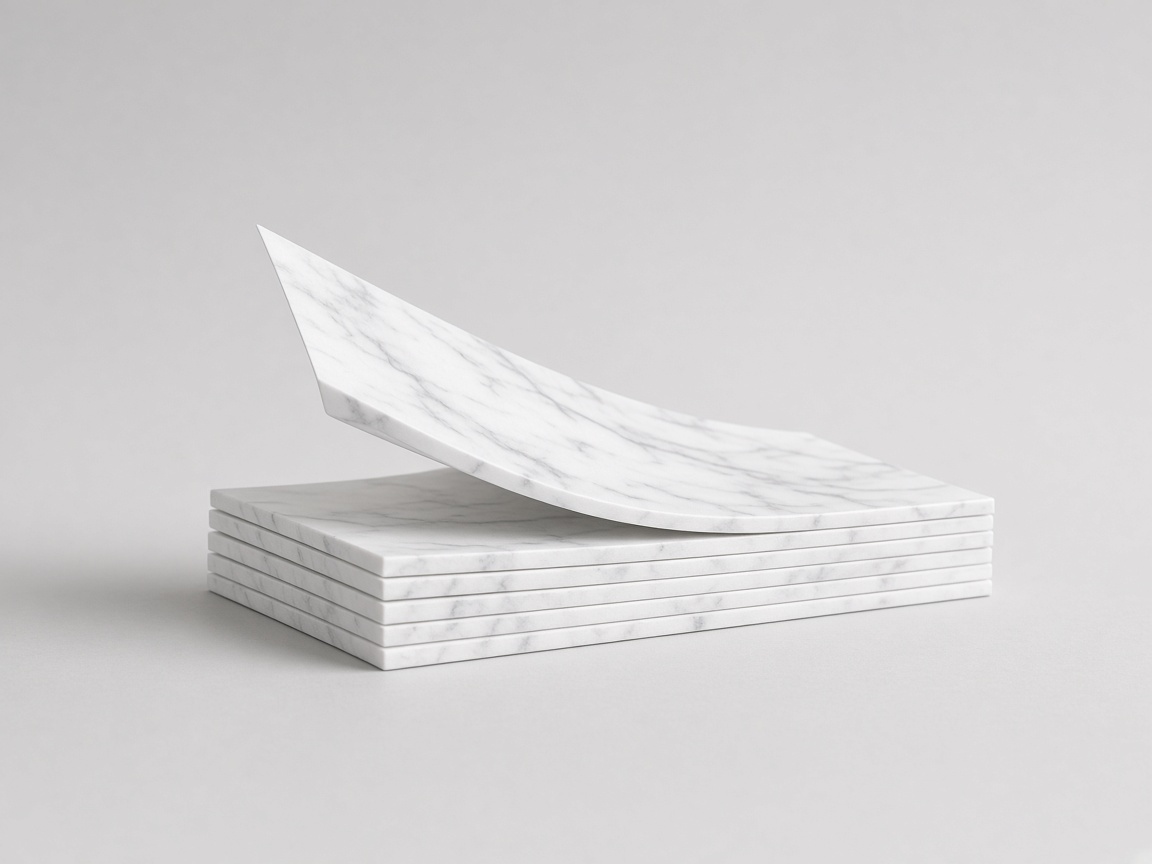
Cut labels sit in a magazine. Picking one at a time, never two stuck together, is a real design problem for the automation.
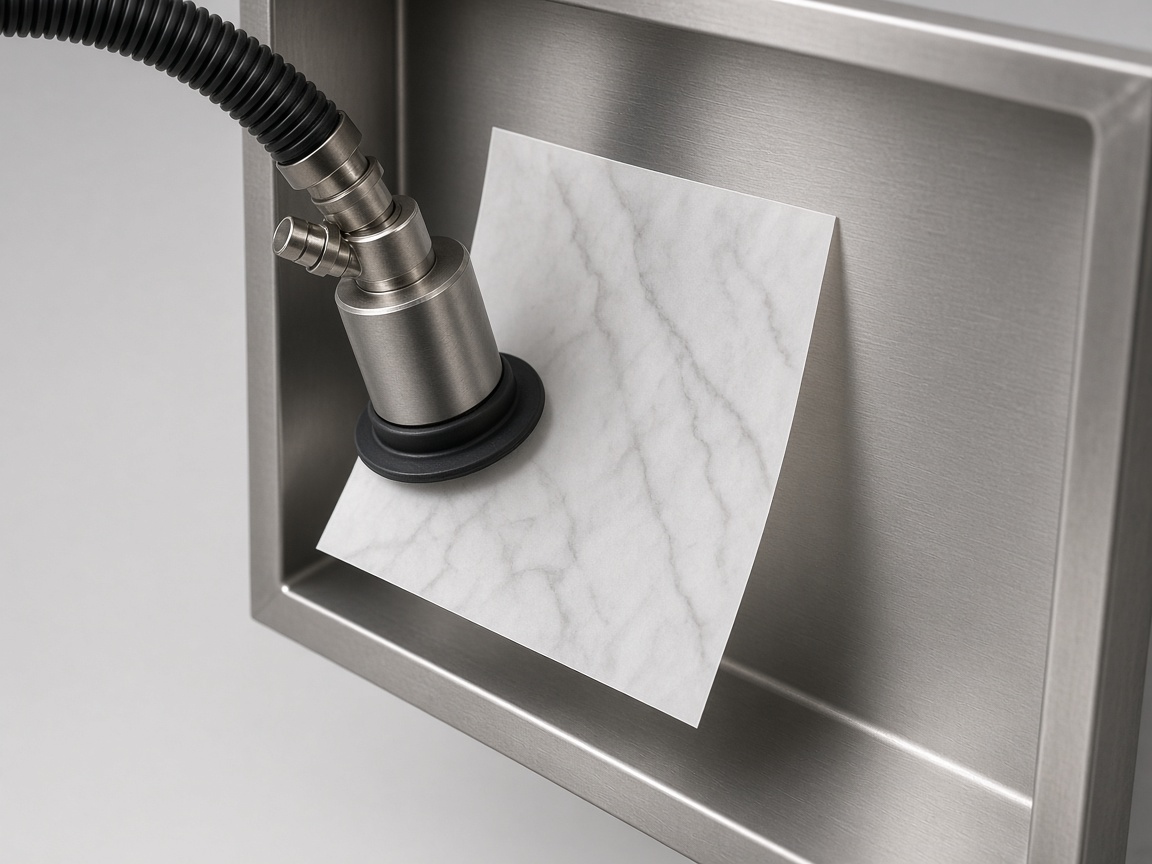
The robot places the label on a mandrel or straight into the cavity. Vacuum ports or an electrostatic charge hold it while the mold closes. Production cells rely on repeatable pickup, not manual placement.
Resin fills behind the label and fuses to its back. The part leaves the mold decorated and goes straight to stacking.
Label shapes
A label is a flat sheet. It can wrap a cone or a cylinder, but it cannot stretch over a dome.
| Placement | Typical part | What to watch |
|---|---|---|
| Lid top | Flat or gently curved lids | The simplest case. Keep the label clear of the snap bead and the gate |
| Side band | Round or oval tubs and cups | Ends meet or overlap at a seam; the taper of the wall sets the curve of the cut label |
| Four side wrap | Square and rectangular containers | Corners need a generous radius or the label creases where it folds |
| Bottom and side | Containers that need a barrier or full coverage | Several labels or a folded blank; placement tolerance tightens at every joint |
Alternatives
IML does not suit every decorated container. The volume and the artwork usually make the call.
Fit
IML does not suit very low volumes, complex 3D contours, or parts that need a functional coating after molding. A flat film wrinkles on a dome. A short run, or a coating that has to go on after the shot, is usually a molded part plus pad printing or painting .
Quick compare
Engineers often choose between in-mold labeling and post-mold decoration. Use this as a first filter before you commit to tooling.
| Process | Durability | When it runs | Color / artwork | Typical volume | Cost shape |
|---|---|---|---|---|---|
| IML | High (fused, no lifted edge) | Inside the mold | Full color, gradients, metallic effects | Mid to high volume | Label and automation upfront; low per part |
| Pad printing | Medium (surface ink) | After molding | One or few colors, simple graphics | Low to mid volume | Low start; cost rises with color count |
| Heat transfer | Mid to high (film bond) | After molding | Full color | Mid volume | Film plus labor; improves with scale |
| Direct printing (UV / screen) | Medium (surface coating) | After molding | Depends on print method | Mid volume | Equipment amortizes; per part can stay stable |
IML DFM
Review these with your mold and label supplier before you freeze the cavity. Pair with the injection molding DFM guide for general part rules.
Label film matches the substrate resin family (for example PP label on PP) when you need true fusion
Label thickness is part of the wall. The cavity has to allow for the film, and the thickness comes from the film supplier.
Gate location avoids direct impingement on the label edge to limit wash-off or wrinkling
Label bend radius meets the film supplier minimum; sharp bends risk bridging or air traps
Draft on label-covered surfaces still clears the mold after the label is in place
Static control or vacuum retention is specified so the label stays flat until the mold closes
Registration is defined for seams and edges. Placement tolerance is confirmed during DFM review for your label and part.
Sink or gloss mismatch behind thick label areas is anticipated; ribs or core-outs compensate
Design checks
These come up in almost every IML review.
Every labeled surface can be unrolled flat: cylinders and cones yes, spheres and domes no
The label material matches the container resin, or you know why it does not
The gate faces the label's back or sits outside the label area, so hot resin does not wash out the print
Artwork leaves room for placement tolerance at seams and edges
Volume is high enough to justify automation and label stock
Keep reading
Other ways to decorate a molded part, and the parts IML is usually used on.
Foil transfer and formed films for durable parts.
In mold decoratingInk transferred onto a molded part by a silicone pad.
Pad printingHeat and pressure for foil marks and metallic trim.
Hot stampingSnap beads, hinges, and flat decorated tops.
LidsWalls, stacking, and draft on molded containers.
ContainersWhere resin enters, and what it does on the way.
Gate locationPrinting, marking, and assembly after molding.
Secondary operationsEvery molding process and secondary operation.
All processesPost-mold decorating and finishing when IML is not the fit.
Secondary operationsGeneral DFM rules that still apply to labeled parts.
Injection molding DFMResin grades and label compatibility starting points.
Injection molding materialsUpload CAD for DFM feedback on decorated parts.
Instant quote platformRegistration and quality expectations for production parts.
Manufacturing standardsFAQ
No. A sticker uses adhesive and sits on the surface. An IML film has no adhesive. Its back fuses to the resin during the shot, so there is no edge to lift.
A gentle curve in one direction can work. A dome curves two ways at once. A flat film wrinkles there instead of stretching.
A label in the same resin family as the container is the usual path, such as a polypropylene film on a polypropylene tub. A different family is a different question for the recycler.
Resin leaves the gate hot and fast. Aimed at the printed face, it can smear the ink or shove the film. Gating through the base, or from the side without the film, is the usual fix.
The film needs a smooth face to fuse. Grain on the show face belongs in the film, not in the steel under it.
No. Placing the film adds a motion inside the open mold. How long that takes, and the smallest film the handler can place, belong to the press setup and are confirmed in DFM.
Next step
Upload CAD for DFM review and an instant quote on the injection molded part.