
Co injection
- Materials stack through the thickness of the wall.
- The skin covers both faces, so the core never shows when things go right.
- Often a conventional mold on a specialized press.
Process guide
Two shot puts materials side by side. Co injection puts one inside the other. The skin you see and touch is one resin, and the core underneath can be recycled, foamed, or filled material that would never pass as a show surface.
How it works
Also called sandwich molding. The layers form because plastic freezes from the outside in.
Co-injection fills a skin and a core through the same gate. Two shot molding and multi shot molding place materials side by side. Gas assist hollows a thick section instead of filling it with a second resin. Gate location decides where the core can break through.
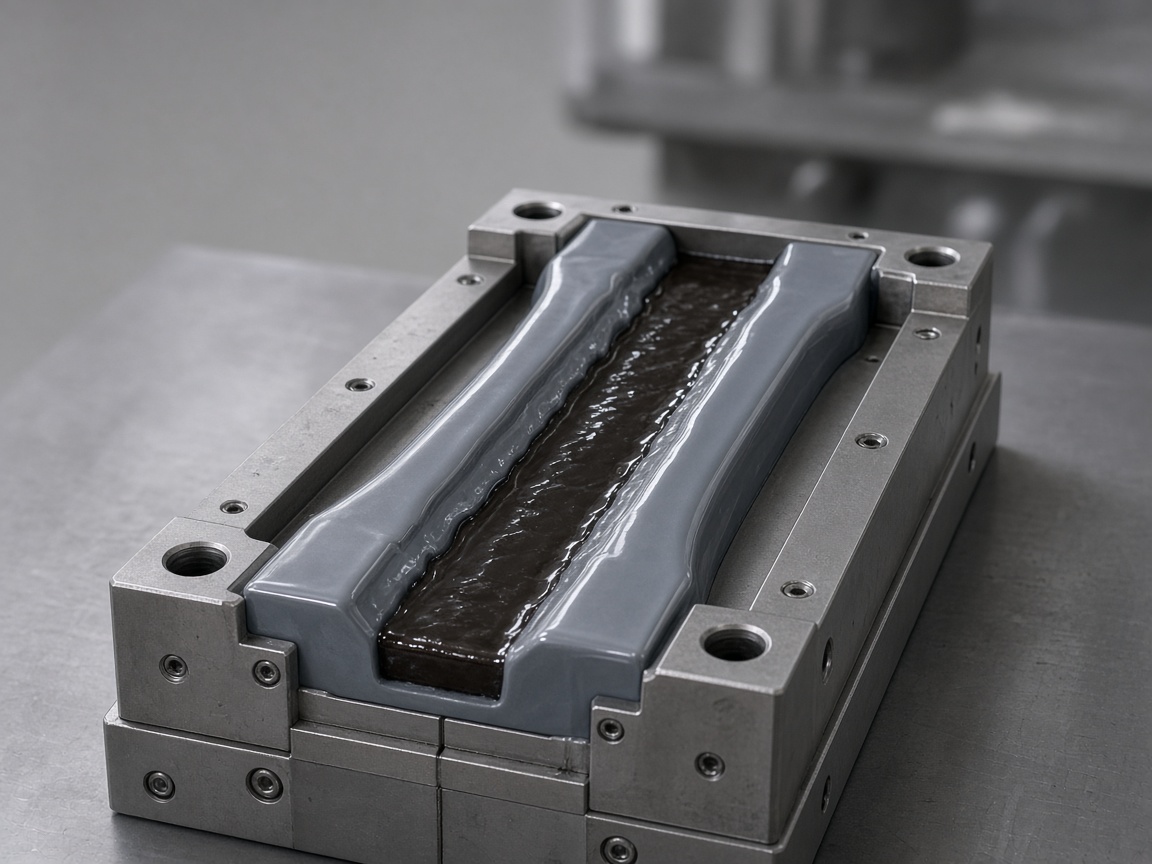
Skin material goes in first. As it flows, it freezes against the cold steel, so what keeps moving is a molten channel down the middle. The core material follows through the same gate, pushes into that channel, and spreads out behind the flow front. A short last shot of skin material closes off the gate. Cut the finished part in half and you see the same resin on both faces with something else sandwiched between them.
The press does the unusual work here. It needs two injection units feeding one nozzle that can switch between them, or run both at a set ratio. The mold can be close to an ordinary single material tool. That is the reverse of two shot, where the tool carries most of the complexity.
You find it where a part needs a good surface but most of its volume could be something else: crates and pallets with recycled content hidden inside, housings with a stiff filled core under an unfilled skin, and thick parts with a foamed core to keep the surface from sinking.
Roles
Co-injection stacks a skin over a core. Two shot places materials side by side. Gas assist hollows the thick section.
| Page | Use it for |
|---|---|
| Co-injection (this page) | Skin and core through one gate |
| Two shot molding | Two materials side by side |
| Multi shot molding | A third material and another station |
| Gas assist | A hollow channel, not a second resin |
| Gate location | Where the core can break out |
Not two shot
Both processes use two injection units. Where the second material ends up is completely different.
Pairings
General industry practice. Skin and core usually come from the same resin family so the layers stay bonded.
| Skin | Core | Reason |
|---|---|---|
| Virgin resin in the part color | Recycled or regrind of the same resin | Recycled content goes where nobody sees it, and the face keeps its color |
| Unfilled grade | Glass filled grade of the same family | Stiffness from the core without glass fibers showing on the surface |
| Solid resin | Foamed version of the same resin | Less weight and less sink on thick sections, with a solid skin outside |
| PET | A barrier resin such as EVOH | Layered preforms and containers where the middle layer slows oxygen getting through |
Failure modes
Most co injection trouble comes down to where the layer boundary ends up. Sectioned sample parts are the only reliable way to see it.

Is it worth it
Co-injection only pays when the core is a large share of volume and does work the skin cannot. These limits matter as much as the savings story.
It earns its place when the core material is much less expensive than the skin, or more useful, and makes up most of the part's volume. Hiding recycled content under a colored face is the most common reason today. Small, thin parts leave little room for a core, and the extra process control buys very little.
The process window is also narrow. Skin to core ratio, injection speed, and the switch point all move the layer boundary. Expect more sampling than for a single material part, and ask whoever runs it how they check layer distribution. The honest answer usually involves a saw and a stack of cut parts.
Before you quote co-injection, scan the part for the constraints below. They are the usual reasons sampling runs long or the process never pays back.
Usually not worth it
Treat these as stop signs before you commit tooling and resin trials to a sandwich build.
Wall thickness under about 1.5 mm leaves too little room to control skin and core placement
Small parts at low volume rarely amortize the specialized equipment and extra sampling
Two resins from different families with no tie layer: high delamination risk at the interface
Soft touch on one face only: overmolding or two-shot molding is usually the faster path
Keep reading
Sibling multi material processes, the resins that go into cores, and the defects that show up when layers misbehave.
Two materials side by side, molded in one cycle.
Two shot moldingThree or more materials in one tool.
Multi shot moldingRecycled resin behavior and where it fits.
Recycled PET (rPET)What glass adds to stiffness, and what it does to the surface.
Glass filled vs unfilledWhy molded layers peel apart and how to stop it.
DelaminationThe thick section problem a foamed core is often used to hide.
Sink marksMolded tubs and jars, and where their walls get thin.
ContainersEvery molding process and secondary operation.
All processesFAQ
Yes. Sandwich molding is the older name for the same process. You will also see it written as coinjection or skin and core molding.
It can, but layers that do not bond can separate under load or impact. Most production parts pair a skin and a core from the same family for that reason.
Cut sample parts at several points along the flow path and look at the layers. Surface inspection only tells you about breakthrough after it has already happened.
Core out thick sections, add ribs for stiffness instead of mass, and blend recycled content into the resin where the color allows it. A design review will show which of those fits the part.
Two shot places materials next to each other. Co-injection stacks a skin over a core through the same gate.
Upload CAD for DFM review and an instant quote. A standard single material mold is the right choice when one resin can do the job.
Next step
Upload CAD for DFM review and an instant quote on the injection molded part.