Skip to content
NetProto

Soft tooling

Soft Tooling for Injection Molding: Where the Wear Shows Up

A soft tool is cut from material that machines quickly and wears quickly. The trade is invisible on the first parts and obvious later in the run.

What soft means

Soft tooling trades hardness for cutting speed

Soft tooling is a mold cut from unhardened steel or aluminum rather than hardened tool steel. It is easier to machine, and that is the whole appeal.

Hardness is also what lets a mold hold a sharp parting line, a clean gate, and a consistent texture shot after shot. Without it the tool starts changing from the first cycle, slowly at first and then in ways you can see on the part.

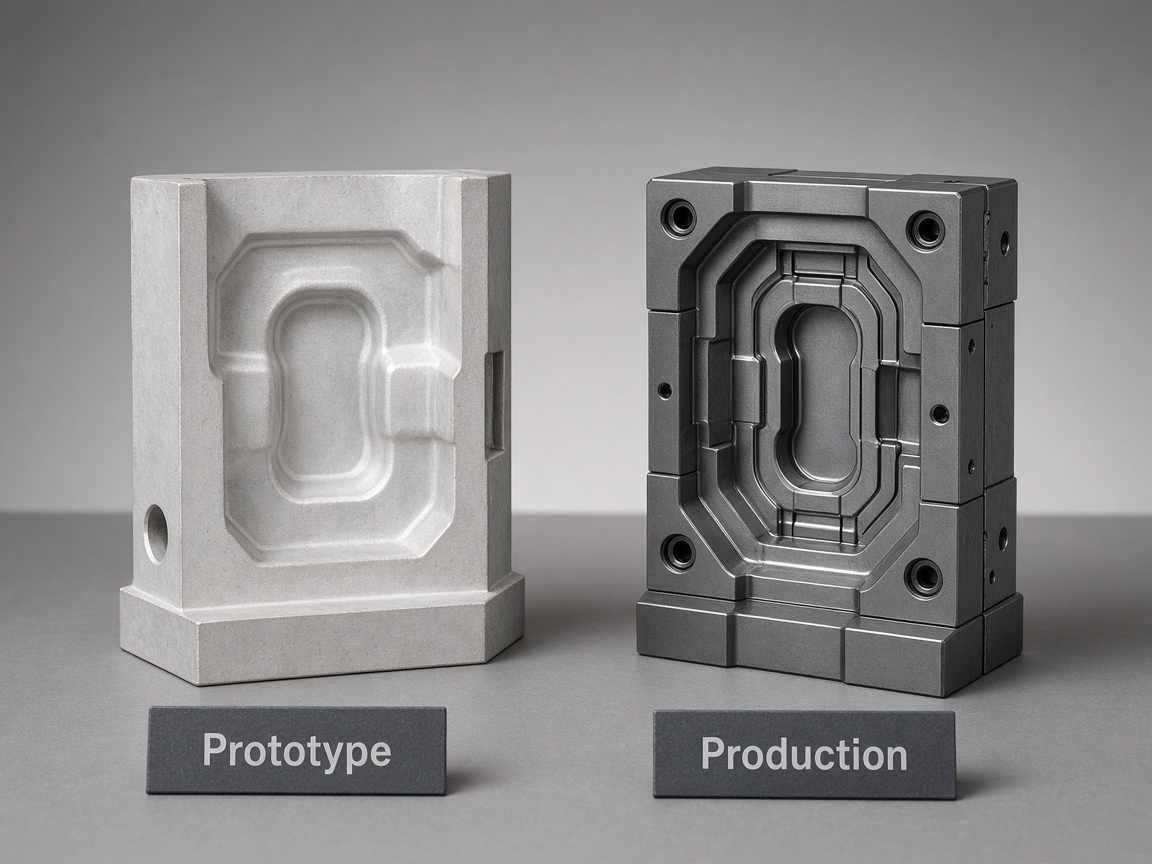
Soft tooling is often compared with one hardened steel tool. Every program here runs on that steel tool, and this page explains how wear shows up on a softer cavity.

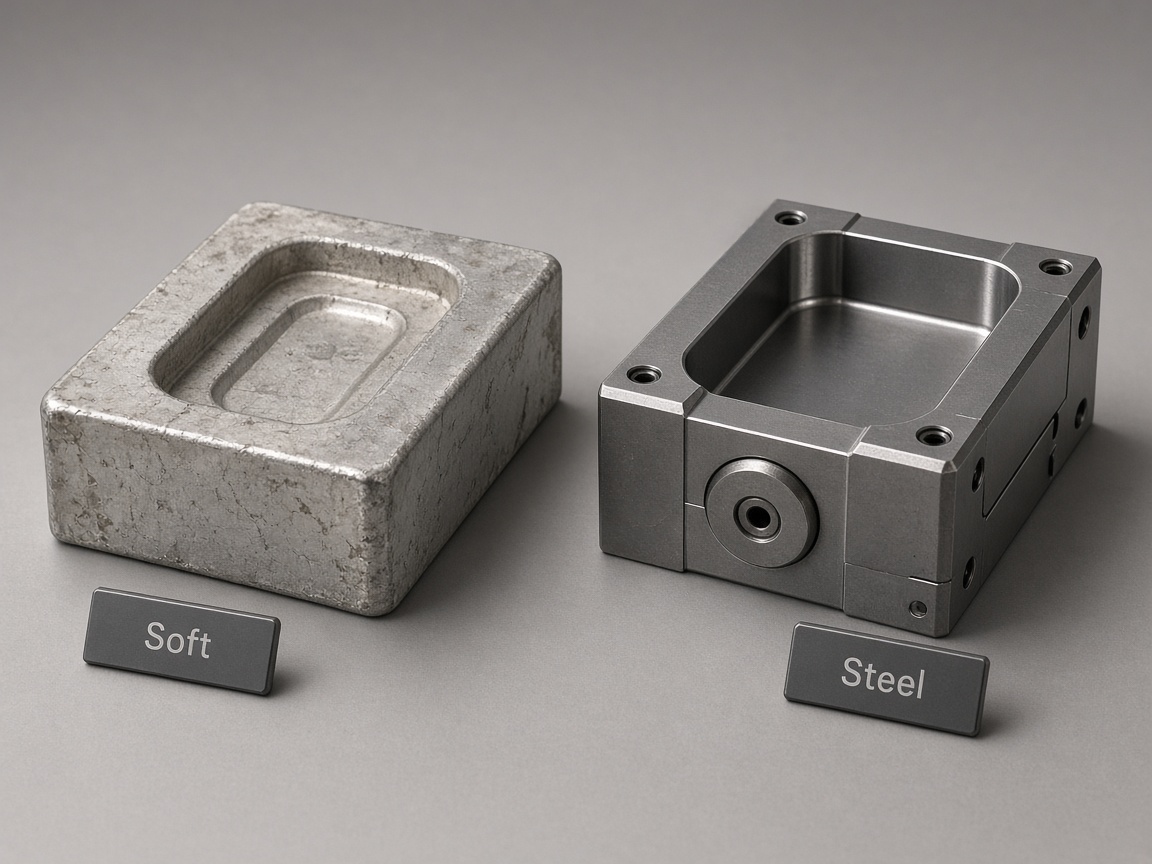
Cavity block marked Soft beside a hardened steel mold

Wear symptoms

Where tool wear shows up on the part

Each symptom links to a troubleshooting guide for the defect it produces.

SymptomWhat is happening in the toolWhat you see on the part
Flash at the parting lineMating surfaces lose their sharp shutoffThin excess plastic that needs trimming or causes rejects
Dimensional driftCavity and gate areas erode unevenlyParts that passed first article move toward the edge of tolerance
Cosmetic changePolish and texture wear down in high flow areasGloss or grain that no longer matches the approved sample
Drag marks and stickingDraft surfaces scuff and lose their finishParts that eject harder and show scrape lines
Faster wear with filled resinsGlass and mineral fillers act as an abrasiveEvery symptom above arrives sooner in the run

Over the program

A soft tool versus hardened steel, shot after shot

The first parts from either tool can look the same. The difference is what happens next.

Hardened steel tool

  • Holds shutoffs, gates, and texture across the run.
  • Typical output is 100,000+ parts from the same tool.
  • Stands up to glass filled and other abrasive resins.
  • Keeps running for reorders without the tooling charge being billed again.

Soft tool

  • Machines faster, so the tool is quicker to cut.
  • Wear starts at the first cycle and accumulates with every shot.
  • Abrasive resins shorten its useful life further.
  • Once wear outpaces maintenance, the program needs a new tool.

Warning signs

Signs a program has outgrown its soft tool

If a part is already running on a soft tool elsewhere, these are the usual signals.

  • Flash is appearing where it was absent on first article parts.

  • Critical dimensions are drifting toward the limits of their tolerance band.

  • Cosmetic surfaces no longer match the approved sample.

  • Maintenance stops are getting more frequent between runs.

  • Annual volume has grown past what the tool was planned for.

Moving to steel

Moving a program onto hardened steel

If a part is running on a worn soft tool from another supplier, the part CAD is the starting point. NetProto reviews it for DFM and builds one hardened steel tool that you own.

  • DFM review of the existing design before steel is cut
  • Tool completed in 10 business days on qualified programs
  • You own the mold once the tooling charge is paid
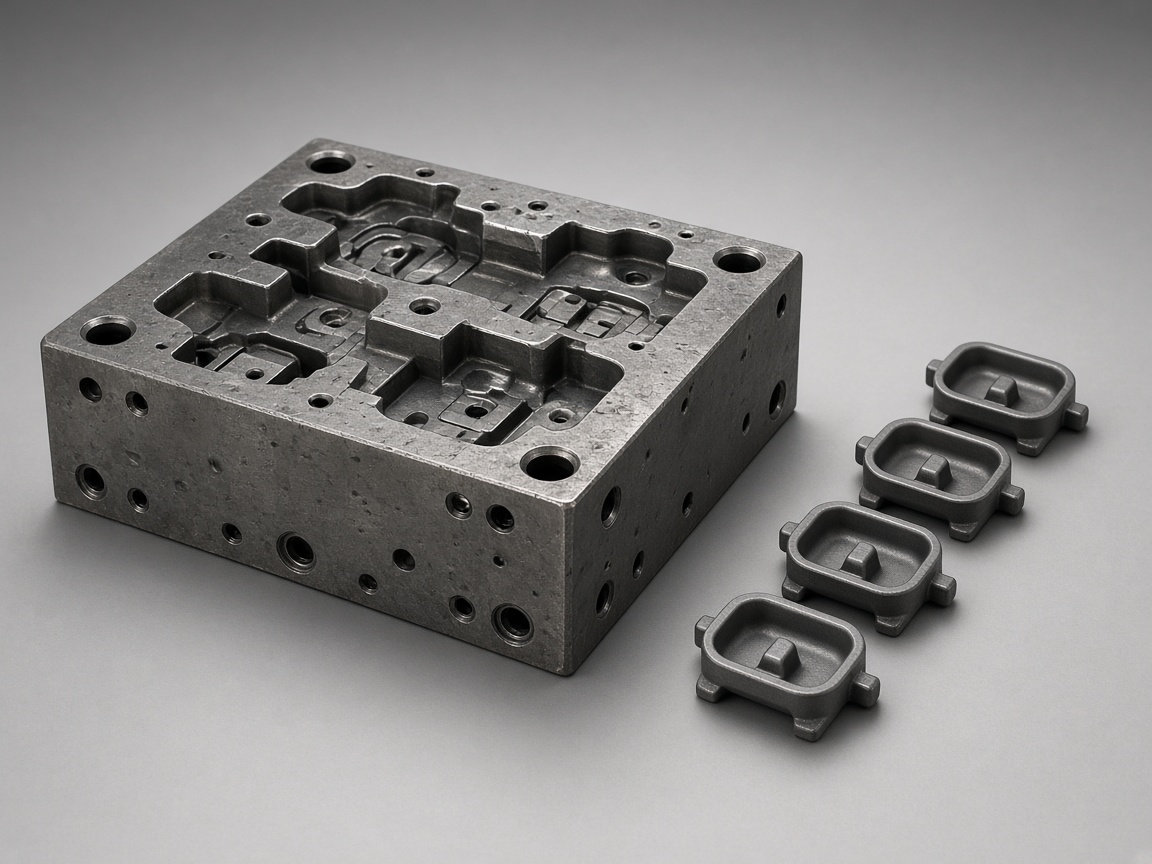
Hardened steel mold with molded parts beside the cavity

Related guides

Diagnose and prevent wear

Defect guides for the symptoms above, plus the tooling pages next to this one.

Gray molded housing with a thin flash line along the parting line

Flash

Why excess plastic escapes at the parting line and how to stop it.

Flash

Glass filled nylon

An abrasive resin that makes tool hardness matter most.

Glass filled nylon
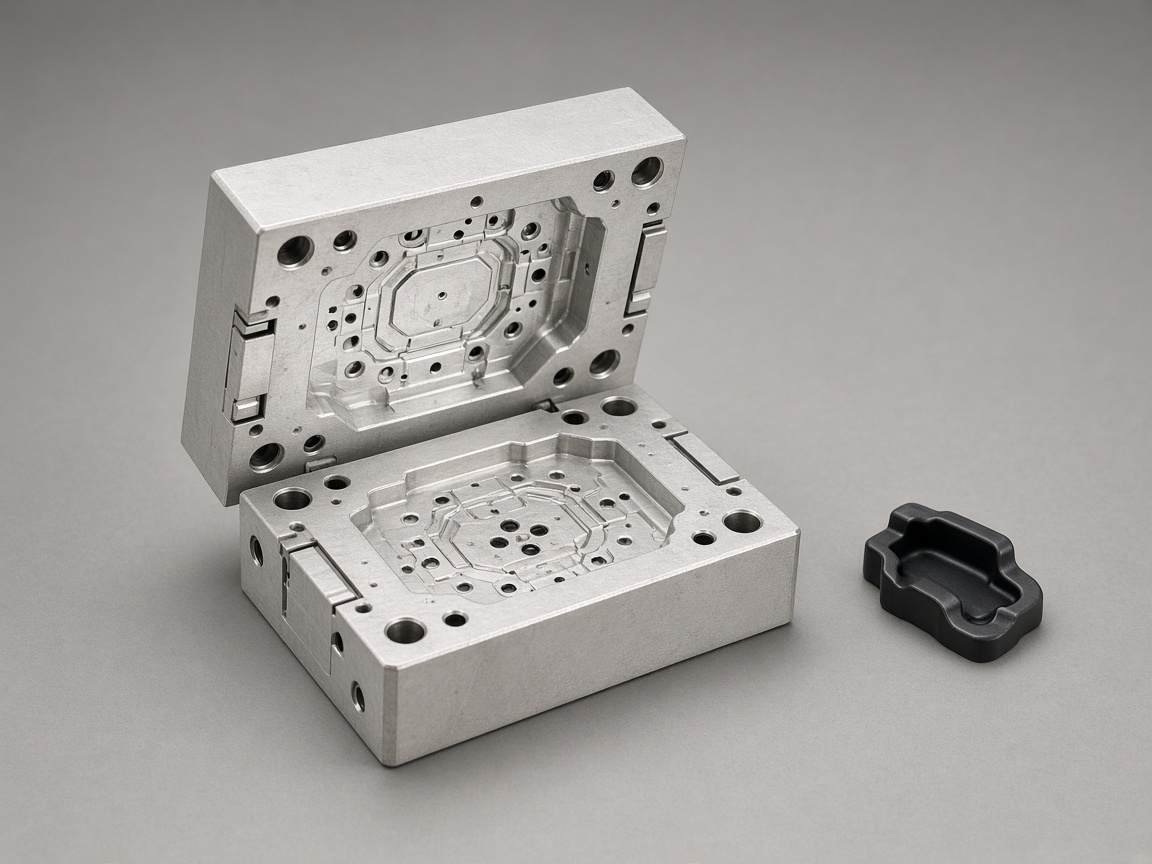
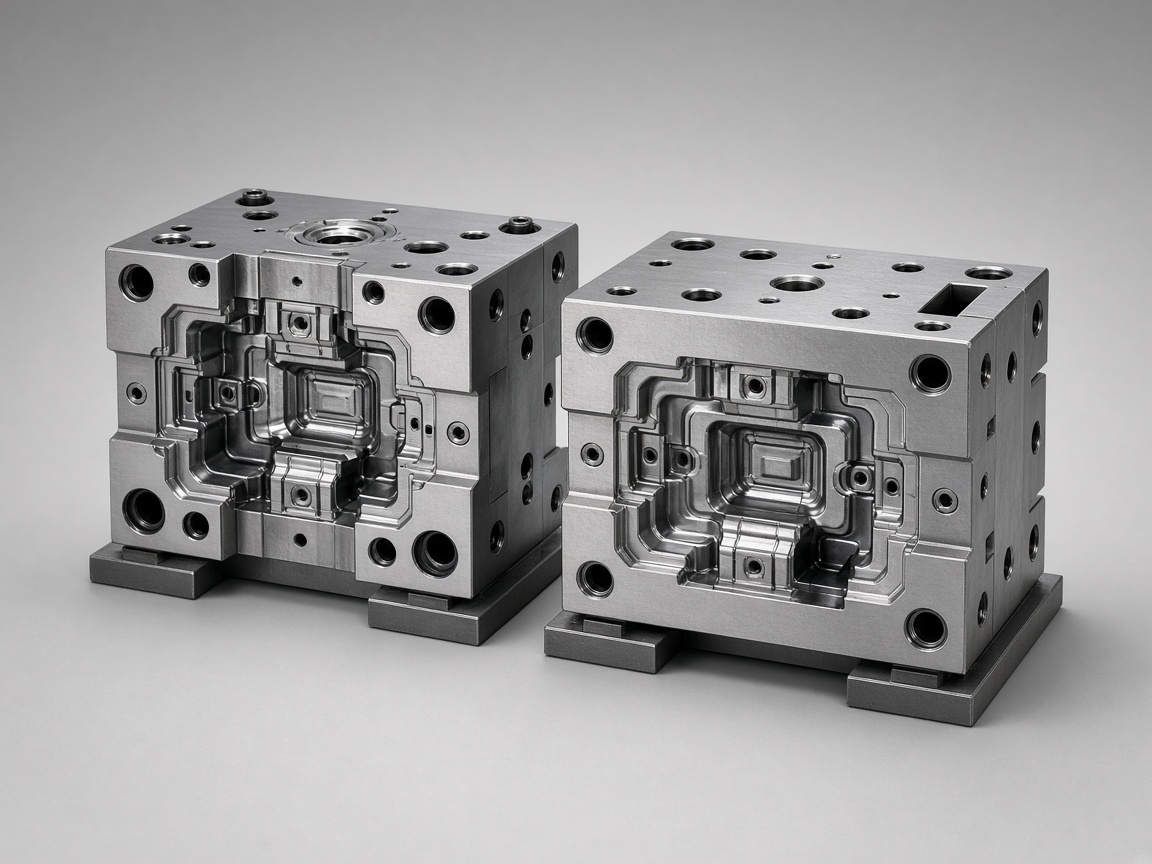
Two hardened steel injection mold halves

Hardened steel tool

This is the hardened steel tool a softer cavity is compared with.

Steel injection mold
Steel mold beside a stack of identical molded parts

When volume outgrows the softer cavity

Soft tooling is often compared with one hardened steel tool when the planned volume is outgrown.

Low volume injection molding

FAQ

Soft tooling questions

Does soft tooling save money over hardened steel?

The soft tool itself can be less costly to cut. Across a full program, steel tooling from NetProto is often priced competitively with US-made aluminum tooling, and it lasts far longer than a soft tool.

How many parts will a softer cavity produce?

Part count for a softer cavity depends on the resin and the geometry, and it is not published here. A hardened steel tool from NetProto typically reaches over 100,000 parts. Treat that figure as typical.

Does ordering again include free wear repairs?

The same tool keeps running while you keep ordering, and the tooling charge is not billed again. Maintenance and wear parts are quoted separately.

What if my resin is glass filled?

Filled resins are abrasive, which is one of the strongest reasons to run them on a hardened steel tool. The glass filled nylon guide covers the material side.

Next step

Replace wear with a tool built once

Upload your CAD for DFM feedback and an instant quote on a hardened steel tool. NetProto manufacturing is ISO 9001 certified.