
Structural foam
- Thick wall does the stiffening; fewer ribs to design and fill
- Low cavity pressure, so large parts fit smaller presses
- Long cooling, because foam insulates the core
- Swirled surface that usually needs paint or heavy texture
Process guide
Machine covers, pallets, and kiosk housings often have walls far thicker than normal molding likes. Structural foam handles that thickness by letting gas bubbles fill the middle of the wall, and it does it at low pressure.
How it works
The press injects less resin than the cavity needs. Gas in the melt does the rest.
Structural foam molding makes a thick part with a solid skin and a foamed core. MuCell disperses much finer cells. Gas assist hollows one channel. Rib design is how a solid molding gets stiff without foam.
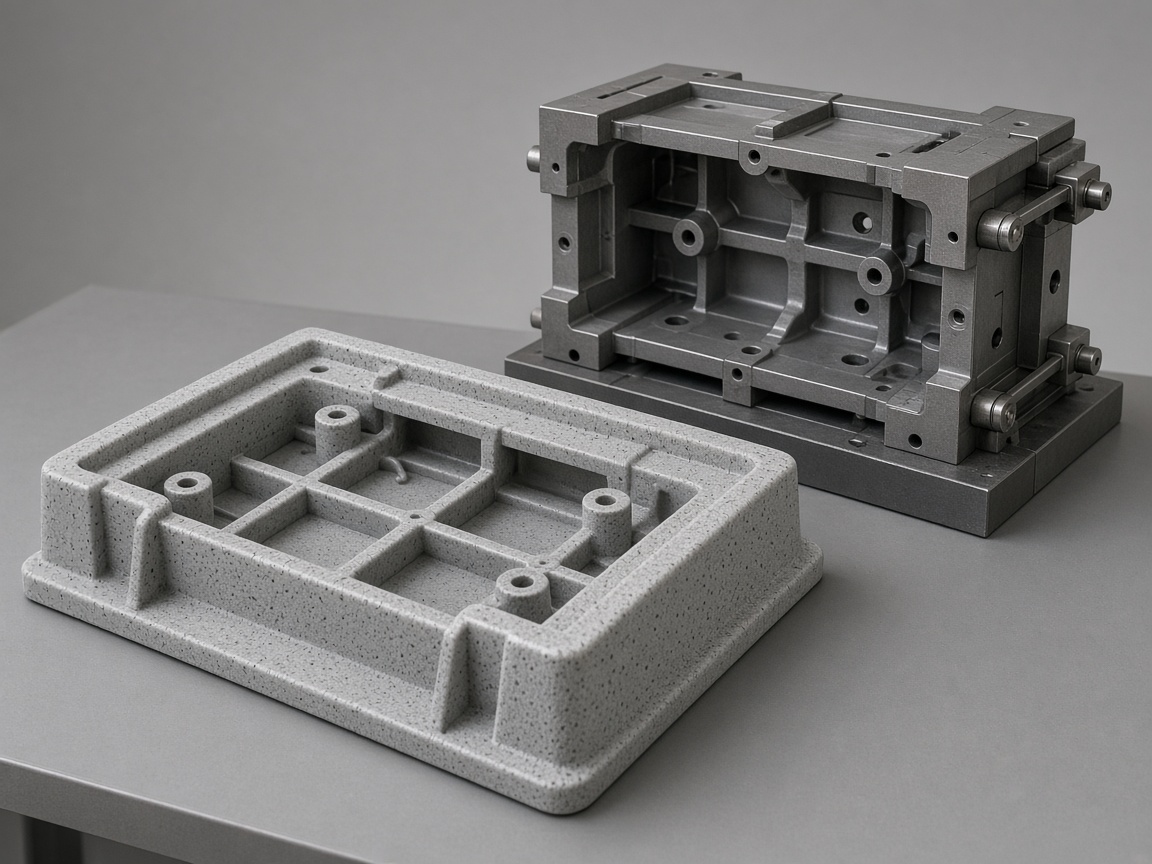
The resin carries a chemical blowing agent, or nitrogen injected into the barrel. While it stays under pressure in the barrel, the gas stays dissolved. Once a short shot enters the cavity and the pressure drops, the gas comes out of solution and expands, pushing the resin out to fill the cavity.
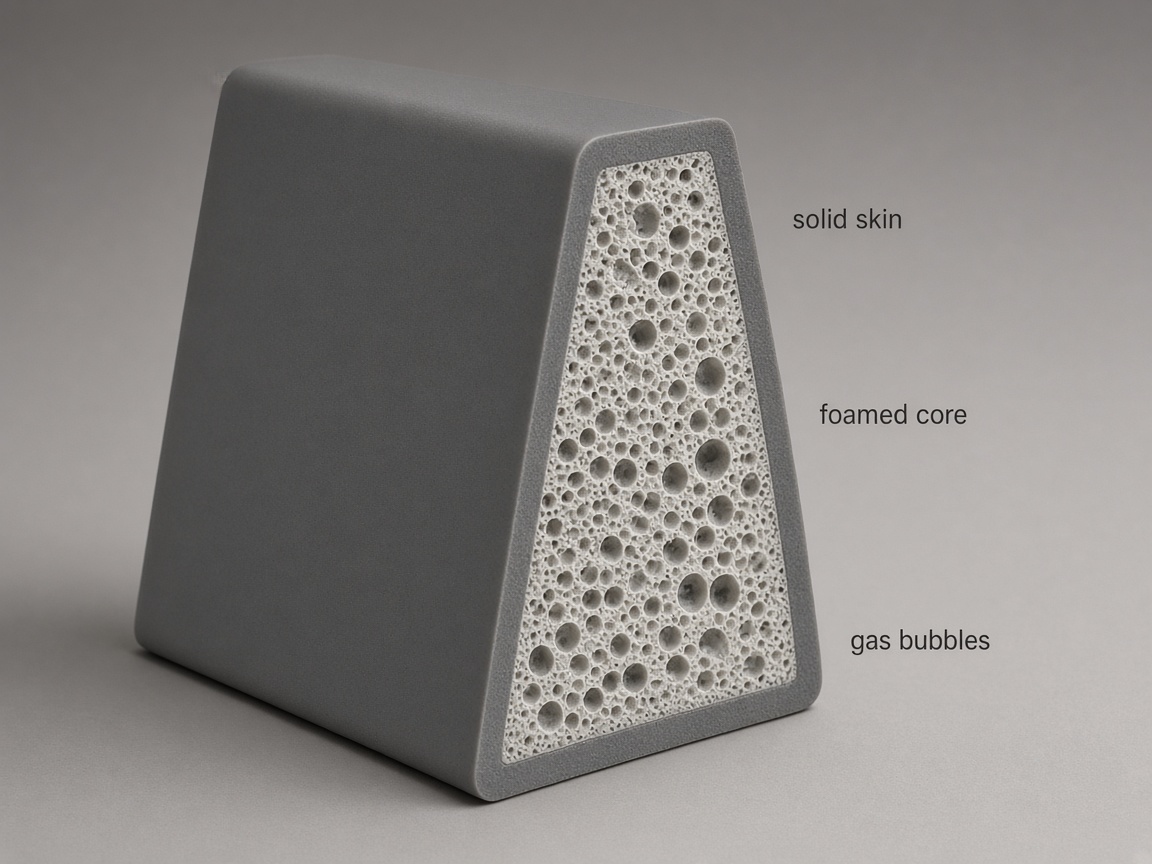
Resin touching the cold steel freezes before the bubbles can grow there, so the part ends up with a solid skin on each face and a foamed core between them. The result is a sandwich that is light and stiff for its thickness.
The foam does the packing, so cavity pressure stays low. That is the whole point commercially. Low pressure means smaller clamps for large parts, and in some cases mold steel or aluminum that could never survive a solid shot of the same size.
Roles
Structural foam is a skin and a coarse core. MuCell is finer cells. Gas assist is one hollow channel.
| Page | Use it for |
|---|---|
| Structural foam (this page) | A large part with a solid skin and a foamed core |
| MuCell | Fine cells through the wall |
| Gas assist | One hollow channel in a thick section |
| Rib design | Stiffness from ribs in a solid molding |
| Painting | Covering the swirl the foam leaves on the skin |
The cut face
Resin against the cold steel freezes into a solid skin. The gas expands in the middle and leaves a foamed core full of bubbles.
Where it shows up
The common thread is size, thickness, and a surface that will be textured, painted, or ignored.
| Part | What foam brings |
|---|---|
| Machine and equipment covers | Large panels that stay flat and stiff without a forest of ribs |
| Pallets and material handling bins | Thick walls that take impact, without the weight of solid resin |
| Kiosk, medical cart, and terminal housings | A few big parts replacing sheet metal, with bosses and mounts molded in |
| Outdoor and agricultural parts | Rugged sections where a paintable textured surface is fine |
The catch
Some of the gas reaches the steel before the skin freezes, and it smears across the face as silver streaks and a dull, swirled pattern.

Alternative
Both get a stiff panel. They get there differently.
Variants
Two related routes get mixed up with classic structural foam.
In core back foaming, the cavity is filled completely at normal pressure, and then part of the mold opens a little so the core of the wall can expand. The skin comes out better and the foam more even, but the tool needs moving steel. It is the second meaning of core back described on the core back page.
Microcellular foaming, sold under names such as MuCell, uses a supercritical gas and much finer cells in thinner walls. The aim there is flatness and dimensional control rather than bulk, and it is covered on its own page.
Keep reading
Other foam and thick part processes, and the finishes that cover swirl.
Microcellular foam in thinner walls.
MuCell foam moldingA hollow channel instead of a foamed core.
Gas assist moldingMoving steel, for a second material or for foam.
Core back moldingGas and moisture marks on the surface.
Silver streaksSizing ribs on the solid wall route.
Rib to wall ratioCovers, housings, and rugged parts.
Industrial and transportationEvery molding process and secondary operation.
All processesFAQ
No. Packaging foam is mostly air. Structural foam has a solid skin and a denser core, and the part is meant to carry load.
Resins that are also molded solid. Polyethylene and polypropylene show up on bins and pallets. PC, PPO, and ABS blends show up on housings. The blowing agent is added at the press.
The wall is thick and the foam slows heat leaving the middle. Open the mold too soon and the hot core keeps growing, so the part bulges after ejection.
Yes. Mounts are one reason these parts replace sheet covers. Thin features fill mostly as solid skin.
Gas assist pushes one hollow channel through a thick section and leaves a solid wall around it. Structural foam fills the part with a foamed core and a solid skin on each face.
MuCell disperses fine cells through the melt. Structural foam is the coarser skin-and-core route used on large, thick parts, and the skin often shows a swirl.
Next step
Upload CAD for DFM review and an instant quote on the injection molded part.