
Zirconia or alumina
- Hardness and wear resistance no plastic comes close to
- Stays stiff and insulating at temperatures that would melt any resin
- Brittle, so drops and point loads need care in the design
Process guide
CIM runs feedstock through molding, debinding, and sintering to hard zirconia or alumina parts. This guide stays at industry-typical ranges and when plastics may be enough.
Same route, less forgiveness
Process knowledge for engineers evaluating CIM. Not a statement of in-house CIM capacity.
Ceramic injection molding shapes a powder part that is then fired into ceramic. Metal injection molding follows the same route with metal powder. PEEK and PEI stay plastic when the part needs toughness. Micro molding is about a shot too small to meter, not about the furnace.
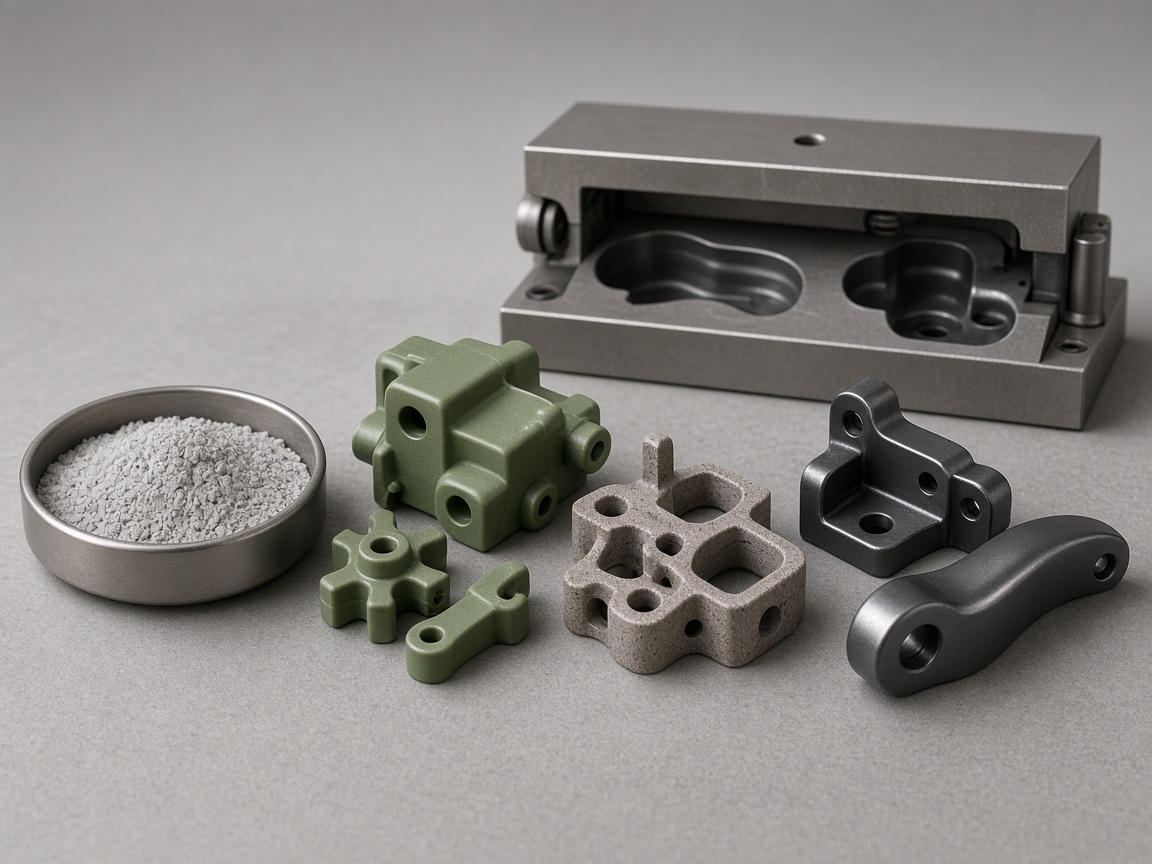
This guide describes ceramic injection molding (CIM) as industry practice. Whether a program belongs on CIM, plastic, or another route is decided in RFQ review.
The stages match MIM: feedstock, a molded green part, binder removal, then sintering to full hardness. A metal part can hide a small void or a weak knit line, because metal yields a little before it breaks. A fired ceramic has no such margin. Whatever went wrong in the mold tends to come out of the furnace as a crack.
So most of the engineering effort on a CIM part goes into the green state. Gate position, fill pattern, and how the part is picked off the core decide the yield long before anyone opens the furnace.
Roles
Ceramic is fired powder. MIM is the metal version. PEEK and PEI stay plastic.
| Page | Use it for |
|---|---|
| Ceramic injection molding (this page) | A molded powder part that is fired hard |
| Metal injection molding | The same route with metal powder |
| PEEK | A tough plastic when ceramic hardness is not required |
| PEI | Heat resistance that stays a thermoplastic |
| Micro molding | A shot too small for a standard screw |
Which powder
Choose ceramic injection molding when the fired part must stay an electrical insulator, or when wear and heat are beyond a metal. Choose metal injection molding when the same powder route should finish as metal. Metal can take a thread or a press fit that ceramic would crack. The press steps match. The powder decides which page you need.
CIM core process
Industry-typical CIM follows the same powder route as MIM. Molds are scaled for large sinter shrink, not for the green part size you measure at the press.
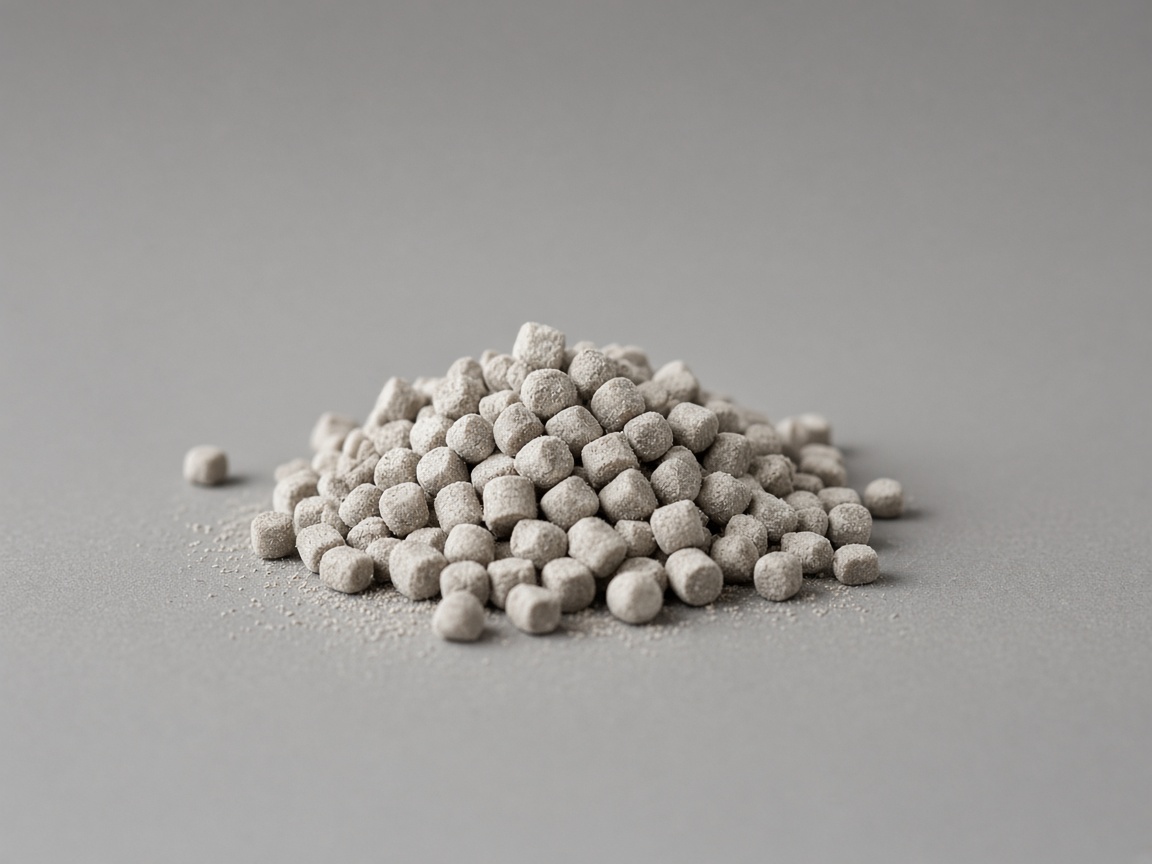
Ceramic powder is mixed with thermoplastic binders into a feedstock that can be injection molded. How much powder the binder can carry depends on the grade.
The feedstock fills a mold like plastic and forms a green part. Knit lines, voids, and gate wash show up here and rarely heal in the furnace.
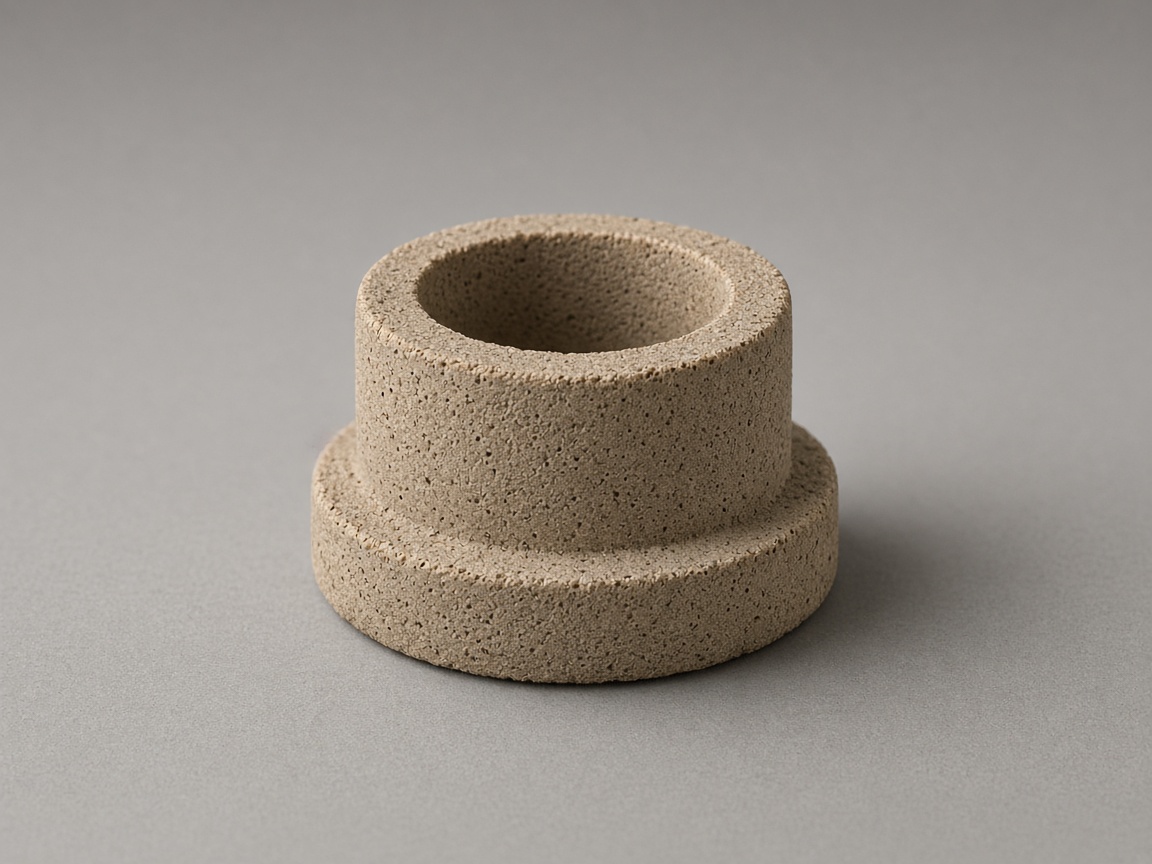
Binders are removed by solvent, thermal, or catalytic debinding routes, often combined. The brown body is porous and fragile before full densification.
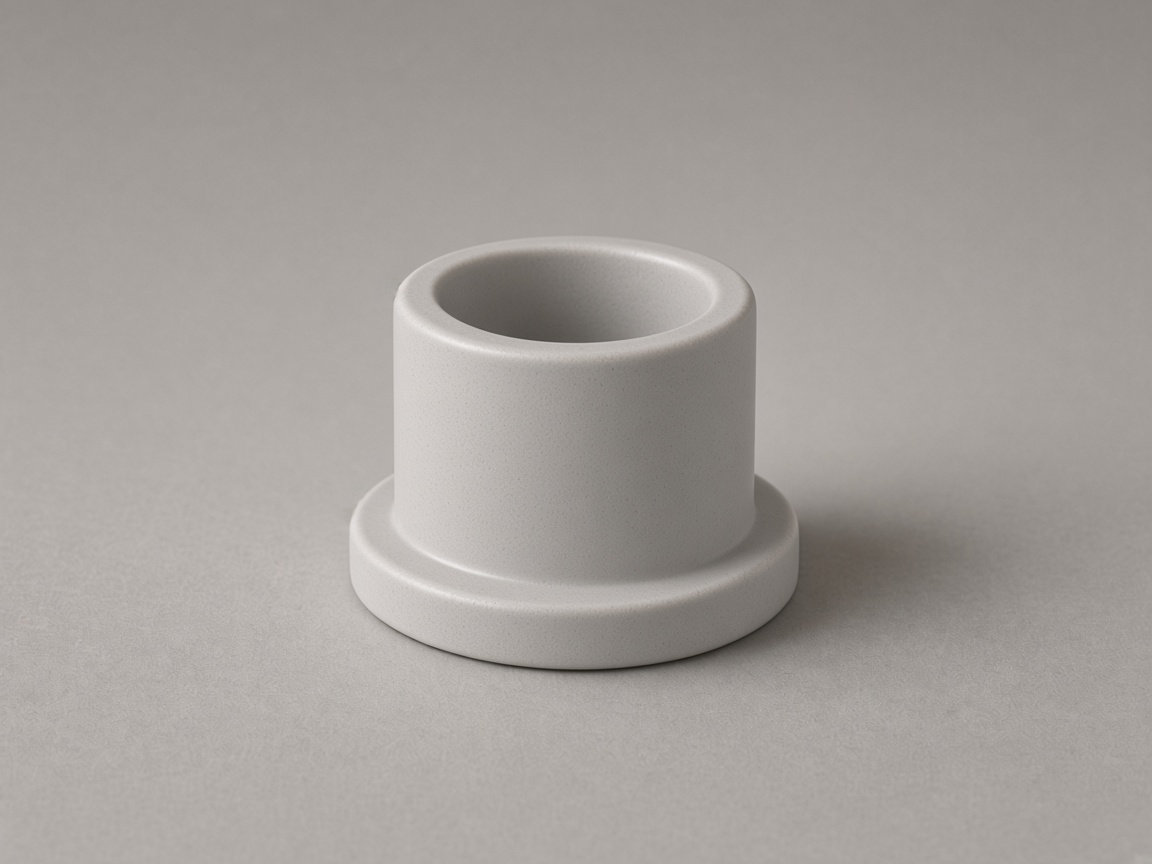
High temperature firing densifies the ceramic and the part changes size. The cavity is scaled for that change. Shrink allowance depends on the feedstock and firing cycle, and it is set during DFM review.
Materials
Zirconia and alumina cover much of the market. Silicon nitride and silicon carbide appear where heat shock and wear dominate. When the job is not at ceramic extremes, PEEK or PEI plastics are often enough.
| Material | Why it is chosen | Typical parts |
|---|---|---|
| Zirconia | Tough for a ceramic, polishes to a high gloss, tooth colored grades | Orthodontic brackets, fiber optic ferrules, watch cases, blades |
| Alumina | Very hard and electrically insulating, the workhorse among technical ceramics | Insulators, thread and wire guides, wear pads, sensor bodies |
| Translucent alumina | Lets light through after careful sintering | Lamp tubes, clear orthodontic brackets |
| Silicon nitride (Si3N4) | High thermal shock resistance and toughness for a ceramic | Turbine components, wear parts in hot or cyclic service |
| Silicon carbide (SiC) | Extreme hardness and wear resistance | Seal faces, slurry components, high-wear inserts |
After molding
The furnace stage turns a molded green part into a dense ceramic.
Debinding routes are usually grouped as solvent, thermal, or catalytic, and many production lines combine steps. The goal is to open porosity and remove binders without cracking the brown body. Ramping too fast or trapping binder in thick sections are common industry failure modes.
Sintering then drives densification with controlled heating rates. The part passes through a porous brown state before it reaches final hardness. That is why green molding quality and uniform section thickness matter as much as kiln profile.
Defects
Each of these can look harmless on a green part.
Knit lines where two flow fronts meet, which fire into weak seams
Voids and sink inside heavy sections, which open up during binder removal
Powder and binder separating near the gate, leaving a zone that shrinks differently
Ejection stress on a fragile green part, leaving microcracks that show only after firing
Uneven sections that trap binder and then crack or bloat in the kiln
Tooling and finishing
Ceramic wears the equipment on the way in and resists every tool on the way out.

Is CIM worth it
Covers searches such as whether ceramic injection molding is worth it. These are routing hints, not hard rules.
A simple disk or block at low volume: machining from ceramic stock or dry pressing is often the simpler route
Large parts where furnace cost and shrink risk dominate: sub-assemblies or machined blanks may beat CIM tooling
Heat, wear, or insulation needs that PEEK, PEI, or other high-performance plastics already meet: plastic injection is usually lower total cost
Impact or drop loads that need toughness more than absolute hardness: engineering plastics or metal MIM may fit better than a brittle ceramic
Alternative
Ceramic is chosen for hardness and heat. When the job is really insulation or light wear, PEEK or PEI is often enough.
FAQ
The route matches: feedstock, a green part, binder removal, then sintering. The powder is ceramic, the fired part is brittle, and a molding flaw is more likely to leave the furnace as a crack.
Firing changes the size of the part. Features that must hold a tight fit are ground or lapped afterward. Shrink allowance depends on the feedstock and firing cycle, and it is set during DFM review.
Small detailed parts that need hardness or heat resistance, such as ferrules, insulators, watch parts, and wear pieces in pumps and valves.
When the part needs toughness and a normal molding cycle. PEEK and PEI cover many of those jobs. Ceramic is the route when hardness, wear, or heat is beyond those plastics.
It is removed before firing, often in more than one step. The sequence depends on the binder and the section. Name both on the RFQ.
No. Firing changes size, and the mold is scaled for that change. The figure belongs to the feedstock and is confirmed in DFM.
Keep reading
The metal version of the process and the plastics that take on ceramic jobs.
The shared powder and sintering route.
Metal injection moldingHeat, wear, and chemical resistance in a plastic.
PEEKStiffer and harder wearing than plain PEEK.
Carbon fiber PEEKInsulating and flame resistant.
PEI (Ultem)Choosing between the two.
PEEK vs UltemEvery molding process and secondary operation.
All processesPlastic DFM habits that still help you compare CIM versus molded resin.
Injection molding DFMGeneral CAD upload and quoting entry for plastic programs.
Instant quote platformPEEK, PEI, and other grades when ceramic is more than you need.
Materials libraryNext step
Upload CAD for DFM review and an instant quote on the injection molded part.