
Overmolded TPE seal
- No loose seal to misplace in assembly
- Seal and soft grip made in the same step
- The resin pair must bond, and changes need tool work
Molded part guide: wearable enclosures
Fitness bands, clip-on trackers, smart rings, and body-worn sensors live against skin all day. Their shells are thin to keep weight and size down, they have to keep out sweat and rain, and they meet sunscreen, lotion, and cleaners that most enclosures never see. Those chemicals are what usually break them.
Worn all day
Fitness bands, clip-on trackers, smart rings, body sensors, and hearing device shells.
A wearable shell is small and thin, and it carries a battery, a board, sensors, and often a charging contact. Thin walls in a small part fill quickly and freeze quickly, so the flow path from the gate to the far end is checked early. A gate on a hidden face or under a strap keeps its vestige off the surface people look at and touch.
Sealing is usually done in one of three ways. A soft TPE layer overmolded onto the rigid shell seals the seam and adds grip at the same time. A separate gasket is compressed between halves by screws or snaps. Or the halves are closed permanently by ultrasonic welding or adhesive. Charging contacts that pass through the shell are insert molded so plastic seals around each pin.
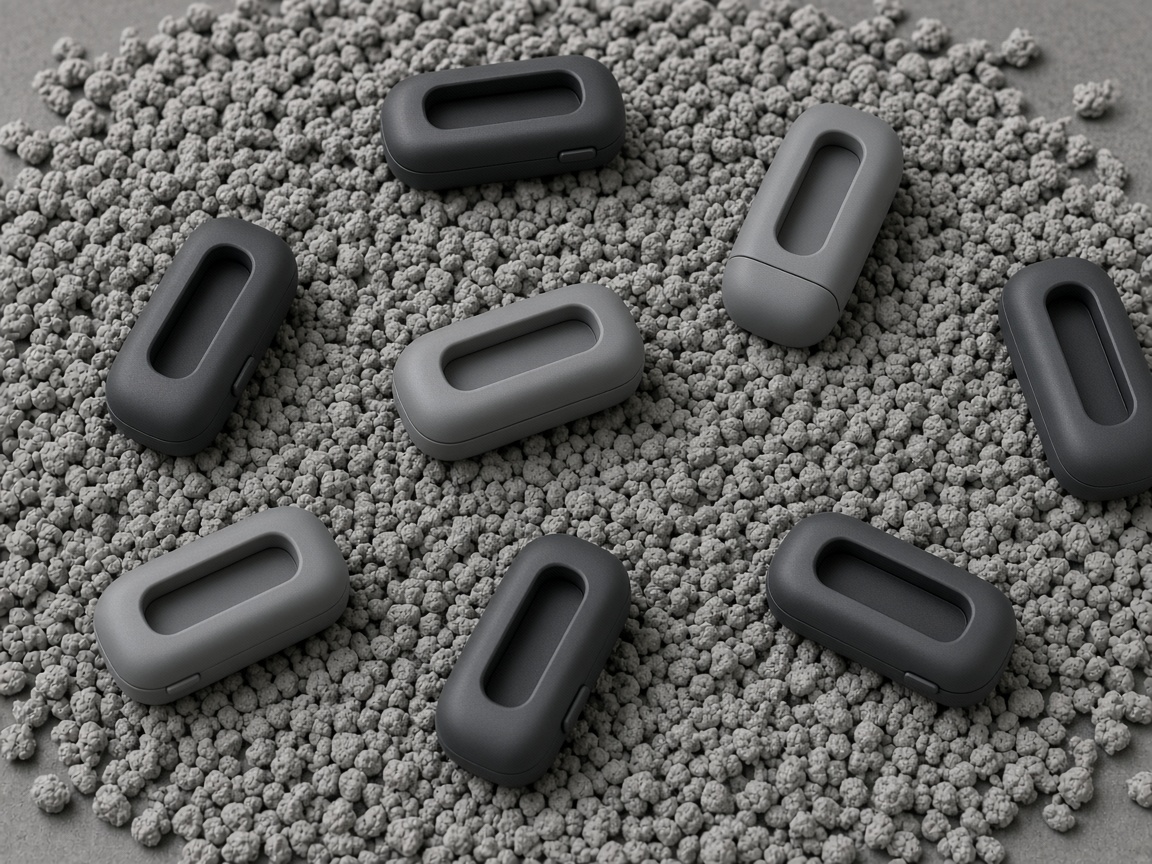
The failure that surprises teams is cracking in the field. Sunscreen, hand lotion, insect repellent, and some cleaners contain oils and solvents that attack stressed polycarbonate and similar resins. A shell that is fine in the chemical alone, and fine under load alone, cracks when both are present. The cracks start where stress is locked in: press fits, snaps, and screw points.
Two things reduce the risk. Molding with less locked-in stress, through gate placement, even walls, and tool temperature. And choosing a resin grade with better chemical resistance for the surfaces that touch skin. Soaking stressed parts in the real lotions the product will meet is the practical way to check a design before tooling is final.
Features
Each feature trades size against sealing and strength.
| Feature | Purpose | Design note |
|---|---|---|
| Thin rigid shell | Holds electronics at low weight | Flow path checked early, gate hidden |
| TPE overmold | Seal and soft grip | Resin pair chosen to bond, with mechanical locks |
| Molded-in contacts | Sealed charging pins | Insert molded so plastic flows around each pin |
| Closed seam | Keeps sweat out | Ultrasonic weld, adhesive, or gasket |
| Strap attachment | Carries pulling loads | Metal pin or solid section, not a thin snap |
Service tiers
Part focus: Sweat and lotion on stressed PC, TPE seal beads. Upload CAD with critical fits and environment in notes when not modeled.
| Tier | Environment | What matters most | Typical molded route | Quote path |
|---|---|---|---|---|
| 1 Thin shell | Battery, board, and sensors | The flow can freeze before the far end | Gate on a hidden face | Upload CAD; note the span |
| 2 TPE seal | Closes the seam and adds grip | The pair has to bond | Overmold, plus a hole or an undercut | Instant quote; name both resins |
| 3 Gasket | Compressed between the halves | Needs screws or snaps to hold the load | Gasket named on the drawing | Upload CAD |
| 4 Contacts | Charging pins through the shell | Sweat must not get in around them | Insert molded so plastic flows around each pin | Instant quote; note the pins |
| 5 Skin chemicals | Sunscreen, lotion, repellent, cleaners | Cracks where stress is locked in | Name the chemicals with the resin | Instant quote; name the lotions |
Materials
One primary family per line item. Put commercial grade, fillers, and environment filters in comments.
| Family | Typical use on this part type | Notes for instant quote |
|---|---|---|
| PC | Rigid shells that meet lotion and sunscreen | Field PC; name the lotions |
| TPE | Overmolded seal and grip | Field TPE; name the resin it bonds to |
Chemical attack
Many resins survive a lotion alone or a load alone, but crack with both.
Sealing
Both seal well. They differ in assembly and in flexibility later.
Avoid these
Two choices that crack a shell against the skin, or peel the seal.
A press fit, a snap, or a screw on a face that touches skin, without naming the lotion. Sunscreen, lotion, and insect repellent attack stressed polycarbonate there. Name those chemicals, and keep the stressed fits off the skin face.
A TPE overmold with nowhere to lock. If the resin pair does not bond, the seal peels. Give the TPE a hole or an undercut to flow through.
Drawing
How and where it is worn drives most choices.
Enclosure CAD with seal and seam details
Chemicals the device will meet, such as lotions, sunscreen, and cleaners
Charging or sensor contacts through the shell
Colors, textures, and soft grip areas
Strap attachment and its loads
Expected annual volume
Keep reading
Other worn devices, soft resins, and ways to close a seam.
Crystal seats, case backs, and lugs.
Watch casesSmall shells with acoustic ports.
Earbud housingsBoards, shielding, and heat.
Electronic enclosuresThe usual soft overmold resin.
TPEChoosing the soft layer.
TPU vs TPESealing contacts into the shell.
Insert moldingClosing the seam for good.
Ultrasonic welding vs adhesiveHow we support consumer programs.
Consumer productsEvery part-type guide, grouped by family.
Molded parts libraryCases, bands, and cradles together.
WearablesFAQ
Most likely chemical attack on a stressed area. Lotions and sunscreen find the press fits and snaps where stress is locked in. Lower molded-in stress and a more resistant grade usually solve it. Moving press fits and snaps away from surfaces that touch skin also lowers the risk.
Not if the resin pair is chosen to bond and the design adds mechanical locks, such as holes or undercuts the TPE flows through. The rigid shell is often molded first and then placed in a second tool, where the TPE is shot over it.
Yes. Insert molding places the contacts in the tool so plastic flows around each pin and seals it as it cools. The contact tips are then finished flush with the shell surface so they wipe clean.
It depends on the flow length from the gate and the resin. We check the fill early and suggest gate positions and local thickening where the shell must stay thin. Short flow paths, more than one gate on longer shells, and generous radii at corners all help thin walls fill.
The vestige shows on a surface people look at and touch. Put the gate on a hidden face, or under the strap.
When the shell does not have to open. Ultrasonic welding or adhesive closes it for good. A gasket is for a seam that screws or snaps shut.
Next step
Upload the enclosure and tell us what it will be exposed to. DFM feedback covers fill, sealing method, contact inserts, and stress at snaps.