
High polish in the mold
- Every part comes out glossy with no extra step
- The polish is made once, in the steel
- Cannot fix gate marks, trimmed edges, or faces changed after molding
Process guide
A clear part can come out of the mold with a hazy edge, a gate mark, or a trimmed face that is no longer glossy. Vapor polishing melts a thin skin of the surface just long enough for it to level out and clear up.
How it works
The surface is not ground or buffed. It is briefly dissolved and allowed to flow.
Vapor polishing uses solvent vapor to level a thin skin after molding. High gloss polish is what the mold can do instead. Annealing is the stress relief step people pair with vapor. Lenses and light pipes are the clear parts that ask for it.
A heated solvent, often a chlorinated or specialty polishing solvent, is turned to vapor and directed at the part with a nozzle or in a closed chamber. The vapor condenses on the cooler plastic and dissolves the outermost layer. Surface tension pulls that thin liquid layer flat, fine scratches and tool marks fill in, and the solvent evaporates to leave a glossy surface.
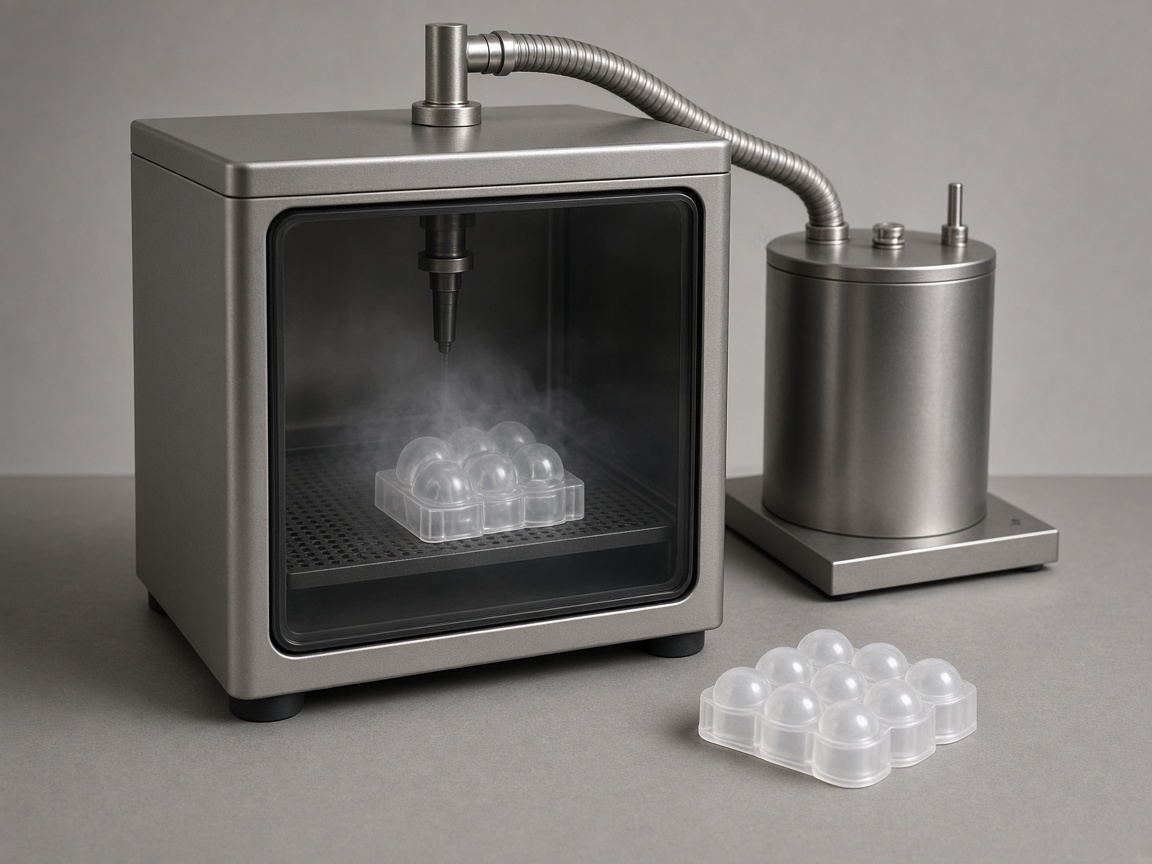
It works on amorphous resins that the solvent can dissolve, such as polycarbonate, acrylic, polysulfone, and PEI, the same group that solvent bonds well. It is fast and reaches edges, holes, and inside corners where a buffing wheel cannot go.
Roles
Vapor polishing treats the part. High gloss polish is in the steel. Annealing is the heat step that may come with it.
| Page | Use it for |
|---|---|
| Vapor polishing (this page) | Solvent vapor on the molded part |
| High gloss polish | Gloss cut into the mold |
| Annealing | Stress relief before or after a solvent step |
| Lenses | A clear part that may need the surface |
| Light pipes | Another clear optical part |
Where to polish
On molded parts, the mold is usually the first answer. Vapor polishing covers what the mold cannot reach.
Uses
It is most common on low volume clear parts and on machined clear stock, and less so on molded parts.
| Situation | Why vapor polish |
|---|---|
| Light pipes and lenses with a trimmed gate | Clears the gate area so it does not scatter light |
| Clear medical and lab parts | Lets operators see fluid clearly through edges and internal channels |
| Display and demonstration parts | Glass like faces on low volume clear parts where the mold was not fully polished |
| Clear parts from machined stock | Removes tool marks that would otherwise need hand polishing |
The risk
The same solvent that smooths the surface will attack stressed plastic, and the damage can take hours or days to appear.

Keep reading
Polishing in the steel, clear resins, and the parts that need clear faces.
Getting gloss from the mold steel.
High gloss polishThe two main clear resins compared.
Polycarbonate vs acrylicClear optics and what spoils them.
LensesCarrying light from a board to the surface.
Light pipesThe same chemistry used to join parts.
Solvent bondingClear, tough, and heat resistant.
Polysulfone (PSU)Every molding process and secondary operation.
All processesFAQ
Only if the cloudiness is on the surface, such as fine scratches or a matte finish. Haze inside the part, from moisture, degraded resin, or crystallinity, stays.
Very slightly. A thin skin flows, and sharp edges and fine texture soften. Critical sealing faces and snap features are usually masked or left unpolished.
Not with the usual solvents. They resist them, which is one reason those resins are chosen for chemical service. Flame polishing is sometimes used instead on low volume parts.
It is used on them, but residual solvent has to be controlled and verified for the application. That is a validation question for each device, not a general yes.
Mold polish is in the steel and repeats on every shot. Vapor polishing treats the part after it is molded. Start with high gloss polish when the mold can hold the surface.
Clear lenses and light pipes. Name the resin on the RFQ. The solvent process is set per resin before polishing.
Next step
Upload CAD for DFM review and an instant quote on the injection molded part.