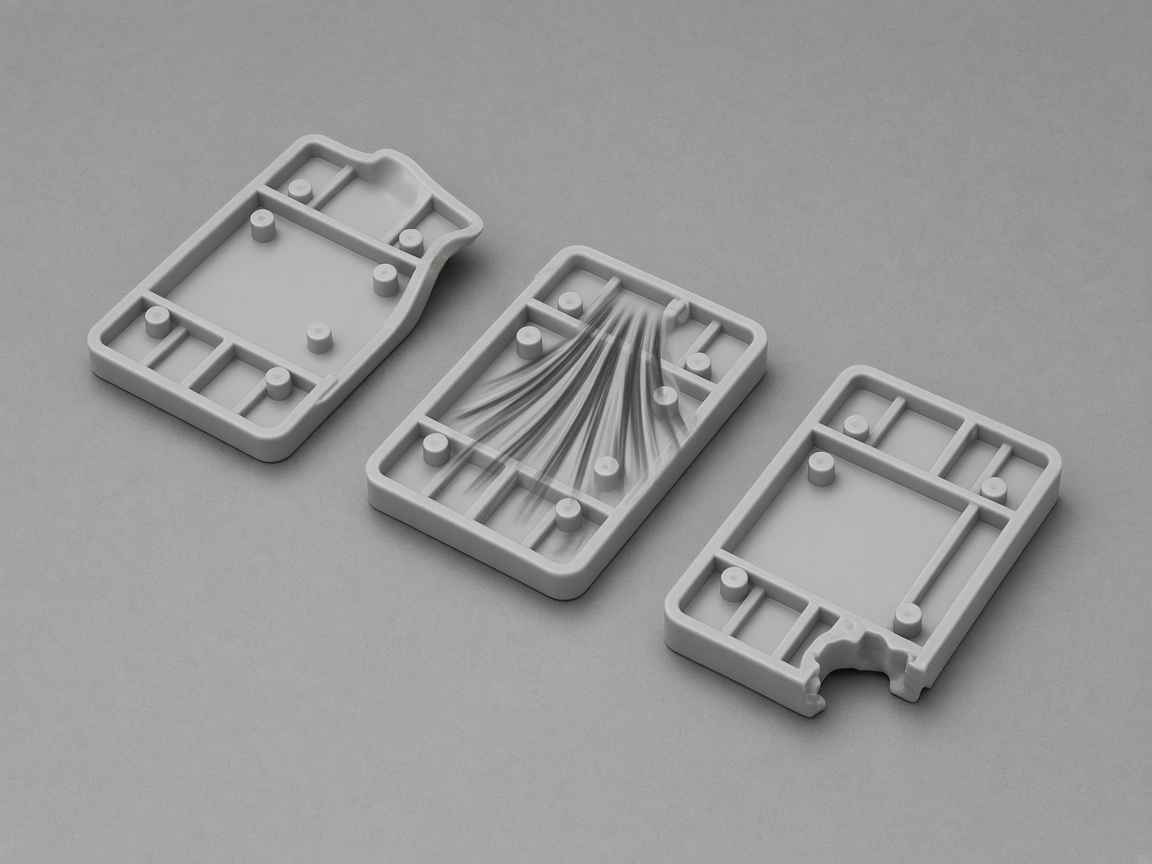
| Melt or mold temperature too low for the resin window | Wavy bands that worsen away from the gate; dull surface with stiff flow | Raise melt and mold heat within supplier limits; confirm barrel profile matches the approved setup sheet |
| Fill too slow so the skin freezes before the cavity is uniformly wetted | Ripple or ring patterns along flow; semi-solid layers pushed by later melt | Increase injection speed during fill in controlled stages; avoid a single slow first stage on long flow paths |
| Abrupt wall thickness changes or sharp corners in the cavity | Lines that track thin-to-thick transitions; hesitation marks near ribs or bosses | Smooth transitions in CAD; add radii on cores; use fill simulation to preview hesitation before tooling changes |
| Undersized gate or runner restricting flow | High shear near the gate plus downstream waves; pressure spikes on the machine log | Enlarge gate or runner in the next tool revision; balance restriction with jetting risk at the gate |
| Moisture or inconsistent melt density in hygroscopic resins | Flow lines plus splay or silver streaks; defect worsens after material lot change | Verify drying time and temperature; stabilize back pressure for homogeneous melt before chasing mold polish |
| Poor venting or trapped air disturbing the flow front | Waves at end of fill; burn or blush adjacent to flow tracks | Clean and deepen vents at last-to-fill regions; confirm parting line alignment before texture or polish work |