
What the floor team often tries first
- Lowering barrel temps everywhere while vents remain plugged or shallow.
Defect troubleshooting
Burn marks are charred or brown patches, often at last-to-fill areas or vents, caused by compressed air or material overheating.
Defect troubleshooting
Burn marks look like brown, black, or degraded patches on the part or at the vent land. They often appear at the last place the cavity fills, near vent pins, or in trapped air pockets around deep ribs.
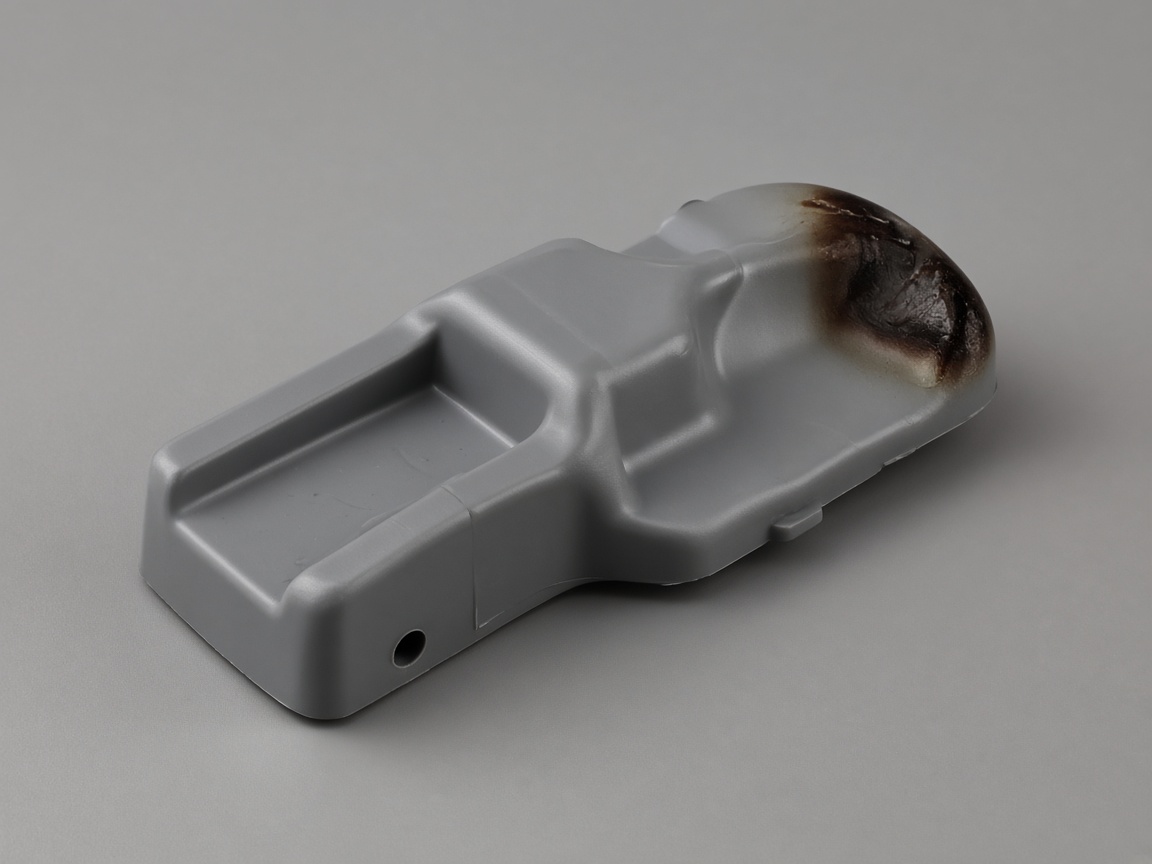
The usual mechanism is diesel effect: air or volatiles compress and heat until the material degrades at the surface. Less often, excessive shear in a thin channel overheats a narrow melt ribbon.
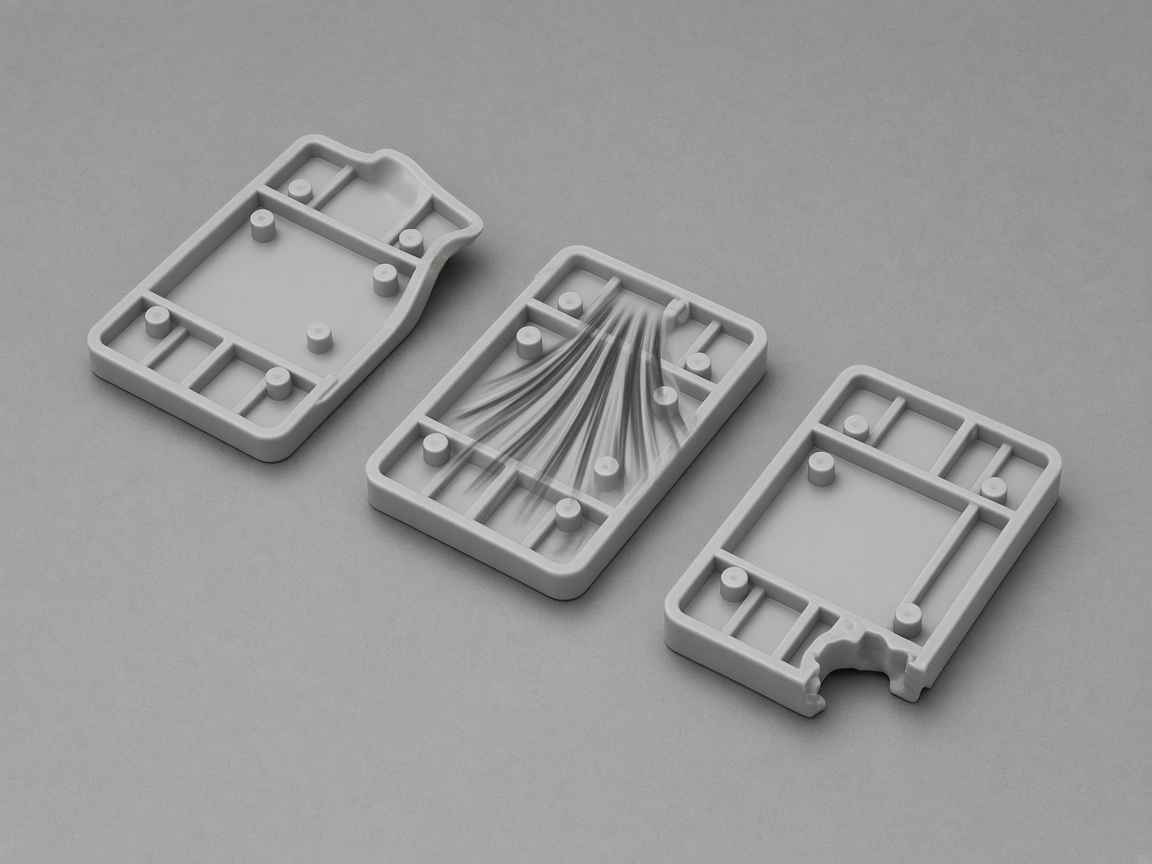
Start with venting and fill rate at the burn location, not with arbitrary temperature cuts alone. Document vent depth, cleanliness, and whether burns move when fill speed changes.
| Signal on the part | Common process lever | Tooling / DFM lever |
|---|---|---|
| Dark spot at vent or parting line | Clean vents; increase vent depth or count | Vent placement in DFM at last fill |
| Burn inside rib or boss | Slow fill locally; improve vent path from rib | Rib thickness ratio; avoid blind traps |
| Burn after material change | Verify dry time and melt temperature window | Gate size vs shear for new resin |
Mark whether burn is vent-adjacent or mid-wall in thin sections.
Inspect vent lands, obstructions, and blow-back from prior runs.
Adjust first-stage speed to see if burn tracks air trap timing.
Confirm drying and melt stability for the lot in use.
Use this order before opening steel or rewriting fill profiles without data.
Vent pins extracted and cleaned on the affected cavity.
Parting line alignment and clamp tonnage verified.
No blocked vent channels in last-to-fill pocket.
Photos logged for quality and steel review if needed.
Ribs, bosses, and deep pockets need vent paths planned before CNC starts. Instant quote intake includes DFM feedback on risky geometry.

Browse related defect guides and prevention checklists.
Learn moreWhere melt fronts meet and how to reduce cosmetic risk.
Learn moreGate aim and early-fill velocity issues near the gate.
Learn moreIncomplete fill and venting checks before blaming the mold.
Learn moreIndirectly if vents are poor, but burns are primarily an air-trap and shear story. Fix vent path first.
Cosmetic burns may be reworked per spec; structural degradation requires root-cause closure.
Ready to quote
Upload CAD for DFM review focused on venting and last-to-fill regions before build.